With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider of industrial material handling solutions, specializes in advanced pneumatic conveying systems designed for the efficient transport of rare earth materials. This article explores the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in modern industrial applications.
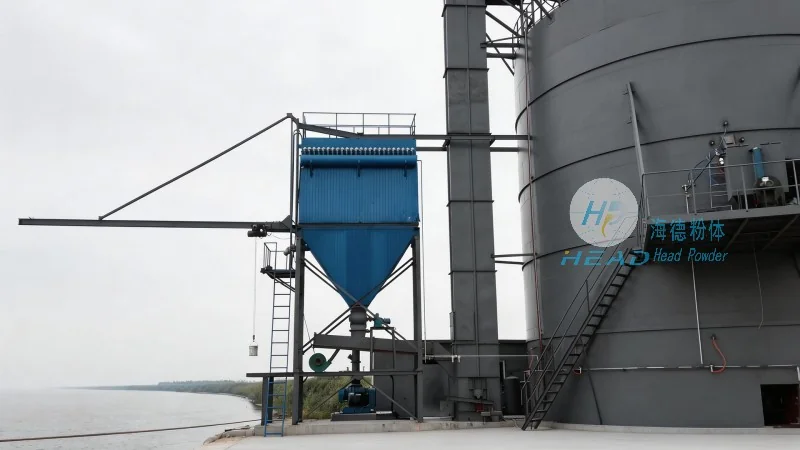
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has established itself as a trusted name in the field of material handling technology. The company’s expertise lies in developing and manufacturing high-performance pneumatic conveying equipment tailored for the unique demands of rare earth processing industries. These systems are engineered to ensure reliable, low-maintenance operation while maximizing productivity and safety in handling these critical materials.
The fundamental principle of pneumatic conveying involves the use of air or gas to transport bulk materials through a pipeline system. In the case of rare earth materials, which often require precise control and minimal contamination, HeadPowder’s systems utilize a combination of positive and negative pressure methods. Positive pressure systems push material through the pipeline using a blower or compressor, while negative pressure systems draw material into the system using a vacuum pump. This dual approach allows for flexible operation and adaptability to different material properties and process requirements.
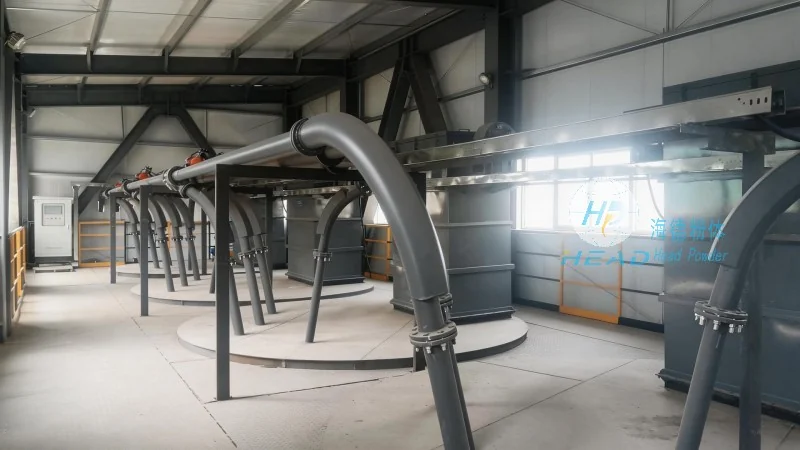
One of the most significant advantages of rare earth pneumatic conveying systems is their ability to operate in diverse industrial environments. The systems are designed to handle materials with varying particle sizes, densities, and flow characteristics, making them suitable for both short-distance and long-distance transport. In industrial settings, these systems are commonly used in rare earth ore processing plants, where they facilitate the movement of raw materials from storage silos to processing units, and in manufacturing facilities where finished products are transferred to packaging or storage areas.
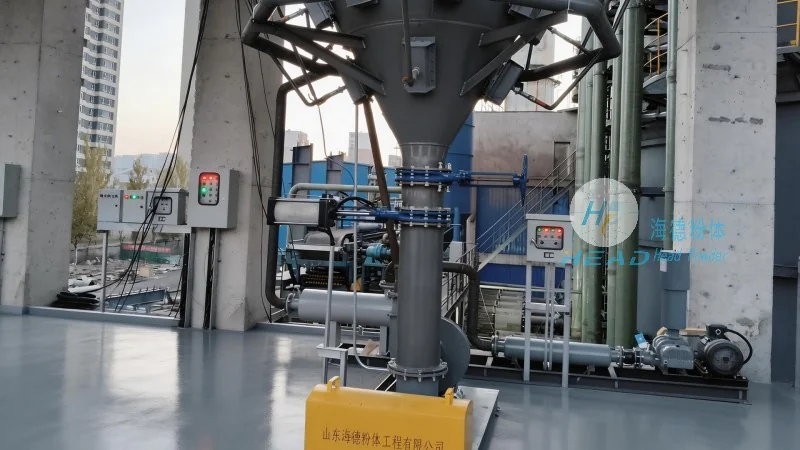
Another critical characteristic is the system’s ability to maintain material integrity and prevent contamination. Rare earth materials are often sensitive to moisture, dust, and other environmental factors, and HeadPowder’s equipment incorporates features such as sealed pipelines, air filtration systems, and material drying units to ensure that the conveyed material remains in optimal condition. This is particularly important in applications where the purity of the rare earth material directly impacts the quality of the final product.
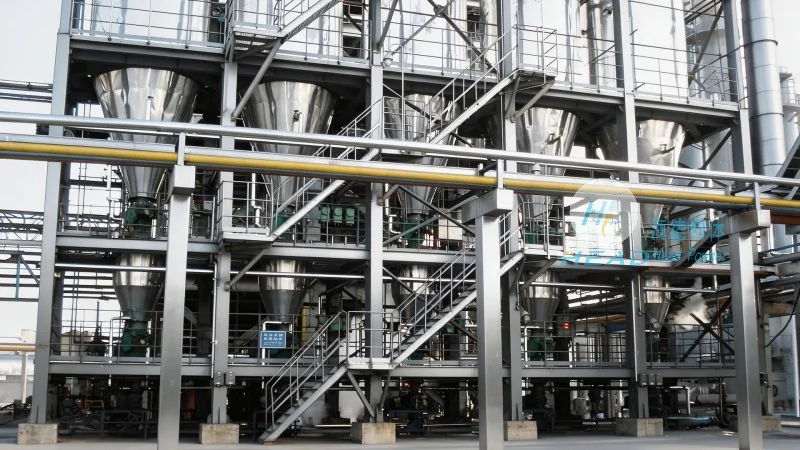
HeadPowder’s rare earth pneumatic conveying systems are engineered for high operational efficiency and ease of maintenance. The use of robust materials, such as stainless steel and corrosion-resistant alloys, ensures durability even in harsh industrial environments. Additionally, the systems are equipped with advanced monitoring and control technologies that allow for real-time tracking of material flow, pressure, and temperature. This enables operators to quickly identify and resolve any issues, minimizing downtime and maximizing productivity.
HeadPowder Engineering Co., Ltd. continues to innovate in the development of rare earth pneumatic conveying systems, providing industries with reliable and efficient solutions for material handling. By understanding the core principles and working scene characteristics of these systems, businesses can make informed decisions to enhance their operational performance and ensure the safe and effective transport of rare earth materials. With a strong presence in Shandong, China, HeadPowder remains committed to delivering high-quality equipment that meets the evolving needs of the rare earth processing sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top