

Working Principle and Features of a Calcium Carbonate Material Pneumatic Conveying System
For industrial applications involving the handling of calcium carbonate powders, efficient and reliable material transport is crucial. The pneumatic conveying system designed by Shandong HeadPowder Engineering Co., Ltd. (a company known as HeadPowder) offers a robust solution that addresses the unique challenges associated with calcium carbonate material handling. This article explores the working principle and key features of this specialized equipment, providing insights into its functionality and benefits for various industrial processes.
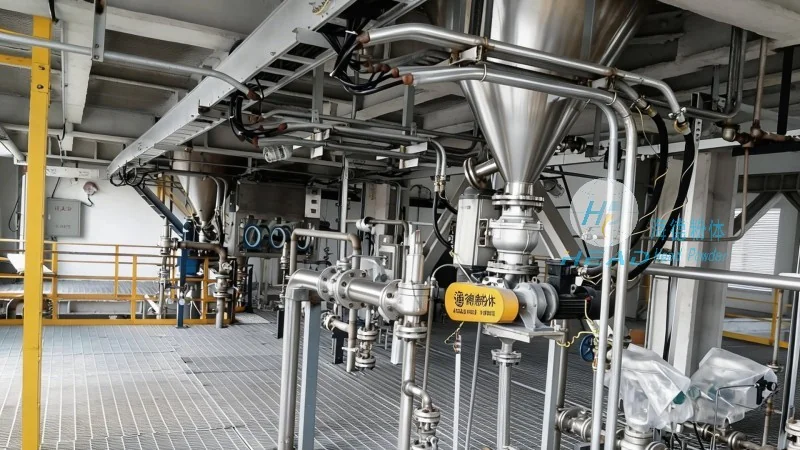
Working Principle of the Calcium Carbonate Pneumatic Conveyor
The calcium carbonate pneumatic conveying system operates on the principle of using compressed air to transport bulk materials through a pipeline network. The process begins with the material being fed into a hopper or feeder, where it is then drawn into the conveying line by the action of the air flow. As the air moves through the pipeline, it creates a low-pressure zone that pulls the calcium carbonate particles along with it, ensuring a consistent and controlled flow. The system typically includes components such as a blower, a filter, and a discharge valve, all working in tandem to maintain optimal pressure and prevent material degradation. The air velocity is carefully controlled to ensure that the calcium carbonate particles are conveyed without causing excessive wear on the system components or clogging the pipeline. This method of pneumatic transport is particularly effective for calcium carbonate, as it minimizes the risk of dust generation and provides a clean, efficient means of moving the material from the source to the destination.
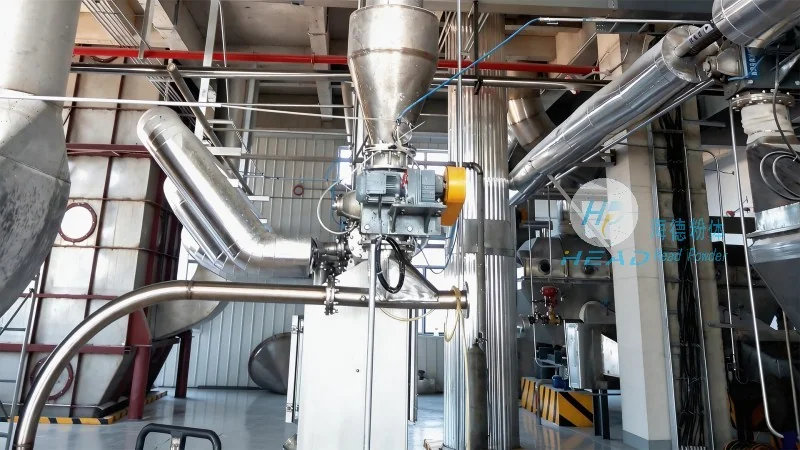
Key Features of the Calcium Carbonate Pneumatic Conveyor
The pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. is engineered with several key features that enhance its performance and reliability. One of the primary advantages is its ability to handle calcium carbonate in a dust-free environment, which is essential for maintaining product quality and ensuring workplace safety. The system is designed with corrosion-resistant materials to withstand the chemical properties of calcium carbonate, extending its operational lifespan. Additionally, the conveyor features adjustable air pressure and flow rates, allowing for customization to meet the specific requirements of different industrial applications. The compact design of the system makes it suitable for installation in limited spaces, while the modular construction facilitates easy maintenance and component replacement. Another notable feature is the integration of a filtration system that captures any fine particles, preventing them from escaping into the environment and ensuring compliance with environmental regulations. The system also includes safety features such as pressure relief valves and overload protection, providing peace of mind for operators and ensuring continuous operation without interruptions.
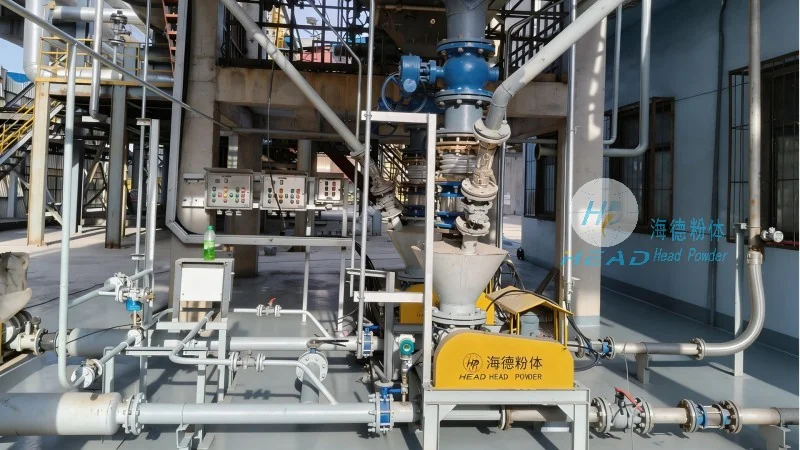
Benefits and Applications
The calcium carbonate pneumatic conveying system offers numerous benefits for industries that rely on calcium carbonate as a raw material. By eliminating the need for traditional bulk handling methods, such as bucket elevators or belt conveyors, the system reduces labor costs and operational downtime. The dust-free operation minimizes product contamination and improves overall process efficiency. The system is particularly well-suited for applications in the chemical, pharmaceutical, and food industries, where product purity and safety are paramount. Additionally, the ability to transport calcium carbonate over long distances without the need for intermediate storage or transfer points streamlines production processes and enhances overall productivity. The system's adaptability to various particle sizes and flow rates makes it a versatile solution for a wide range of industrial needs, from small-scale laboratory operations to large-scale manufacturing facilities.
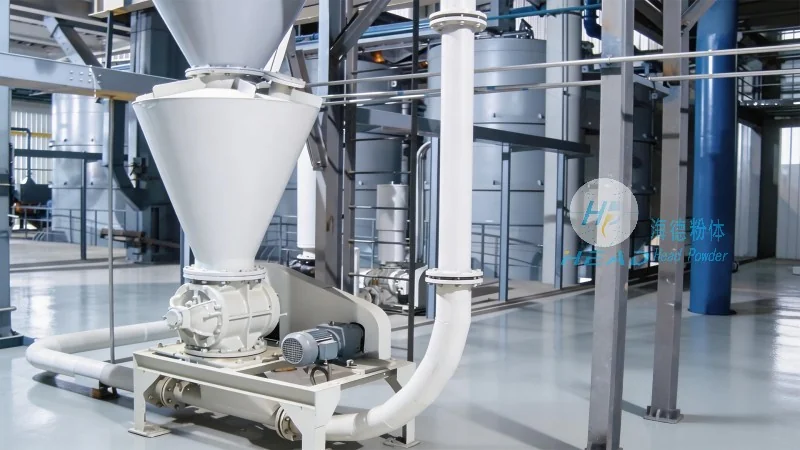
Conclusion
In conclusion, the calcium carbonate pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated and efficient solution for the transportation of calcium carbonate materials. Its working principle, based on pneumatic transport, ensures reliable and controlled movement of the material, while its key features, including dust-free operation, corrosion resistance, and adjustable parameters, enhance its performance and adaptability. The system's benefits, such as reduced labor costs, improved product quality, and streamlined processes, make it an attractive option for industries seeking to optimize their material handling operations. As a leader in engineering solutions for bulk material transport, Shandong HeadPowder Engineering Co., Ltd. continues to provide innovative and reliable equipment that meets the evolving needs of industrial applications.