With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Sugar, particularly granulated or powdered sugar, presents unique challenges in industrial handling. It is a highly friable material that tends to generate fines and dust during movement. Furthermore, sugar is hygroscopic, meaning it absorbs moisture from the air, which can lead to clogging in mechanical systems or clumping in storage. Traditional methods of material handling often struggle with these specific properties. Consequently, selecting a robust and precise sugar conveying system is critical for maintaining product integrity and ensuring operational efficiency in food processing plants.
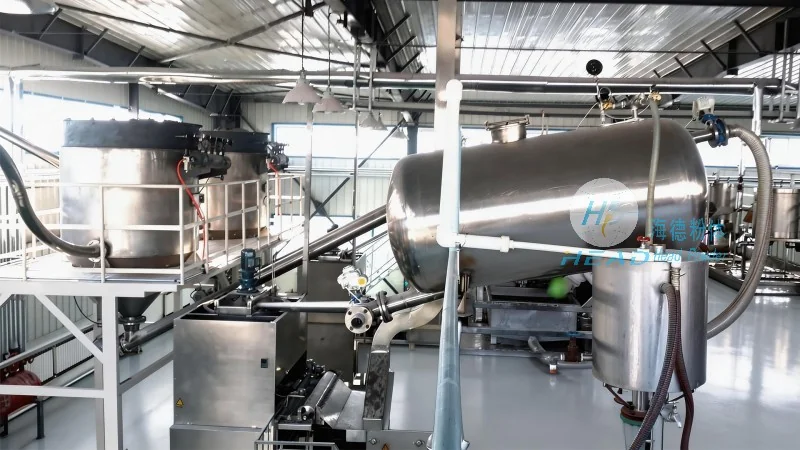
To address these challenges, sugar pneumatic conveying has emerged as the preferred solution in modern industrial settings. This technology utilizes air pressure or vacuum to move the sugar through a closed pipeline system. Unlike mechanical conveyors that rely on physical contact with belts or screws, pneumatic conveying gently suspends the sugar particles in the air stream. This method allows for the precise and continuous transfer of bulk sugar from storage silos to processing equipment or packaging lines. The system is designed to handle various flow rates and distances, making it versatile for different facility layouts.
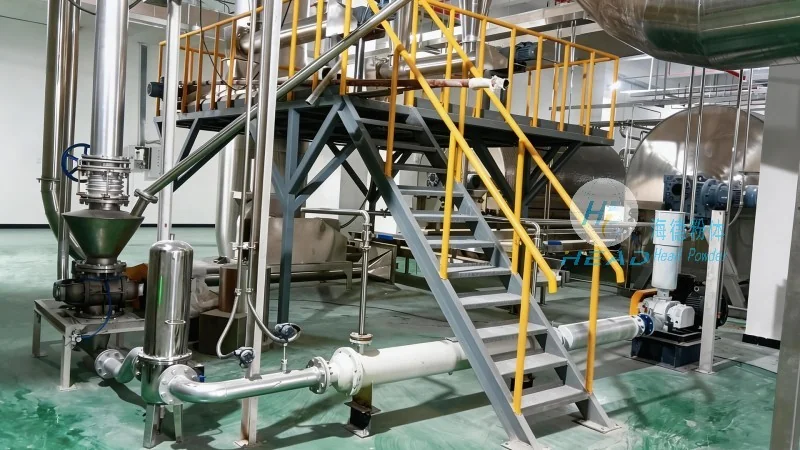
The adoption of pneumatic conveying technology offers significant advantages over traditional mechanical methods. First and foremost is the issue of hygiene and contamination. Because the entire transfer process takes place within a sealed pipeline, there is zero risk of external contamination. This is paramount in the food industry, where strict hygiene standards must be maintained. Additionally, pneumatic conveying eliminates the physical abrasion that occurs when sugar rubs against conveyor belts or screws, thereby preserving the quality of the sugar and reducing maintenance costs. The system is also highly flexible; pipes can be installed in tight spaces or around existing machinery without significant disruption.
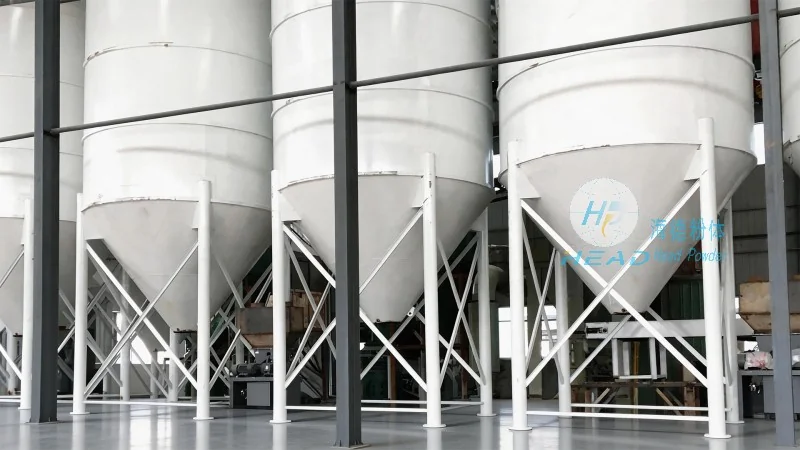
For businesses seeking reliable and efficient material conveying solutions, Shandong Headpowder Engineering Co., Ltd. stands out as a dedicated expert in the field. Located in Shandong, China, the company specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for the food and chemical industries. Headpowder focuses on understanding the specific rheological properties of different powders, including the delicate nature of sugar. Their engineering team works closely with clients to develop customized systems that optimize energy consumption while maximizing throughput.
Headpowder distinguishes itself through a commitment to quality and technical precision. Their sugar conveying systems are engineered to prevent blockages, handle high humidity conditions, and ensure a dust-free environment. By utilizing state-of-the-art technology, Headpowder ensures that the sugar remains free-flowing and uncontaminated throughout the entire transportation process. Whether the requirement is for a new installation or an upgrade to an existing facility, their expertise in sugar pneumatic conveying provides a seamless solution that enhances production safety and efficiency.
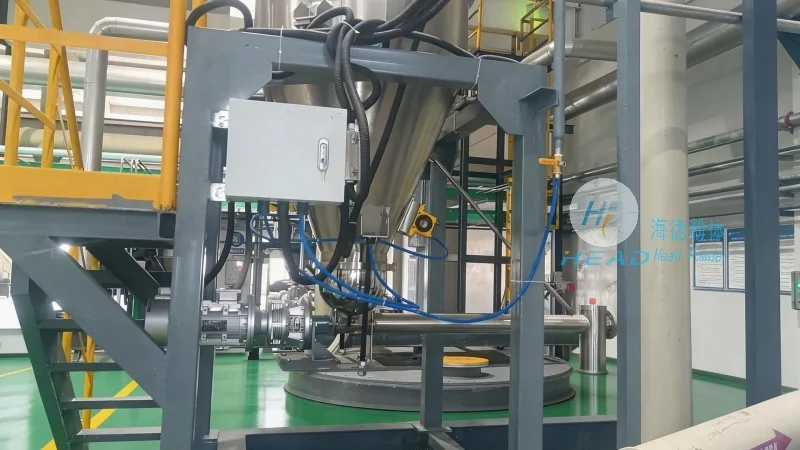
Choosing the right partner for your material handling needs is essential for long-term success. If you are looking for professional guidance on sugar conveying systems or require a custom solution for material conveying, please do not hesitate to contact the team at Shandong Headpowder Engineering Co., Ltd. You may reach out directly to Zhang Manager for a detailed consultation. They are ready to assist you with technical specifications and project planning to ensure your operations run smoothly.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top