With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and supply of advanced powder conveying systems tailored for the cement and fly ash industries. Based in Shandong, China, the company leverages decades of expertise to deliver reliable solutions that enhance operational efficiency and safety in bulk material handling. This article explores the working principle and key features of their cement fly ash powder conveying system equipment, providing insights into how these systems operate and the advantages they offer to industrial clients.
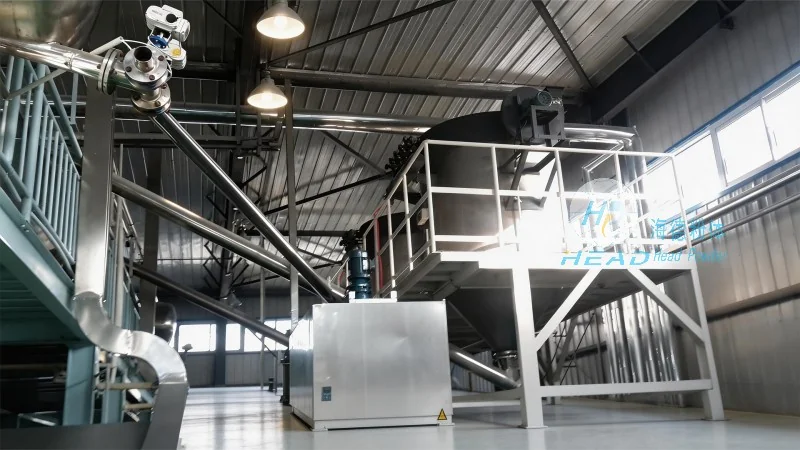
The cement fly ash powder conveying system is a sophisticated piece of industrial equipment engineered to transport bulk powders such as cement and fly ash from storage silos to processing units or end-use applications. It combines advanced pneumatic conveying technology with robust mechanical components to ensure efficient, low-maintenance operation. The system is designed to handle high volumes of fine powders while maintaining consistent flow rates and minimizing material degradation.
The core of the system operates on the principle of pneumatic conveying, where compressed air is used to transport the powder through a network of pipes. The process begins with the material being drawn from the storage silo by a vacuum or pressure source, depending on the system configuration. The powder is then carried through the pipeline by the airflow, which can be either positive pressure (blowing air into the line) or negative pressure (sucking air out of the line). The system includes key components such as a feeder, a conveying line, a control valve, and a receiver, all working in tandem to ensure smooth material transfer.
During operation, the feeder regulates the flow of powder from the silo, ensuring a consistent feed rate that matches the conveying capacity of the system. The conveying line, typically made of corrosion-resistant materials like stainless steel or polyethylene, transports the powder while minimizing friction and particle attrition. The control valve, often a rotary or slide valve, manages the flow direction and pressure within the system, allowing for precise control over the material movement. The receiver, where the powder is deposited, is equipped with dust collection and filtration systems to maintain air quality and prevent material loss.
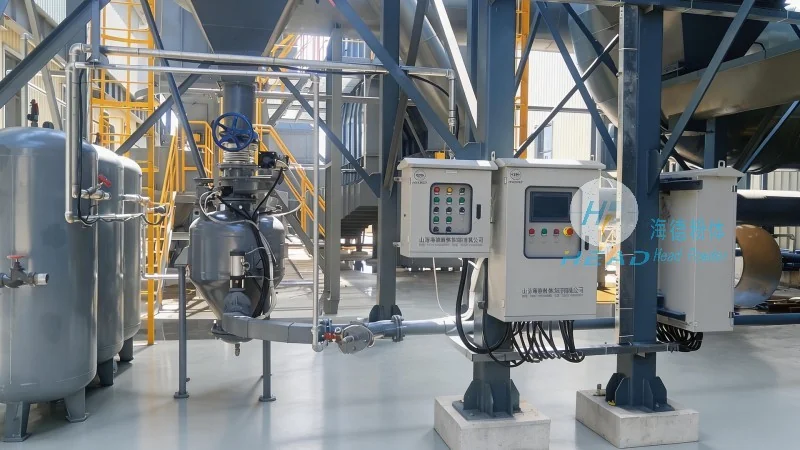
Shandong HeadPowder Engineering Co., Ltd.'s cement fly ash powder conveying system is distinguished by several key features that enhance its performance and reliability. One of the primary advantages is its ability to handle high volumes of fine powders with minimal pressure drop, ensuring efficient material transport over long distances. The system is also designed for low maintenance, with components that are easy to access and replace, reducing downtime and operational costs.
Another notable feature is the system's adaptability to different material characteristics. It can be configured to handle various particle sizes and moisture contents, making it suitable for a wide range of applications in the cement and fly ash industries. The equipment also incorporates advanced control systems that allow for real-time monitoring of flow rates, pressure, and temperature, enabling operators to optimize performance and detect potential issues before they escalate.
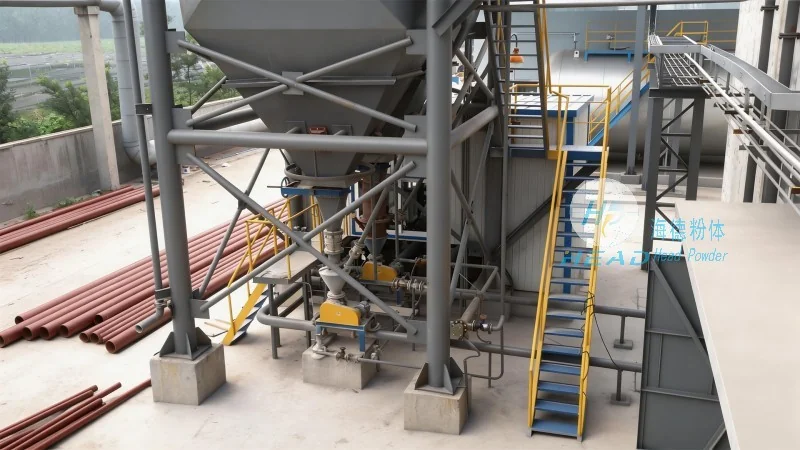
The system's design prioritizes safety and environmental compliance. It includes features such as dust suppression and filtration to minimize airborne particulates, which is crucial for maintaining a safe working environment and meeting regulatory standards. Additionally, the equipment is built to withstand the corrosive nature of cement and fly ash, with materials that resist wear and degradation over time.
The cement fly ash powder conveying system is widely used in the cement manufacturing process, where it efficiently transports raw materials and byproducts between production stages. It is also utilized in power plants and other industrial facilities that generate fly ash, ensuring that this valuable material is properly handled and utilized. By improving the efficiency of material handling, the system contributes to overall operational productivity and cost savings for industrial clients.
In summary, the cement fly ash powder conveying system from Shandong HeadPowder Engineering Co., Ltd. represents a reliable and efficient solution for bulk powder transport. Its working principle, based on pneumatic conveying technology, combined with advanced features such as low maintenance, adaptability, and safety measures, makes it an ideal choice for industries requiring consistent and reliable material handling. The company's commitment to quality and innovation ensures that their systems meet the evolving needs of the cement and fly ash sectors, providing long-term value to their clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top