

Working Principle and Features of Maltose Powder Conveyors
For industries dealing with maltose powder, efficient and reliable material handling is crucial. The maltose powder conveyor, a specialized piece of equipment designed for transporting maltose powder, plays a vital role in ensuring smooth production processes. This article will explore the working principle and key features of such conveyors, providing insights into how they operate and why they are essential in modern industrial applications.
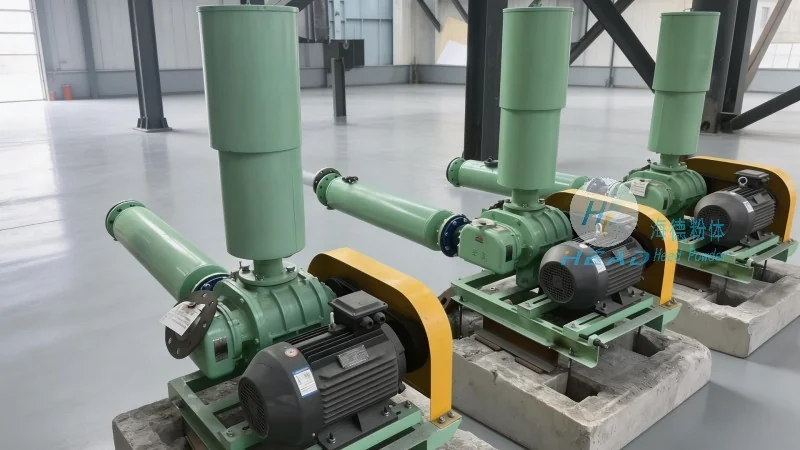
Introduction to Maltose Powder Conveyors
Maltose powder conveyors are engineered to handle the unique properties of maltose powder, which can be hygroscopic and prone to bridging or caking under certain conditions. The design of these conveyors addresses these challenges by incorporating features that promote uniform flow and prevent material buildup. As a result, they offer enhanced efficiency and safety in the handling of maltose powder, making them indispensable in food processing, pharmaceutical, and chemical industries where maltose is used as a sweetener or raw material.
Key Components and Working Principle
The working principle of a maltose powder conveyor typically involves a combination of mechanical and pneumatic components. The system often includes a hopper for material storage, a feeding mechanism to control the flow rate, and a conveyor section that transports the powder to the desired destination. In many designs, a screw or auger mechanism is used to move the powder, while an airlock or rotary valve ensures airtight transfer and prevents dust emissions. The conveyor may also feature a dust collection system to maintain a clean and safe working environment.
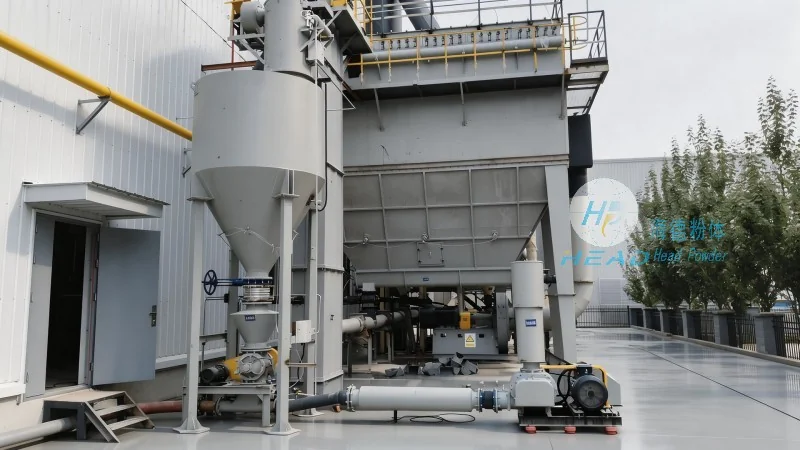
During operation, the maltose powder is first fed from the storage hopper into the conveyor's feeding section. The screw or auger rotates, pushing the powder forward through the conveyor tube. The airlock or rotary valve at the discharge end regulates the flow, ensuring that the powder is released in a controlled manner without causing blockages or spills. This mechanism is designed to handle the hygroscopic nature of maltose powder, as it prevents moisture absorption and maintains the powder's quality throughout the transfer process.
Features and Advantages of Maltose Powder Conveyors
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of high-quality maltose powder conveyors. Their products are characterized by several key features that enhance performance and reliability. One of the primary advantages is the use of stainless steel construction, which ensures durability and resistance to corrosion, even when handling moisture-sensitive materials like maltose. The conveyor systems are also equipped with advanced control systems that allow for precise adjustment of flow rates, ensuring consistent and uniform material transfer.
Another notable feature is the integration of dust suppression and filtration systems. These components help maintain a clean working environment by capturing airborne particles and preventing dust contamination of the maltose powder. This is particularly important in industries where product purity is paramount, such as pharmaceuticals or food processing. Additionally, the conveyors are designed with easy maintenance in mind, featuring accessible components and quick-release mechanisms that reduce downtime and maintenance costs.
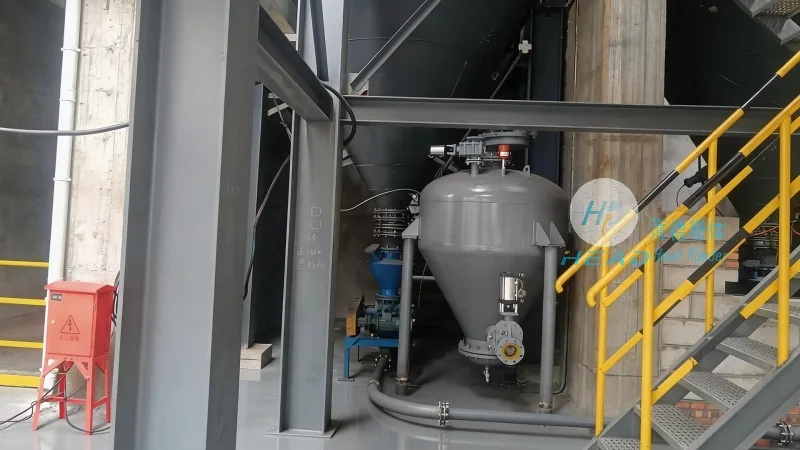
The maltose powder conveyors from HeadPowder Engineering Co., Ltd. also offer flexibility in terms of customization. Depending on the specific requirements of the application, the conveyor can be adjusted to handle different powder types, flow rates, and discharge heights. This adaptability makes them suitable for a wide range of industrial processes, from small-scale production lines to large-scale manufacturing facilities.
Conclusion
In conclusion, maltose powder conveyors are essential equipment for industries that rely on maltose powder. The working principle, which combines mechanical and pneumatic components, ensures efficient and safe material handling. The key features, such as stainless steel construction, advanced control systems, and dust suppression, enhance performance and maintain product quality. As a manufacturer based in Shandong, China, HeadPowder Engineering Co., Ltd. provides reliable and high-quality maltose powder conveyors that meet the demands of modern industrial applications. Their commitment to innovation and customer satisfaction makes them a trusted partner for businesses seeking efficient material handling solutions.