With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Intelligent centralized powder conveying equipment represents a sophisticated solution for the efficient and reliable transport of bulk powders and granular materials across various industrial applications. This technology is pivotal in sectors such as pharmaceuticals, food processing, chemical manufacturing, and mining, where the safe handling of powders is critical to product quality and operational safety. The equipment integrates advanced automation, control systems, and material handling technologies to optimize the entire conveying process, ensuring consistent performance and minimal downtime.
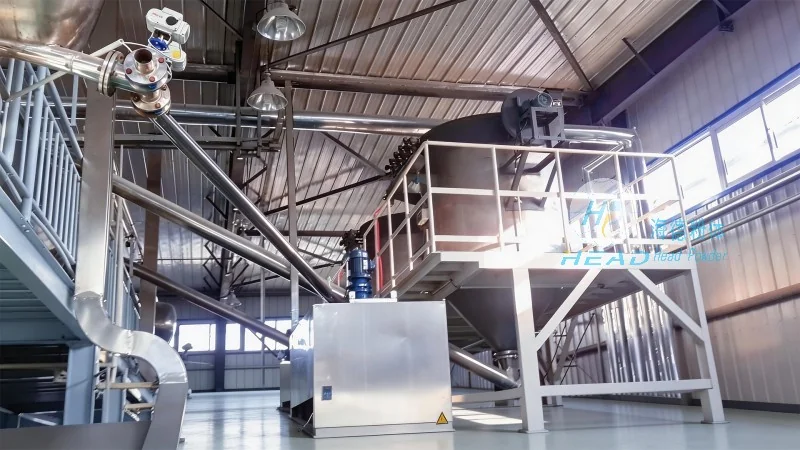
The fundamental working principle of intelligent centralized powder conveying equipment centers on a network of interconnected components that collaborate to achieve seamless material transport. The process typically begins at a material feeding station where powders are introduced into the conveying line. From this point, the material is propelled through a series of pipes or hoses using positive displacement or pneumatic pressure mechanisms. The intelligent control system continuously monitors and adjusts parameters such as flow rate, pressure, and temperature in real-time, ensuring optimal operational conditions. Key components include feeders, conveyors, valves, and sensors that work in tandem to maintain consistent material movement. The system can be programmed to handle diverse powder types, adjust conveying speeds based on material properties, and automatically detect and respond to blockages or abnormalities, thereby preventing disruptions and maintaining system integrity.
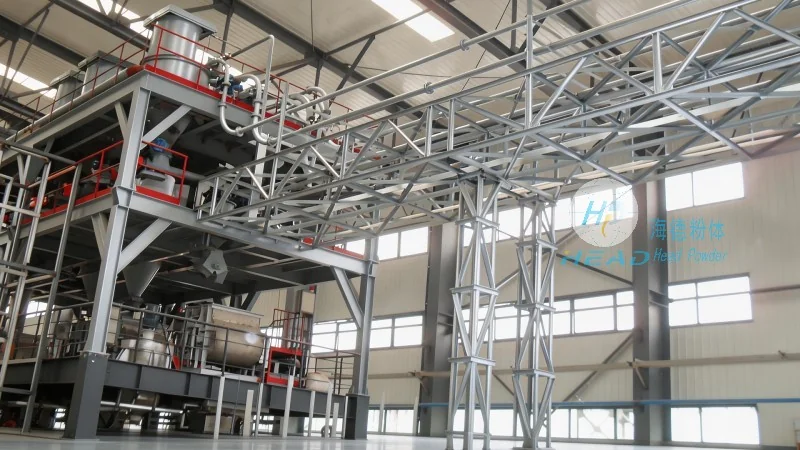
Intelligent centralized powder conveying equipment is distinguished by several advanced features that enhance its functionality and user experience. A primary feature is its centralized control capability, enabling operators to manage multiple conveying lines from a single interface. This reduces the need for on-site manual adjustments and improves overall operational efficiency. The equipment also incorporates advanced sensors and monitoring systems that provide real-time data on material flow, pressure, and temperature, which is crucial for maintaining product quality and preventing equipment damage. Another notable feature is the ability to integrate with other industrial systems, such as inventory management and production scheduling software, facilitating seamless coordination between material handling and production processes. The modular design of the equipment allows for easy expansion or modification as production needs evolve, providing flexibility for growing businesses. Additionally, the intelligent control system includes predictive maintenance capabilities, which can detect potential equipment issues before they cause downtime, further reducing maintenance costs and improving system reliability.
The intelligent centralized powder conveying equipment from Shandong HeadPowder Engineering Co., Ltd. offers significant advantages for industrial operations. The system's high conveying efficiency and precision ensure powders are transported with minimal loss and contamination, which is essential for industries like pharmaceuticals and food processing where product purity is paramount. The centralized control feature simplifies operation and reduces the need for specialized training, making it accessible to a wide range of industrial users. The advanced monitoring and control capabilities enhance safety by preventing overpressure or material blockages that could lead to accidents. Furthermore, the equipment's modular design allows for easy integration into existing production lines, minimizing installation time and costs. The predictive maintenance feature helps reduce unexpected downtime, ensuring consistent production output. Overall, the intelligent centralized powder conveying equipment provides a reliable and efficient solution for bulk powder handling, contributing to improved productivity and reduced operational costs across various industrial sectors.
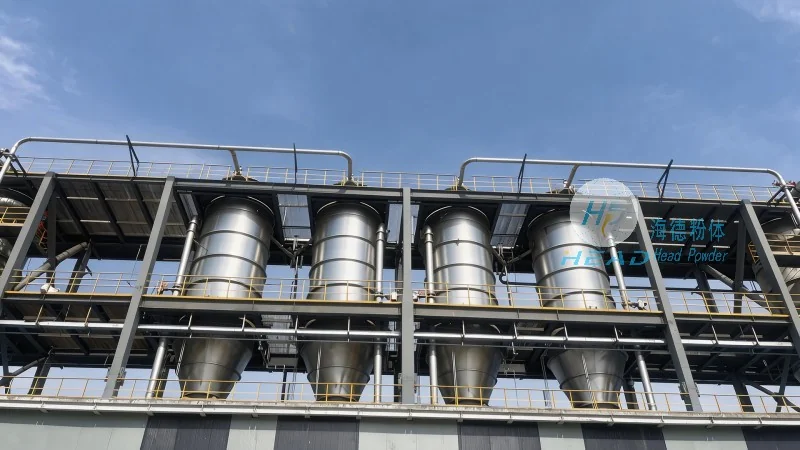
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of advanced powder handling equipment. The company is headquartered in Shandong, China, and has built a strong reputation for delivering high-quality, reliable, and innovative solutions to the global market. With years of experience in the industry, headpowder has developed a deep understanding of the unique challenges faced by different industries when handling powders. This expertise is reflected in the design and manufacturing of their intelligent centralized powder conveying equipment, which incorporates the latest technologies and best practices. The company adheres to strict quality control standards to ensure each product meets or exceeds industry specifications. Additionally, headpowder provides comprehensive after-sales support, including installation, training, and maintenance services, to help customers maximize the performance and lifespan of their equipment. The company's commitment to customer satisfaction and technological advancement has made it a trusted partner for businesses seeking efficient and reliable powder conveying solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top