With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Compound fertilizer powder conveying equipment plays a crucial role in the efficient handling and transportation of bulk fertilizer materials in agricultural and industrial applications. As a key component in modern fertilizer production and distribution systems, these specialized machines ensure reliable and safe movement of powdered fertilizers from storage silos, processing units, or packaging lines to various end-use points. The design and functionality of such equipment are tailored to meet the unique challenges of handling fine, dry powders, which require precise control to prevent issues like caking, segregation, or material loss.
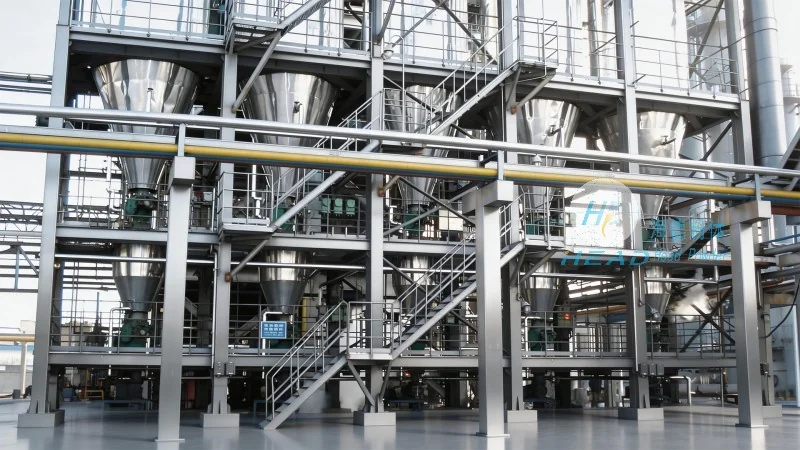
The operation of compound fertilizer powder conveying equipment typically involves several integrated components working in concert to achieve efficient material transport. The core mechanism often relies on positive displacement or pneumatic conveying technologies, depending on the specific application requirements and material characteristics. Positive displacement systems, such as rotary lobe blowers or screw conveyors, use mechanical action to push the powder through a pipeline under pressure. In contrast, pneumatic conveying systems utilize compressed air or other gases to create a flow that carries the powder particles through the system. Both approaches are designed to maintain consistent flow rates and prevent material degradation during transport.
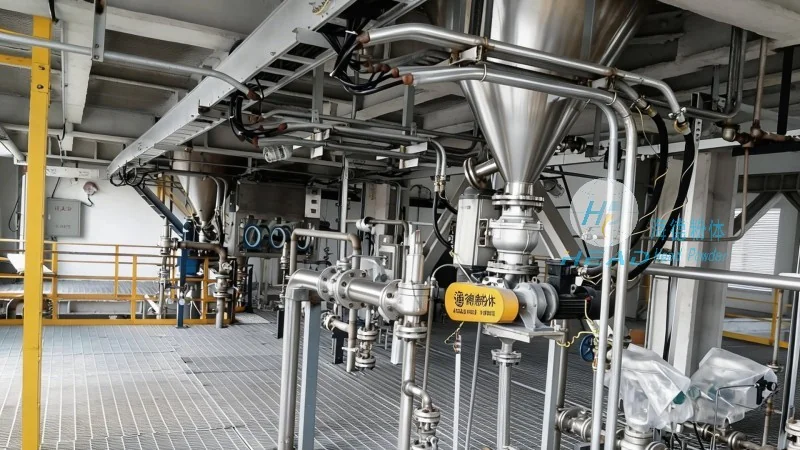
Key components in the system include the feeding hopper, which collects and feeds the fertilizer powder into the conveying line; the conveyor itself, which may be a tube or duct system; and the control valves and regulators that manage the flow and pressure. The feeding hopper is equipped with level sensors and sometimes vibration or agitation systems to prevent material bridging or clogging, ensuring a steady supply of powder to the conveyor. The conveyor line is often made of materials like stainless steel or food-grade plastic to withstand the corrosive nature of fertilizers and maintain hygiene standards. Pressure sensors and flow meters are integrated into the system to monitor performance and adjust parameters in real-time, optimizing the conveying process for maximum efficiency.
Compound fertilizer powder conveying equipment is characterized by several distinct features that enhance its performance and reliability in demanding environments. One of the primary features is its ability to handle fine, dry powders without causing segregation or agglomeration. This is achieved through specialized hopper designs with smooth internal surfaces and optional agitators or vibrators that prevent material from settling unevenly. The equipment also incorporates advanced sealing and dust control mechanisms to minimize environmental contamination and ensure operator safety. For example, some models use double-seal systems or dust collection hoods to capture and filter fine particles, complying with industrial hygiene regulations.
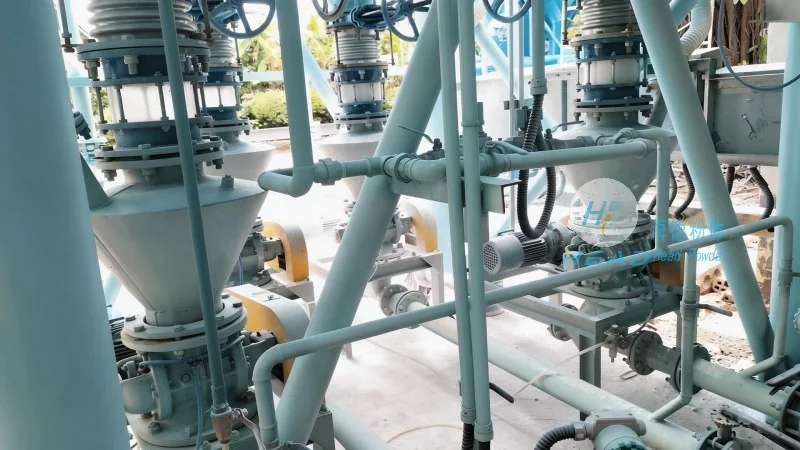
Another important feature is the system's adaptability to different fertilizer types and particle sizes. Many conveying systems are designed with adjustable speed controls and variable pressure settings, allowing operators to tailor the conveying parameters to the specific characteristics of the fertilizer being handled. This flexibility is particularly valuable when processing different compound fertilizers, which may have varying moisture content, bulk density, or flowability. The equipment also includes safety features such as emergency shut-off valves, pressure relief devices, and overload protection to prevent accidents and equipment damage during operation.
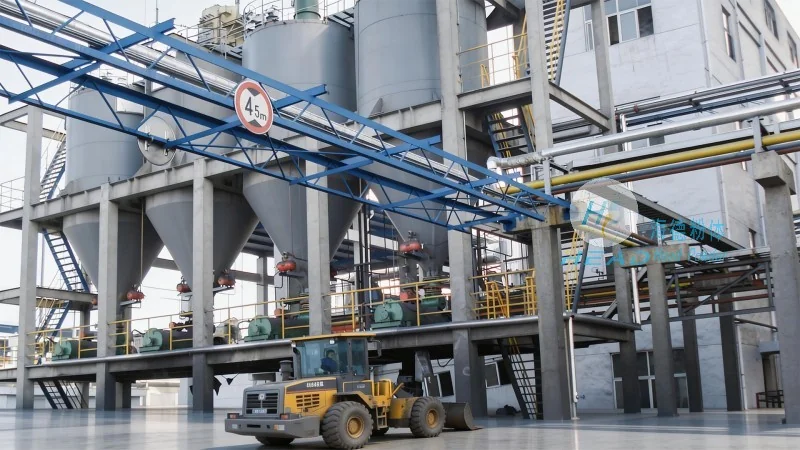
Energy efficiency is another notable feature of modern compound fertilizer powder conveying equipment. Advanced models incorporate energy-saving technologies, such as variable frequency drives (VFDs) that adjust motor speed based on the required flow rate, reducing unnecessary energy consumption. Additionally, the use of high-efficiency conveyor components and optimized system design minimizes power loss, contributing to lower operational costs and reduced environmental impact. The equipment's durability and low maintenance requirements further enhance its economic viability, as it can operate continuously for extended periods with minimal downtime.
As a leading manufacturer of compound fertilizer powder conveying equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality, customized solutions for the fertilizer industry. With years of experience in the field, the company has developed a reputation for producing reliable and efficient equipment that meets the stringent requirements of modern agricultural and industrial applications. HeadPowder's products are designed and manufactured in China, leveraging advanced engineering and quality control processes to ensure superior performance and durability. The company's commitment to innovation and customer satisfaction has made it a trusted partner for fertilizer producers and distributors worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top