With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as headpowder, is a leading manufacturer specializing in advanced powder handling systems for the cement industry. The cement raw material powder conveying system is a critical infrastructure component in cement production, responsible for transporting raw materials like limestone, clay, and iron ore from storage silos to the preheater or kiln. This system is essential for maintaining the continuity and efficiency of the cement manufacturing process, as it ensures that raw materials are delivered to the next stage of production without interruption.
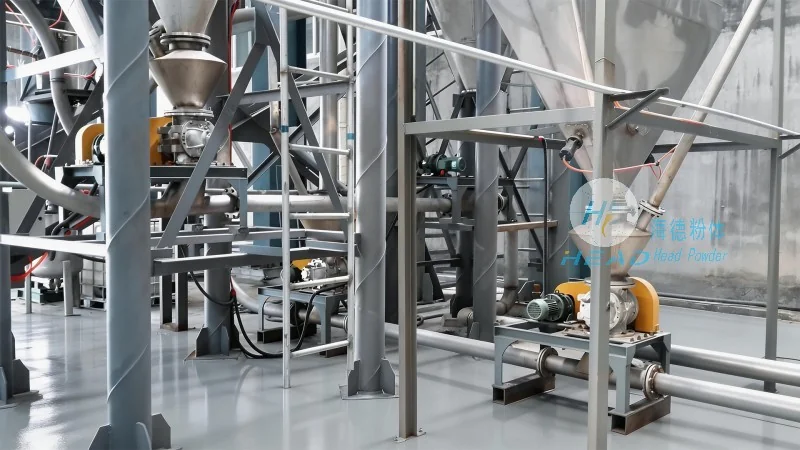
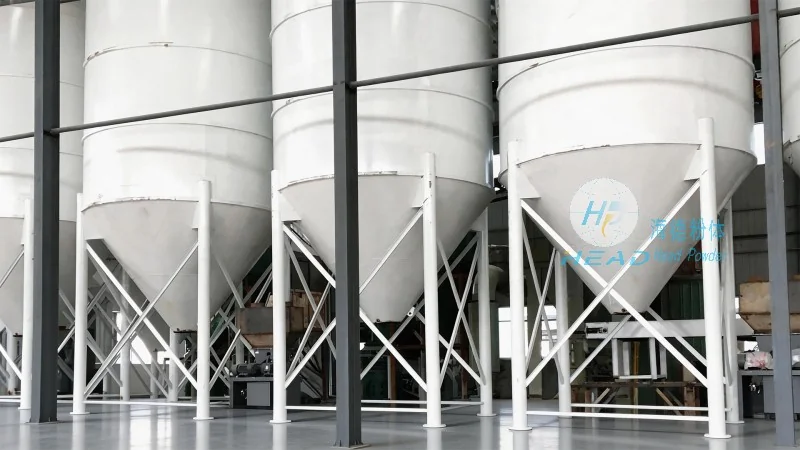
The core technology behind the cement raw material powder conveying system is pneumatic conveying, which utilizes air as the transport medium. The system operates by creating a pressure differential between the feeding and receiving points. In a negative pressure system, a fan draws air through the pipeline, creating a vacuum that pulls the raw material powder from the silo into the pipeline. The powder is then carried by the airflow to the destination, such as the preheater or kiln. In a positive pressure system, a blower pushes air and powder through the pipeline, ensuring the material is transported under pressure. The system may also combine both negative and positive pressure zones to optimize performance for different material characteristics and pipeline lengths. The process typically involves feeders that discharge raw materials into the pipeline, a conveying pipeline network, and separation equipment at the receiving end to recover the powder and recycle the air.
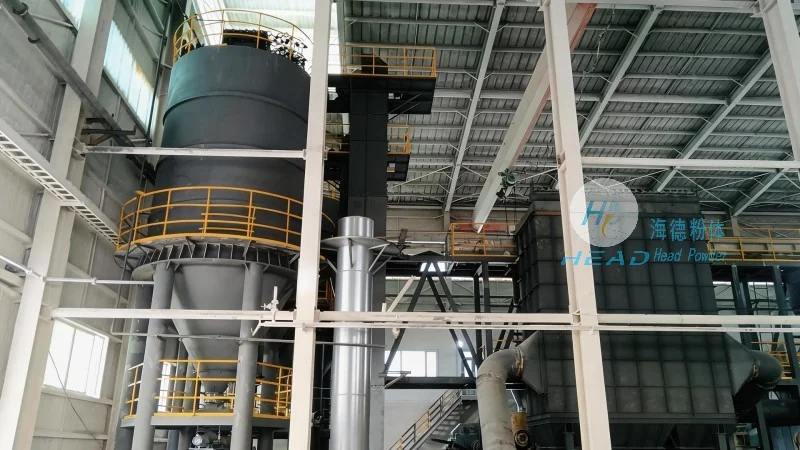
HeadPowder's cement raw material powder conveying system is designed with several key features that enhance its performance and reliability. One primary feature is high conveying efficiency, which minimizes material loss and ensures consistent flow rates. The system incorporates advanced control systems for real-time monitoring and adjustment of the conveying process, allowing operators to maintain optimal operation under varying conditions. Constructed with high-quality materials like stainless steel and corrosion-resistant alloys, the system withstands the harsh cement production environment and extends equipment service life. Another notable feature is customization flexibility, enabling the system to accommodate different raw material types and production capacities, making it suitable for various cement plant scales. Additionally, the system includes energy-efficient air recycling and separation mechanisms, reducing operational costs and environmental impact.
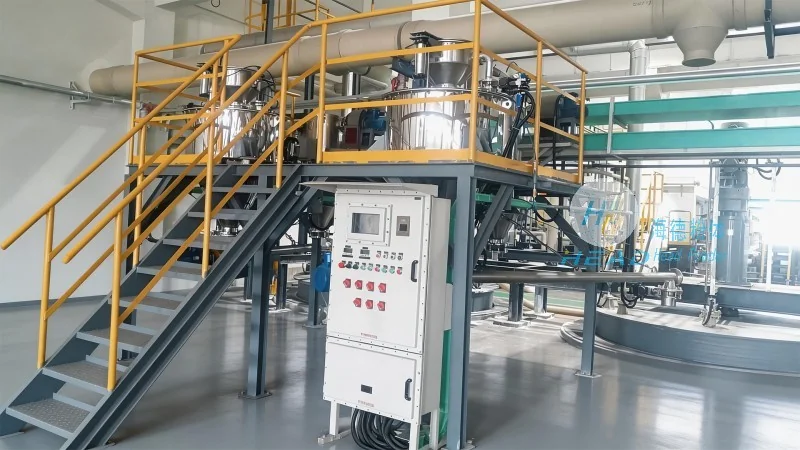
The cement raw material powder conveying system from Shandong HeadPowder Engineering Co., Ltd. offers significant advantages to cement manufacturers. By ensuring efficient and continuous material transport, the system reduces downtime and improves overall plant productivity. The ability to handle large volumes of raw materials with minimal maintenance requirements contributes to cost savings. The system's design minimizes dust emissions and aligns with modern environmental standards. These advantages make it a reliable choice for cement plants seeking to enhance production capabilities and maintain operational excellence.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top