With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the working principle and features of brown sugar powder conveying systems is crucial for optimizing industrial processes in the sugar and food processing sectors. These systems are designed to handle the unique properties of brown sugar, such as its granular structure, moisture content, and tendency to agglomerate, ensuring efficient and reliable material transport from storage to processing or packaging stages.
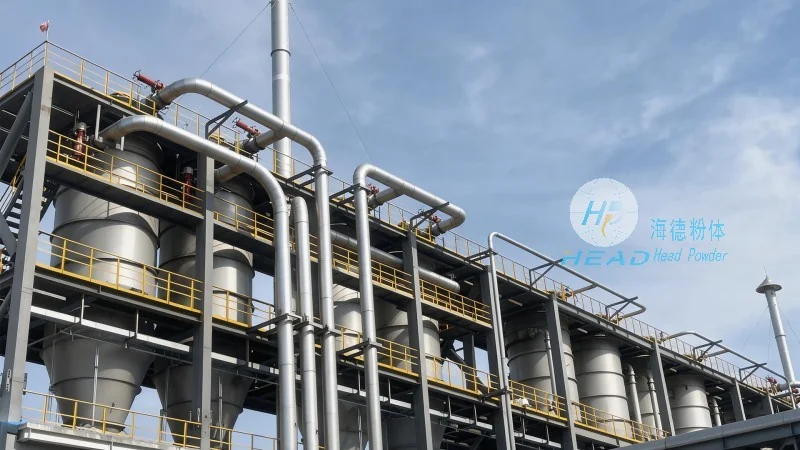
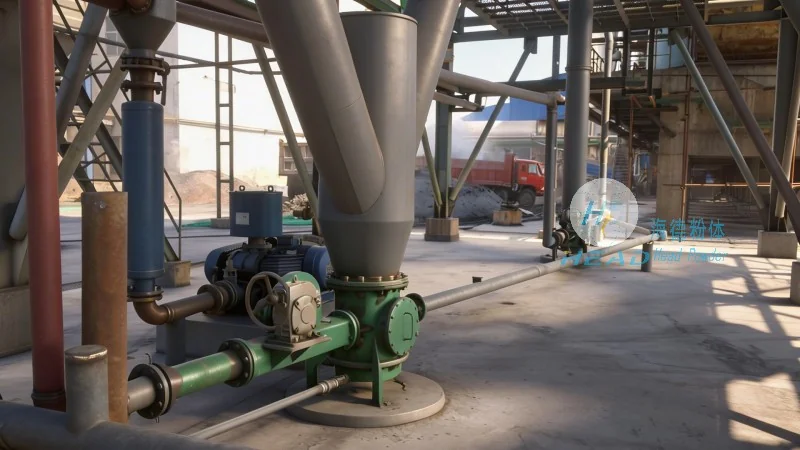
Brown sugar powder conveying systems typically operate based on mechanical or pneumatic principles, tailored to the specific characteristics of the material. The core components include feeders, conveyors, and control mechanisms that work in tandem to move the powder through the system. For mechanical systems, screw conveyors or belt conveyors are commonly used, which rely on rotational motion to transport the material. These conveyors are often equipped with special coatings or materials to prevent sticking and ensure smooth flow. Pneumatic systems, on the other hand, utilize air pressure to move the powder through pipes, which can be more suitable for handling fine powders that are prone to dust generation. The system's control unit monitors parameters like flow rate, pressure, and temperature to maintain consistent performance and prevent blockages or overloading.
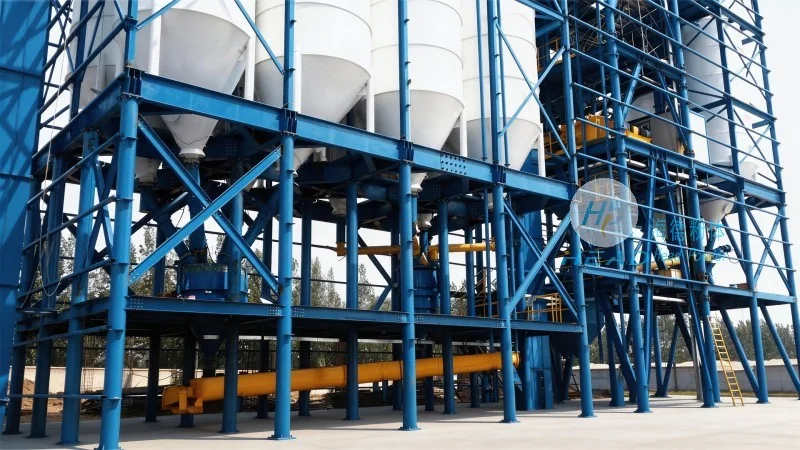
Effective brown sugar powder conveying systems exhibit several key features that enhance their performance and reliability. One of the primary features is the ability to handle variable particle sizes and moisture levels without compromising efficiency. This is achieved through adjustable feed mechanisms and variable speed controls that adapt to the material's changing properties. Another important feature is the system's hygienic design, which is critical in food processing applications. Components such as hoppers, conveyors, and discharge points are often made from stainless steel and designed to minimize dead zones, making cleaning and maintenance straightforward. Additionally, many modern systems incorporate dust suppression and filtration systems to comply with environmental regulations and ensure worker safety. The integration of sensors and real-time monitoring further enhances operational efficiency by providing immediate feedback on system performance and alerting operators to potential issues before they escalate.
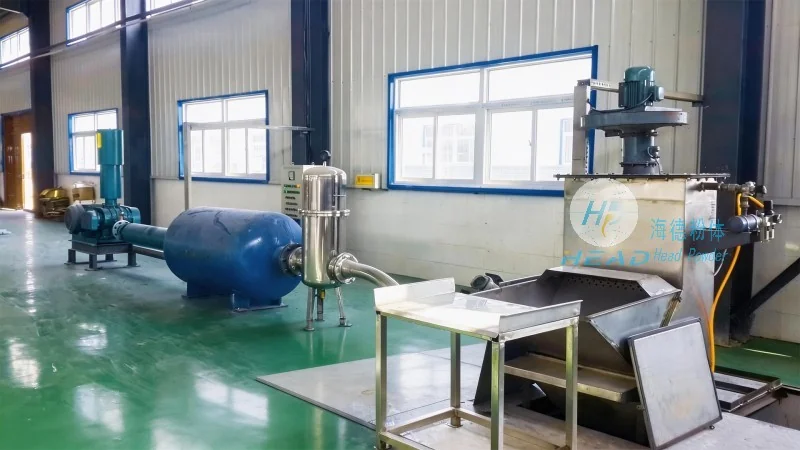
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of advanced powder handling solutions. With a focus on industrial applications, the company has developed expertise in creating customized conveying systems tailored to the unique needs of clients in the food, pharmaceutical, and chemical industries. Headpowder's commitment to quality and innovation is reflected in their use of high-grade materials and advanced engineering techniques, ensuring that their systems meet or exceed industry standards. The company's facilities are located in Shandong, China, where they leverage local resources and expertise to deliver reliable and efficient solutions for powder transport challenges.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top