

What is a Metering Bin Pump Powder Pneumatic Conveying Machine? And What Are Its Design Principles?
Welcome to the world of advanced powder handling technology, where precision and efficiency are paramount. Today, we delve into the specifics of the metering bin pump, a critical component in modern pneumatic conveying systems. This article will explore what a metering bin pump is, its fundamental design principles, and why it stands as a reliable solution for handling bulk powders in various industrial applications.
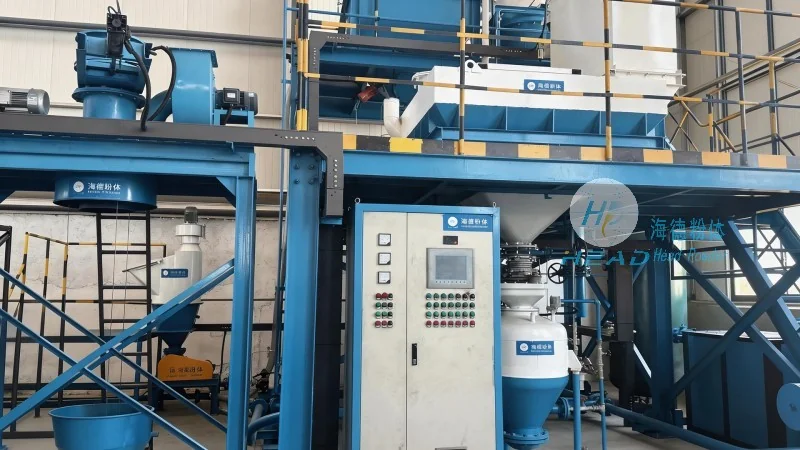
Introduction to Metering Bin Pump Pneumatic Conveying Systems
A metering bin pump, often referred to as a bin pump or a positive displacement pump for powders, is a specialized device designed to transport dry bulk materials through a pneumatic system. The system operates by creating a pressure differential, typically using compressed air or other gases, to move the powder from a storage bin or hopper to the destination point. This technology is widely used across industries such as pharmaceuticals, food processing, chemicals, and mining, where the safe and efficient transfer of powders is essential.
Understanding the Core Components and Functionality
The metering bin pump consists of several key components that work in tandem to ensure smooth operation. At its heart is the bin or hopper, which holds the bulk material. The pump itself includes a piston or diaphragm mechanism that moves in a reciprocating motion, creating a vacuum or pressure to draw and discharge the powder. The system also features a control valve that regulates the flow rate, ensuring precise metering of the material. Additionally, the conveying line connects the pump to the discharge point, often equipped with filters and check valves to prevent backflow and maintain system integrity.
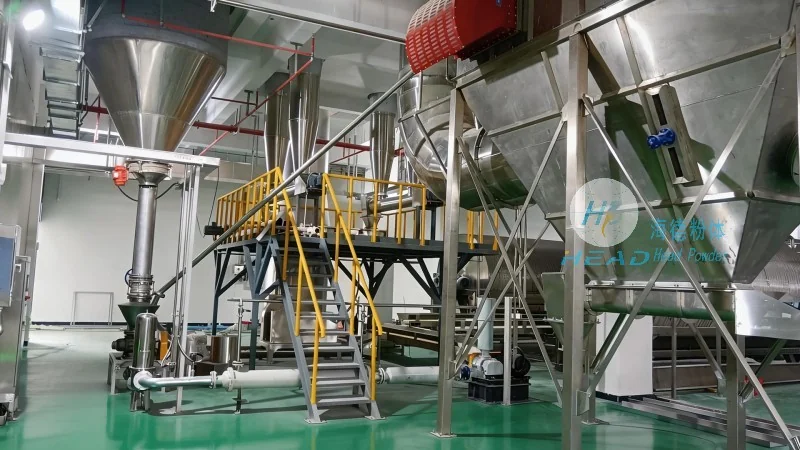
Design Principles Behind the Metering Bin Pump
The design of a metering bin pump is rooted in principles of fluid dynamics and mechanical engineering. The primary goal is to achieve consistent and controlled flow of powders, which is critical for applications requiring accurate dosing or uniform mixing. The pump's design considers factors such as the particle size distribution of the material, the density and flowability of the powder, and the required discharge rate. Engineers use computational fluid dynamics (CFD) and empirical data to optimize the pump's dimensions, including the piston stroke, cylinder volume, and air pressure settings. The result is a system that minimizes pressure drop, reduces wear on components, and maximizes the efficiency of powder transfer.
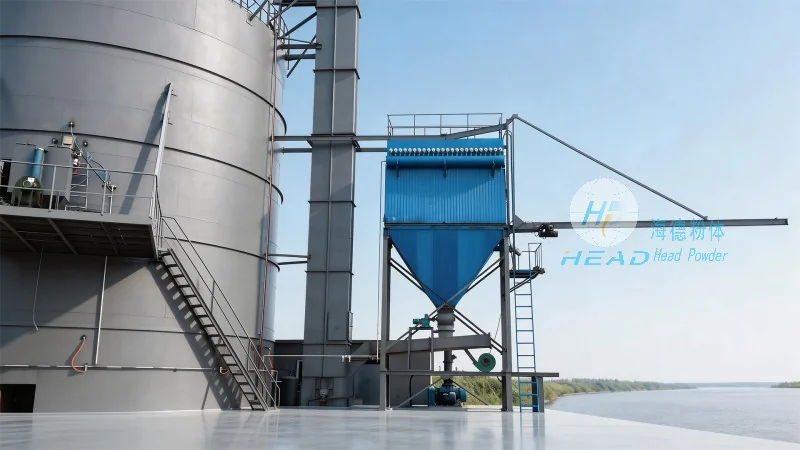
Key Features and Advantages of the System
One of the standout features of the metering bin pump is its ability to handle a wide range of powder types, from fine powders like talc to coarse materials like sand. The system is also highly flexible, allowing for adjustments in flow rate by modifying the air pressure or pump speed. This adaptability makes it suitable for both small-scale laboratory applications and large-scale industrial operations. Another advantage is the system's ability to operate in a closed loop, reducing dust emissions and improving safety in the workplace. The metering bin pump also offers low maintenance requirements, as the moving parts are designed to withstand the abrasive nature of powders, and the system is equipped with self-lubricating components to extend service life.
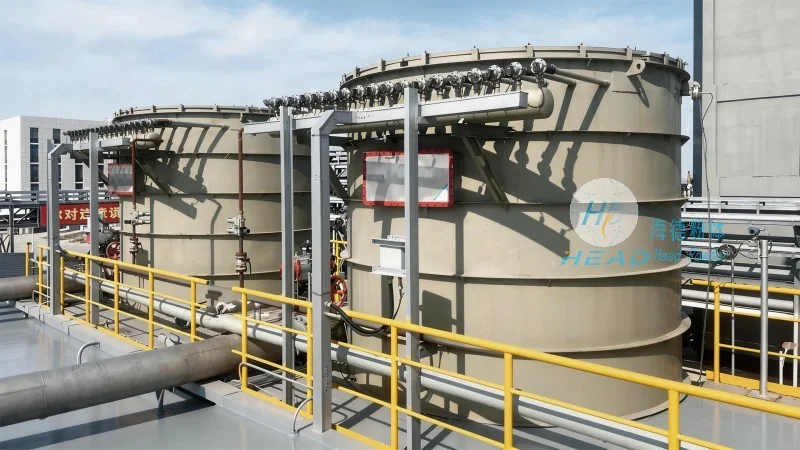
Application Scenarios and Operational Benefits
The metering bin pump is employed in various scenarios where precise powder handling is non-negotiable. In the pharmaceutical industry, for example, it is used to transfer active pharmaceutical ingredients (APIs) and excipients with high accuracy, ensuring consistent batch quality. In food processing, it handles ingredients like flour, sugar, and spices, maintaining hygiene standards and preventing contamination. In chemical manufacturing, the pump transfers raw materials and intermediates, supporting continuous production processes. The operational benefits of this system include reduced downtime due to its robust design, lower energy consumption compared to other conveying methods, and the ability to handle materials that are difficult to transport using traditional methods such as belt conveyors or screw conveyors.
Company Information and Technical Support
HeadPowder, a leading manufacturer of powder handling equipment, specializes in the design and production of metering bin pumps. With a strong commitment to quality and innovation, HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., has been serving industries worldwide since its establishment in Shandong, China. The company's team of engineers and technicians leverages advanced manufacturing techniques and rigorous quality control processes to deliver reliable and efficient metering bin pumps. HeadPowder provides comprehensive technical support, including installation guidance, maintenance services, and customized solutions tailored to specific customer needs. By choosing HeadPowder, industries can ensure the longevity and optimal performance of their pneumatic conveying systems, enhancing productivity and reducing operational costs.