With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the Brown Sugar Powder Conveying System Equipment and Its Design Principles
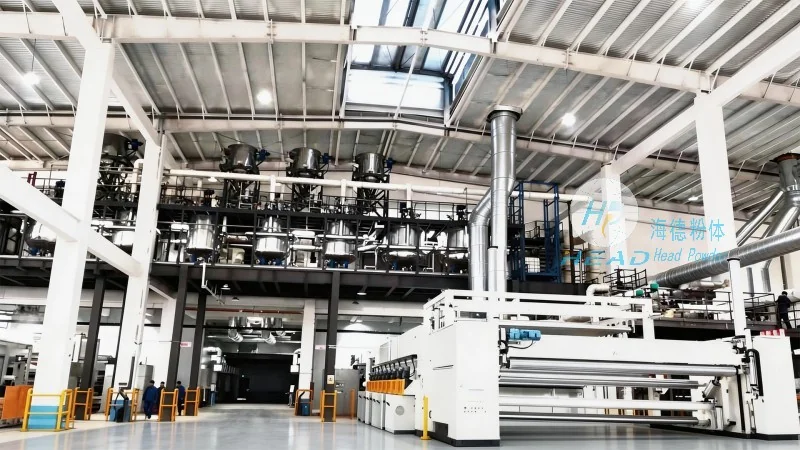
For businesses involved in the processing and handling of brown sugar, an efficient and reliable powder conveying system is essential. The brown sugar powder conveying system equipment, as offered by Shandong HeadPowder Engineering Co., Ltd., is a specialized solution designed to address the unique challenges associated with transporting fine brown sugar particles. This system plays a crucial role in ensuring smooth operations from raw material intake to final product packaging, minimizing material loss and enhancing overall productivity.
The design of the brown sugar powder conveying system equipment is built on a combination of proven engineering principles and practical application. At its core, the system typically comprises several key components that work in tandem to achieve effective material transport. These include a series of airtight pipelines, a high-efficiency dust collector, and a variable-speed fan or blower. The airtight pipelines are constructed from materials resistant to corrosion and abrasion, such as stainless steel or specialized plastic composites, ensuring durability and preventing contamination of the brown sugar powder. The dust collector is integrated to capture any airborne particles, maintaining air quality and complying with environmental regulations. The variable-speed fan allows for precise control over the air flow, which is critical for adjusting the conveying speed based on the particle size and density of the brown sugar. Additionally, the system may incorporate check valves and pressure relief devices to regulate the flow and prevent backflow, ensuring safe and stable operation.
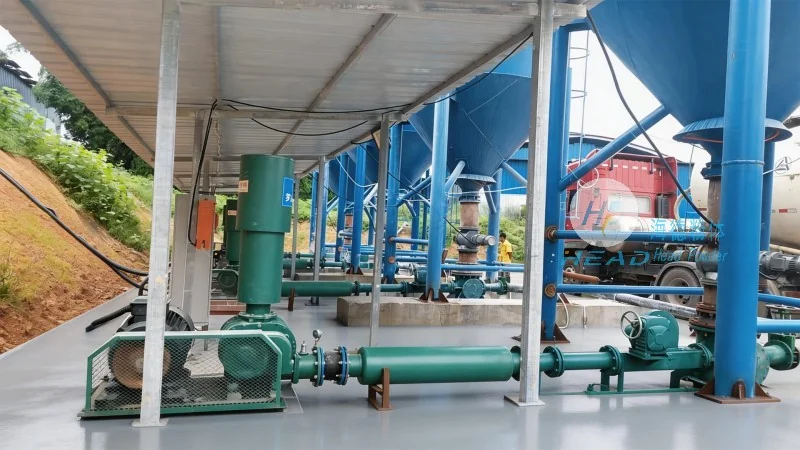
The operation of the brown sugar powder conveying system equipment follows a systematic process that ensures consistent and reliable transport of brown sugar powder. The process begins with the loading of brown sugar into a hopper or storage silo. From there, the material is drawn into the airtight pipeline system by the fan, which creates a negative pressure environment. The air flow carries the brown sugar particles through the pipelines to the desired destination, such as a processing unit or packaging area. The system is equipped with sensors and control panels that allow operators to monitor the flow rate, pressure, and temperature in real-time. This allows for immediate adjustments to maintain optimal performance. The dust collector continuously filters the air, capturing any fine particles and returning clean air back to the system or to the environment, depending on the setup. The entire system is designed to operate with minimal maintenance, thanks to its robust construction and advanced control mechanisms.
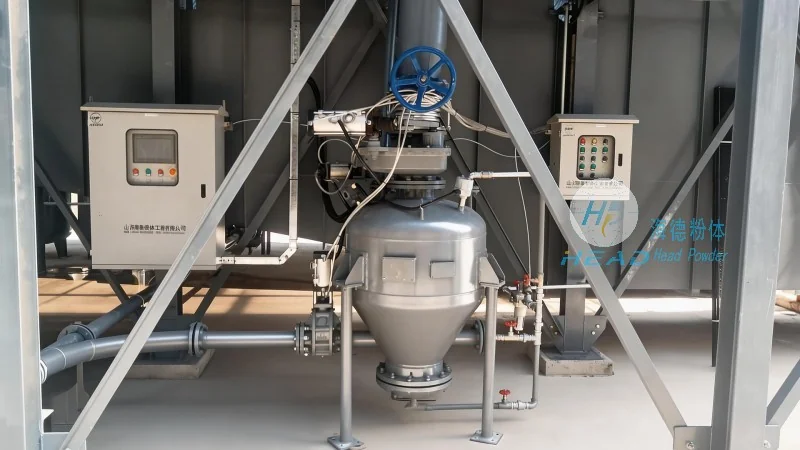
Implementing a brown sugar powder conveying system from Shandong HeadPowder Engineering Co., Ltd. offers numerous benefits for businesses in the sugar industry. One of the primary advantages is the significant reduction in material handling time and labor costs. By automating the transport process, the system minimizes the need for manual handling, which not only improves efficiency but also reduces the risk of product contamination and worker injury. Another key benefit is the reduction in material loss and degradation. The airtight design and controlled air flow prevent moisture absorption and oxidation, which can affect the quality and shelf life of brown sugar. This leads to higher product quality and customer satisfaction. Furthermore, the system's modular design allows for easy integration with existing production lines, making it a flexible solution for businesses of various sizes. The energy-efficient operation, thanks to the variable-speed fan, also contributes to lower operational costs and reduced environmental impact.
As a leading manufacturer of specialized powder handling equipment, Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted partner for businesses in the food and chemical industries. With a strong commitment to quality and innovation, the company designs and manufactures equipment tailored to meet the specific needs of its clients. HeadPowder's team of experienced engineers and technicians work closely with customers to understand their operational requirements and provide customized solutions. The company's facilities, located in Shandong, China, are equipped with state-of-the-art manufacturing and testing equipment, ensuring that every product meets the highest standards of performance and reliability. By choosing HeadPowder, businesses can benefit from years of industry experience and a focus on customer satisfaction, making it the ideal choice for reliable brown sugar powder conveying systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top