With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries dealing with bulk sugar handling, efficient and reliable equipment is crucial. A sugar powder conveyor, also known as a bulk conveyor, is a specialized system designed to transport granular or powdered sugar from one location to another within a processing facility. This equipment is essential for maintaining smooth operations in sugar production, refining, and distribution. The design of such conveyors is tailored to address the unique challenges posed by sugar powder, including its fine particle size, hygroscopic nature, and potential for dust generation.
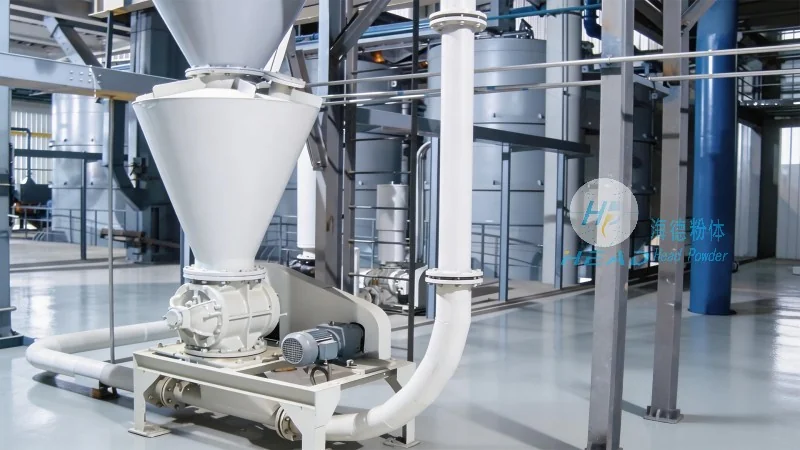
The headpowder sugar powder conveyor system typically consists of several key components that work in tandem to ensure efficient material handling. These components include the hopper, which serves as the storage and feeding unit; the conveyor mechanism, which can be a screw conveyor, belt conveyor, or pneumatic system depending on the application; and the control system, which regulates the flow and speed of the sugar powder. The hopper is designed with a sloped bottom to facilitate the smooth discharge of sugar powder, preventing clogging and ensuring consistent material flow. The conveyor mechanism is engineered to handle the abrasive and fine nature of sugar powder, minimizing wear and tear while maintaining high throughput rates. The control system allows operators to adjust the conveyor speed and feed rate, optimizing the process based on production demands.
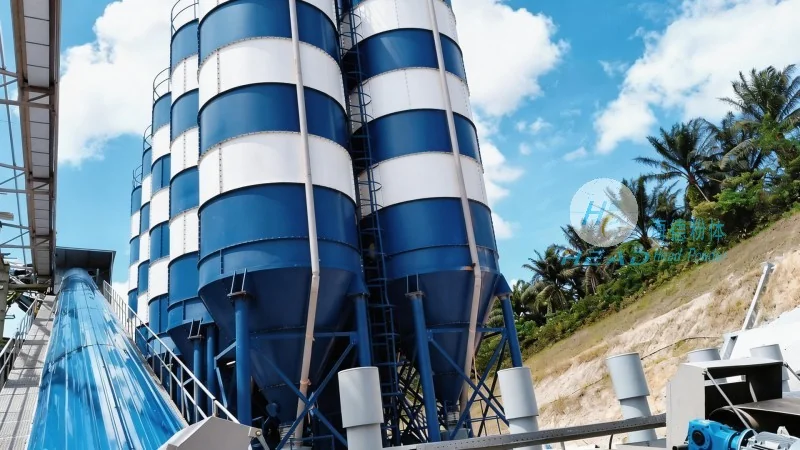
The design principles of a sugar powder conveyor are centered on maximizing efficiency, minimizing material loss, and ensuring safety. One of the primary design considerations is the prevention of sugar powder buildup and caking, which can lead to blockages and reduced conveyor performance. To address this, the conveyor system incorporates features such as anti-static coatings and regular cleaning mechanisms. The material of construction is also critical; components are often made from stainless steel or food-grade materials to prevent contamination and ensure compliance with industry standards. Additionally, the conveyor is designed to minimize air resistance and dust generation, which is essential for maintaining a clean and safe working environment. The design also focuses on energy efficiency, with optimized motor and drive systems that reduce power consumption while maintaining high performance.
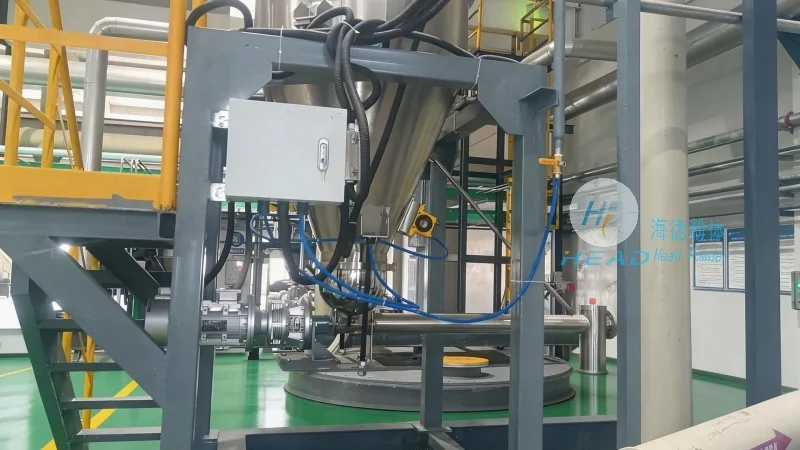
Sugar powder conveyors are widely used in various stages of the sugar production and processing cycle. In the refining process, they are used to transport raw sugar or molasses to the processing units. During the refining stage, the conveyor helps move refined sugar from the crystallization tanks to packaging areas. In the packaging and distribution phase, the conveyor ensures that sugar powder is efficiently transferred from storage silos to packaging machines. The versatility of the sugar powder conveyor makes it suitable for different types of sugar products, including white sugar, brown sugar, and powdered sugar. It can also be integrated into larger processing lines, working in conjunction with other equipment such as mixers, classifiers, and packaging machines to streamline the entire production process.
Choosing a sugar powder conveyor from Shandong HeadPowder Engineering Co., Ltd. offers several advantages for sugar processing facilities. The company specializes in designing and manufacturing high-quality bulk conveying systems tailored to the specific needs of the sugar industry. Their conveyors are engineered to handle the unique properties of sugar powder, ensuring reliable and efficient operation. One of the key advantages is the reduced risk of material loss and contamination, as the conveyor system is designed with tight seals and minimal contact points. This not only improves product quality but also reduces waste and operational costs. Another advantage is the ease of maintenance and cleaning, with components that are easy to access and clean, minimizing downtime and maintenance expenses. The company also provides customized solutions, allowing facilities to adapt the conveyor system to their specific production requirements and space constraints.

In conclusion, a sugar powder conveyor is a critical piece of equipment for any sugar processing facility. Its design and functionality are tailored to address the unique challenges of handling sugar powder, ensuring efficient and safe material transport. The design principles, components, and applications of such conveyors are all focused on maximizing performance and minimizing operational issues. By choosing a high-quality sugar powder conveyor from a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd., sugar processing facilities can enhance their operational efficiency, reduce costs, and maintain product quality. The reliable and efficient operation of a sugar powder conveyor is essential for the smooth functioning of the entire sugar production and distribution process.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top