With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications that require efficient and reliable powder handling, the gray bin powder conveyor is a critical piece of equipment. As a specialized solution from Shandong HeadPowder Engineering Co., Ltd., based in China, this system is designed to address the challenges of transporting bulk materials with precision and consistency. Understanding its design principles is essential for users seeking to optimize their material handling processes.
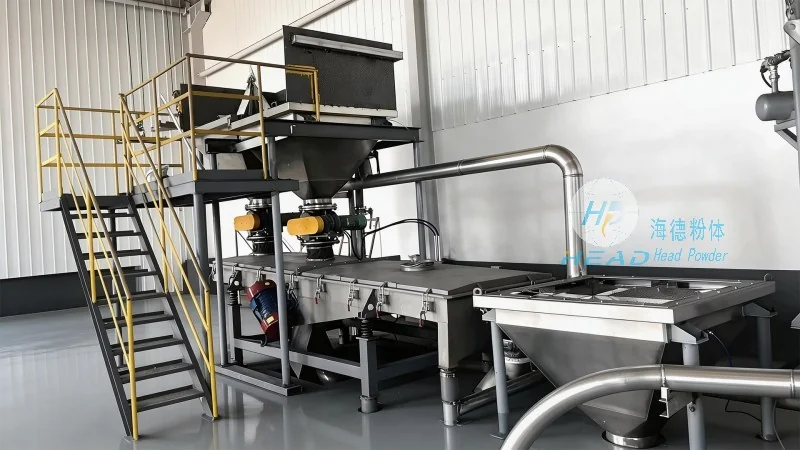
The gray bin powder conveyor, developed by Shandong HeadPowder Engineering Co., Ltd., serves as a robust system for transporting dry powders and granules. This equipment is particularly valuable in industries such as pharmaceuticals, chemicals, food processing, and mining, where the safe and efficient movement of bulk materials is paramount. The design of the gray bin conveyor is tailored to meet the specific demands of these sectors, ensuring minimal product degradation and maximum operational efficiency.
The gray bin powder conveyor consists of several key components that work in harmony to facilitate smooth material transport. At the core is the gray bin, which acts as the storage and feeding unit. This bin is typically made from high-quality materials, such as stainless steel or corrosion-resistant alloys, to ensure durability and resistance to the chemicals or environmental conditions encountered in various industrial settings. The bin is equipped with a feeding mechanism, often a screw or a rotary valve, that regulates the flow of material into the conveyor system.
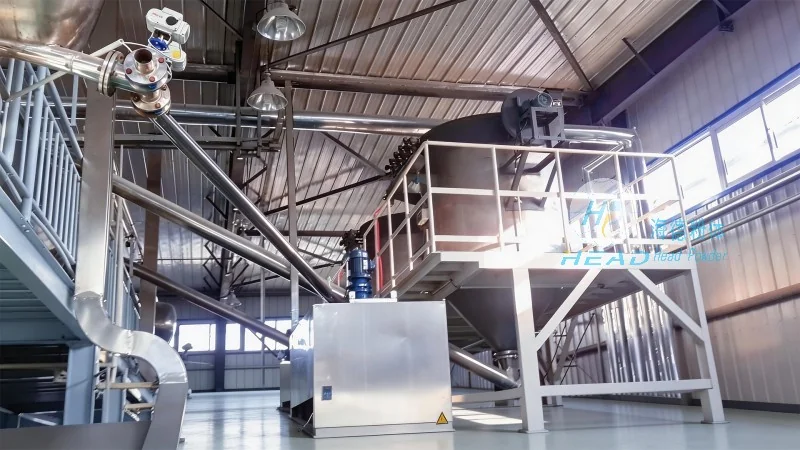
Attached to the gray bin is the conveyor itself, which may include a series of tubes or a flexible hose. The conveyor is designed to handle the vertical and horizontal transport of powders, allowing for flexible installation in different facility layouts. The system may also incorporate a control panel, which enables operators to adjust the speed and flow rate of the conveyor, ensuring precise control over the material handling process.
The design principles of the gray bin powder conveyor are centered on optimizing material flow, minimizing product degradation, and ensuring operational safety. One of the primary principles is the use of a sealed system to prevent dust emissions and contamination. The gray bin and conveyor are typically enclosed, with appropriate sealing mechanisms to maintain a clean and safe working environment. This design also helps to protect the material from moisture and other external factors that could affect its quality.
Another key principle is the optimization of material flow through the use of appropriate angles and slopes. The conveyor system is designed with a slight incline to facilitate the movement of powders from the bin to the discharge point. This design minimizes the risk of material bridging or clogging, which can occur in traditional hoppers. The use of smooth surfaces and rounded corners in the bin and conveyor further reduces the likelihood of material accumulation and improves overall flow characteristics.
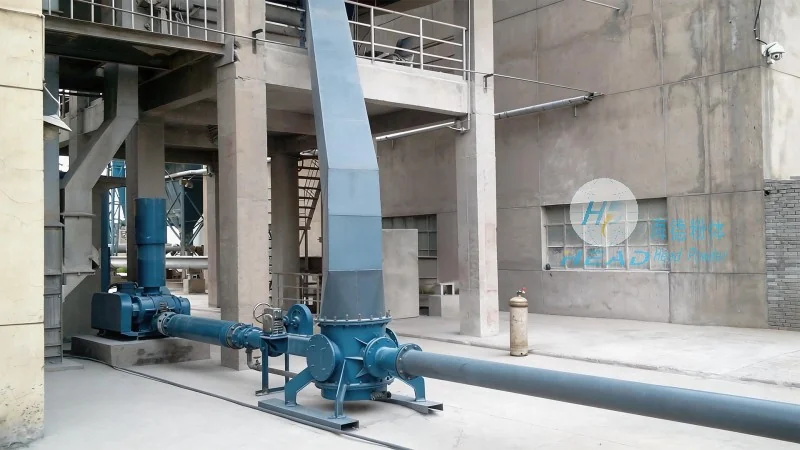
Efficient material handling also relies on the proper selection of components, such as the feeding mechanism and the conveyor type. The screw or rotary valve feeding system is chosen for its ability to control the flow rate accurately, preventing overloading or underloading of the conveyor. The conveyor itself may be a flexible hose or a rigid tube, depending on the application. Flexible hoses are advantageous for applications requiring curved or irregular paths, while rigid tubes offer higher pressure resistance and better flow consistency.
The gray bin powder conveyor offers several operational advantages that make it a preferred choice for many industries. One of the main benefits is its ability to handle a wide range of materials, from fine powders to coarse granules. The system is designed to accommodate different particle sizes and densities, ensuring consistent performance regardless of the material being transported.
Another advantage is the system's low maintenance requirements. The components are engineered for durability and minimal wear, reducing the need for frequent repairs or replacements. The sealed design also minimizes the need for cleaning and maintenance, as it prevents dust from entering the system and contaminating other parts.
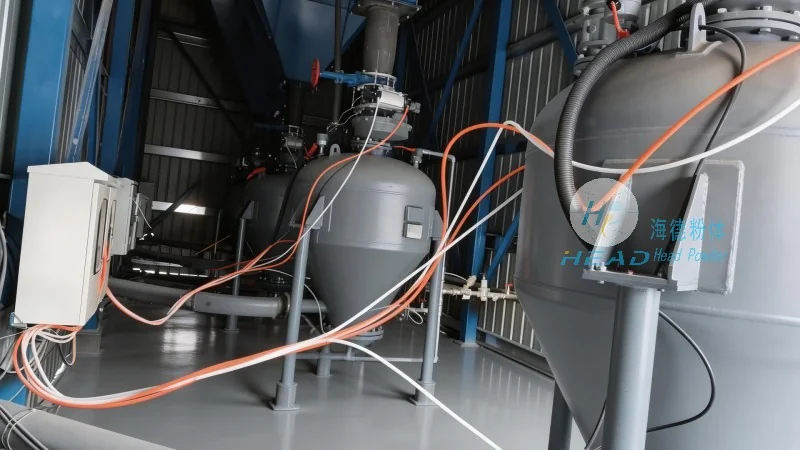
The gray bin powder conveyor is widely used in various applications, including the pharmaceutical industry for transporting active ingredients, the chemical industry for handling raw materials, and the food processing industry for moving ingredients. In mining operations, it is used to transport ore and other bulk materials from storage bins to processing equipment. The versatility of this system makes it suitable for a wide range of industrial needs.
The gray bin powder conveyor, designed by Shandong HeadPowder Engineering Co., Ltd., is a reliable and efficient solution for bulk material handling. Its design principles focus on optimizing flow, ensuring safety, and minimizing product degradation. By incorporating advanced components and a sealed system, this equipment provides users with a robust and durable solution for their material handling needs. Shandong HeadPowder Engineering Co., Ltd., based in China, is committed to delivering high-quality industrial equipment that meets the demands of modern industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top