With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial operations dealing with reclaimed powder, optimizing the conveying process is crucial for maintaining productivity and ensuring a clean working environment. Traditional methods often face challenges such as dust contamination, material loss, and operational inefficiencies. This article explores how pneumatic conveying technology offers a superior solution for enhancing the efficiency of reclaimed powder transport, while maintaining a clean and safe workflow.
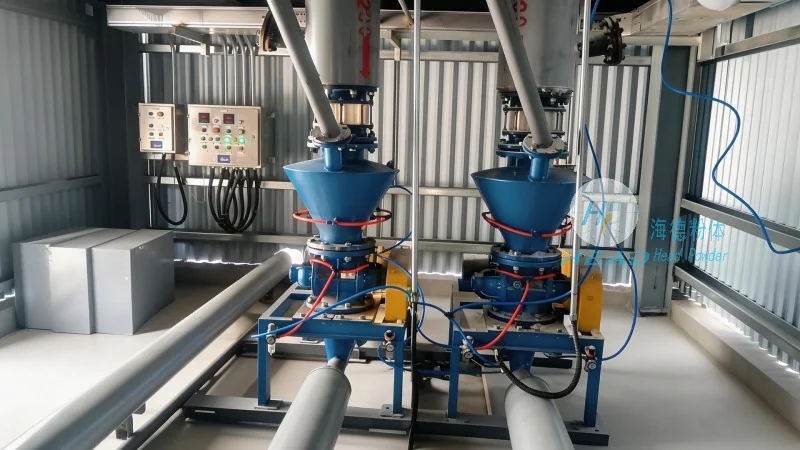
In many industrial sectors, reclaimed powder—such as that from coke or coal processing—plays a vital role in recycling and reducing waste. However, transporting these powders efficiently while minimizing environmental impact and operational costs requires advanced technology. Conventional methods like belt conveyors or screw conveyors can lead to dust emissions, material degradation, and increased maintenance needs. Pneumatic conveying, by contrast, provides a closed system that effectively handles fine powders with minimal contamination, making it an ideal choice for modern industrial applications.
Pneumatic conveying systems utilize air or gas to transport bulk materials through a network of pipes. In the context of reclaimed powder, this technology involves creating a pressure differential to move the powder from the source to the destination. The system typically includes components like a hopper, a feeder, a pipeline, and a receiver. One of the key advantages is the ability to handle fine, abrasive powders without causing degradation or loss. Additionally, the closed system prevents dust from escaping into the environment, aligning with environmental regulations and maintaining a clean workplace. This technology also offers flexibility in system design, allowing for horizontal, vertical, or complex routing configurations to suit various plant layouts.
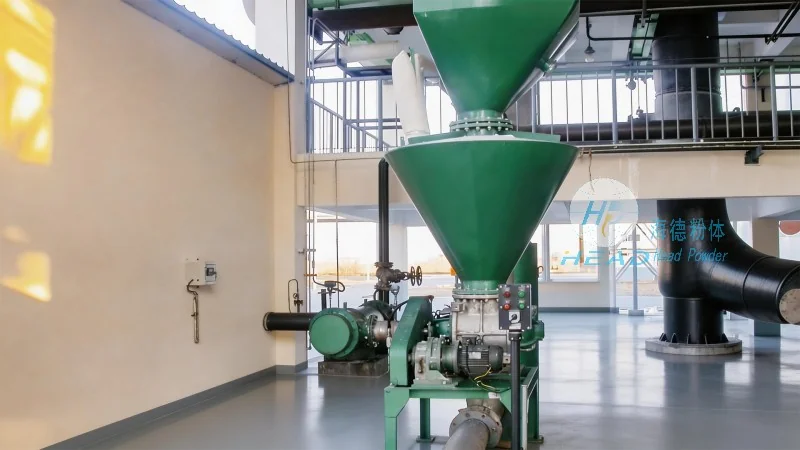
Modern pneumatic conveying systems incorporate advanced features to further improve performance. For instance, variable speed feeders can adjust the material flow rate based on demand, optimizing energy consumption and preventing overloading. The use of high-efficiency filters and dust collectors ensures that any particles that escape the system are captured, maintaining air quality standards. Moreover, the integration of sensors and automation allows for real-time monitoring of system performance, enabling quick adjustments to maintain optimal conveying rates. These advancements not only boost efficiency but also reduce downtime and maintenance costs, making pneumatic conveying a cost-effective solution for long-term operations.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, has successfully implemented pneumatic conveying systems for clients in the coke and coal industries. One notable project involved a client in China who was struggling with inefficient and dusty reclaimed powder transport. By installing a custom-designed pneumatic conveying system, the client achieved significant improvements: the conveying rate increased by 30%, dust emissions were reduced by over 90%, and operational costs decreased by approximately 20%. The system was tailored to the client's specific needs, including the handling of fine, abrasive powders and the integration with existing plant infrastructure. This success story highlights the effectiveness of pneumatic conveying in addressing the unique challenges of reclaimed powder handling.
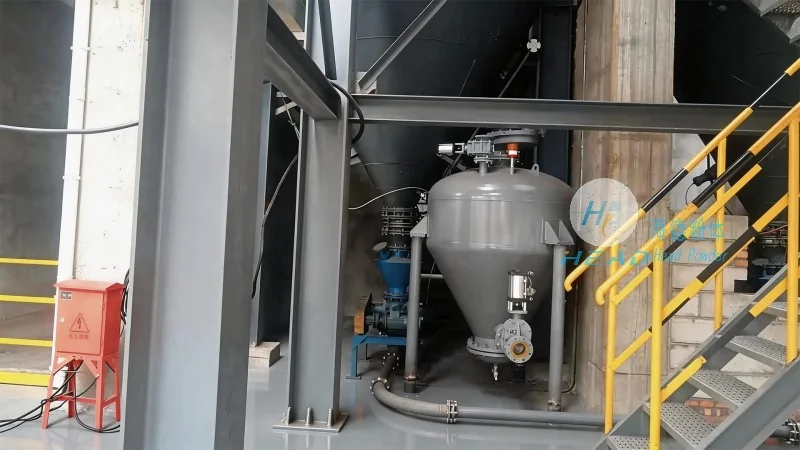
When selecting a pneumatic conveying system for reclaimed powder applications, several factors should be considered. The first is the material characteristics, such as particle size, density, and moisture content, as these affect the system's design and performance. The second is the system layout, including the distance and routing required, which determines the type of conveying (e.g., pressure or vacuum). The third is the environmental and safety requirements, which may dictate the need for a closed system and dust control measures. Consulting with a specialized engineering company, like Shandong HeadPowder Engineering Co., Ltd., ensures that the system is designed to meet all these requirements and is optimized for the specific application. The company's expertise in bulk material handling, combined with its understanding of industrial processes, enables them to provide tailored solutions that enhance efficiency and sustainability.
Pneumatic conveying technology represents a significant advancement in the handling of reclaimed powder, offering a clean, efficient, and sustainable solution for industrial operations. By leveraging advanced systems and expert engineering, companies can improve their conveying processes, reduce environmental impact, and enhance overall productivity. As industries continue to prioritize efficiency and sustainability, pneumatic conveying is poised to remain a key technology in the bulk material handling sector. For businesses seeking to optimize their reclaimed powder transport, partnering with a reputable engineering firm like Shandong HeadPowder Engineering Co., Ltd. can provide the expertise and solutions needed to achieve their operational goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top