With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For agricultural and food processing industries, efficient and reliable transport of corn kernels is crucial for maintaining product quality and operational efficiency. Pneumatic conveying technology has emerged as a sophisticated solution for handling corn kernels, offering advantages such as reduced contamination, minimal product degradation, and enhanced safety compared to traditional methods like belt conveyors or bucket elevators. This article explores the application and optimization of pneumatic conveying systems specifically tailored for corn kernel transport, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field.
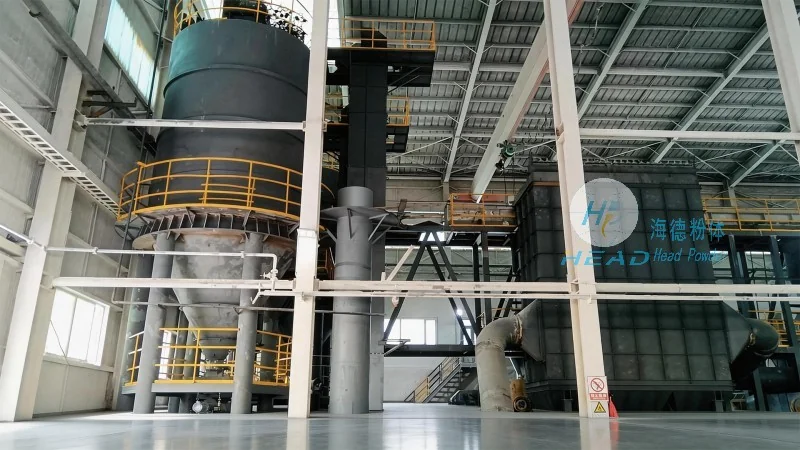
HeadPowder, a division of Shandong HeadPowder Engineering Co., Ltd., specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. With headquarters in Shandong, China, the company leverages decades of experience in bulk material handling to deliver customized solutions for agricultural products, including corn kernels. The company’s commitment to innovation and customer-centric approach ensures that each project is tailored to meet the unique requirements of the client, whether it involves high-volume processing, complex system integration, or adherence to stringent industry standards.
Pneumatic conveying systems utilize air pressure to transport corn kernels through a network of pipes, eliminating the need for mechanical components that can cause friction and damage to the kernels. The technology can be categorized into two main types: dilute-phase and dense-phase conveying. Dilute-phase systems, which operate at higher air velocities, are ideal for short-distance transport and low to medium particle sizes, while dense-phase systems, operating at lower velocities, are better suited for longer distances and higher particle loads, ensuring gentle handling and minimal product degradation. For corn kernel transport, a combination of these systems may be employed to optimize both efficiency and product integrity.
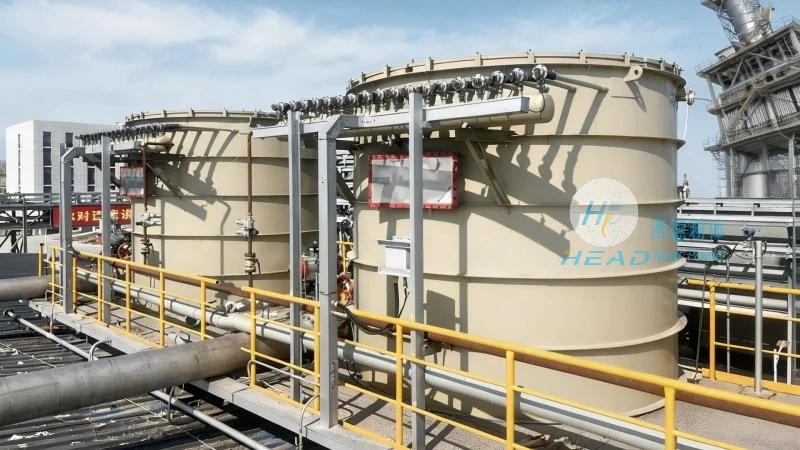
Optimized pneumatic conveying systems offer several key advantages for corn kernel handling. Firstly, they provide a hygienic and dust-free environment, which is critical for maintaining the quality and safety of food products. Unlike mechanical conveyors, pneumatic systems do not come into direct contact with the product, reducing the risk of contamination from metal parts or other materials. Secondly, these systems are highly flexible, allowing for easy integration with existing processing lines and the ability to transport corn kernels to multiple destinations from a single source. Thirdly, pneumatic conveying can significantly reduce energy consumption compared to traditional methods, as the air pressure required is often lower than the mechanical force needed for belt or bucket elevators. Additionally, the systems are capable of handling varying particle sizes and moisture content, making them adaptable to different stages of corn processing, from raw kernel collection to final product packaging.
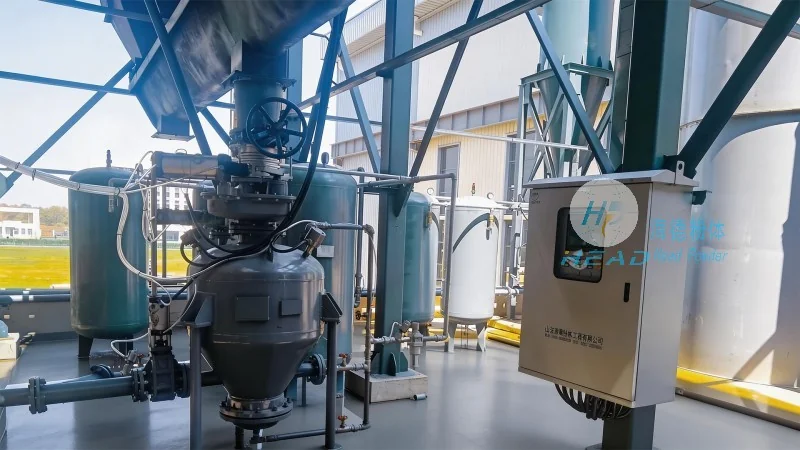
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented pneumatic conveying solutions for numerous corn processing facilities across China. For instance, one client, a large-scale corn milling operation, required a system to transport 500 tons of corn kernels per hour from storage silos to the milling department. The company designed a dense-phase pneumatic conveying system with a custom-built airlock and control panel, ensuring smooth and continuous operation. The system reduced downtime by 30% and improved product quality by minimizing kernel breakage. Another case involved a corn wet-milling plant, where the company integrated a dilute-phase system to transport corn kernels from the cleaning stage to the grinding section. The system’s adjustable air velocity and pressure control allowed for precise handling, resulting in a 20% increase in overall processing efficiency.
In conclusion, the application and optimization of pneumatic conveying technology in corn kernel transport represent a significant advancement in bulk material handling. By leveraging the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., agricultural and food processing industries can achieve enhanced efficiency, product quality, and operational safety. As technology continues to evolve, future developments may include the integration of smart sensors and automation to further optimize system performance, ensuring that pneumatic conveying remains a leading solution for corn kernel transport in the coming years.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top