With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the efficient and reliable transport of sodium hexafluorophosphate (NaPF₆) is crucial for industries that rely on this chemical compound. The design and implementation of specialized transport systems are essential to ensure safe, cost-effective, and environmentally friendly handling of this material. This article provides an overview of sodium hexafluorophosphate transport systems, with a focus on the benefits of pneumatic conveying technology.
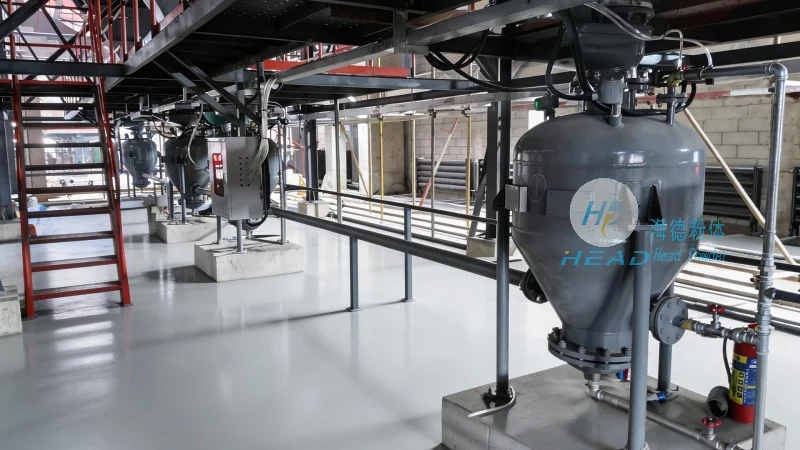
Sodium hexafluorophosphate is a white crystalline powder commonly used in various industrial applications, including the production of pharmaceuticals, electronics, and specialty chemicals. The transport of this material requires careful consideration of its physical properties, such as its hygroscopic nature and potential reactivity with certain materials. Traditional methods like belt conveyors or bucket elevators may not be suitable due to the risk of dust generation and material degradation. Therefore, specialized transport systems are developed to address these challenges.
HeadPowder, a leading provider in the field, offers comprehensive solutions tailored to the unique requirements of sodium hexafluorophosphate handling. The company, based in Shandong, China, leverages advanced engineering and material science expertise to design and manufacture transport systems that meet industry standards and client specifications. The transport systems are engineered to ensure minimal product loss, low maintenance costs, and high operational efficiency.
Pneumatic conveying, also known as air conveying, is a method that uses compressed air to transport bulk materials through a pipeline system. This technology offers several advantages over traditional mechanical conveying methods, particularly for handling sodium hexafluorophosphate. One of the key benefits is the ability to transport the material in a closed system, which significantly reduces dust emissions and improves workplace safety. This is critical for maintaining compliance with environmental regulations and protecting the health of personnel.
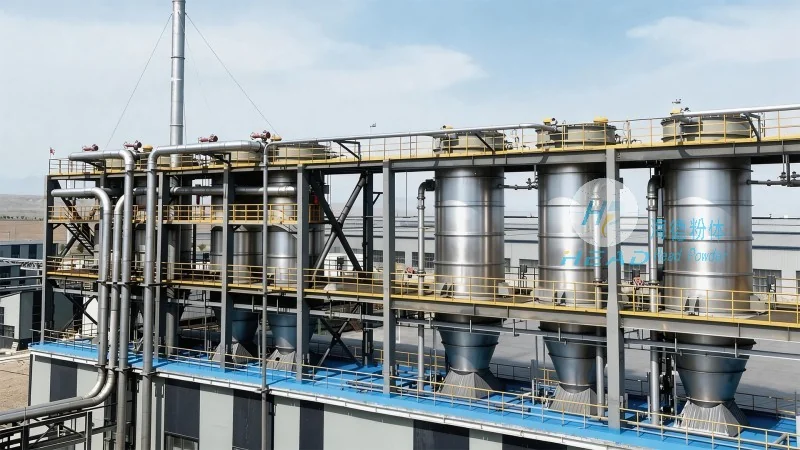
Another advantage is the flexibility of pneumatic conveying systems. They can be easily integrated into existing production lines and adapted to different plant layouts. The system can handle varying material flow rates and can transport materials over long distances without the need for multiple transfer points. This reduces the complexity of the overall transport infrastructure and lowers operational costs.
Furthermore, pneumatic conveying systems provide better control over the material's temperature and moisture content. By maintaining a controlled environment within the pipeline, the material's quality is preserved, preventing issues such as caking or degradation that can occur with other transport methods. This is particularly important for sodium hexafluorophosphate, which is sensitive to moisture and temperature fluctuations.
The transport system for sodium hexafluorophosphate typically includes several components that work together to ensure efficient and safe operation. These components include a hopper for material storage, a feeder to control the flow rate, a conveying pipeline, and a receiver for the material's final destination. The system may also incorporate dust collection and filtration equipment to ensure that any particles released during the process are captured and contained.
HeadPowder's transport systems are designed with durability and reliability in mind. The materials used in the construction of the pipeline and components are selected to resist corrosion and wear, ensuring a long service life. The system is equipped with advanced control systems that allow for real-time monitoring of flow rates, pressure, and other critical parameters. This enables operators to quickly identify and address any issues that may arise, minimizing downtime and maximizing productivity.
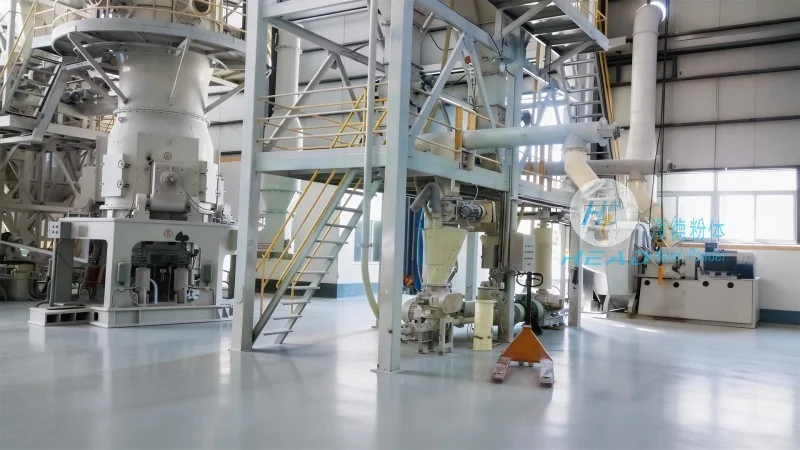
The effectiveness of sodium hexafluorophosphate transport systems, particularly those utilizing pneumatic conveying, has been demonstrated in various industrial settings. For example, in pharmaceutical manufacturing, the need for clean and dust-free environments is paramount. The closed-loop pneumatic conveying system from HeadPowder has been successfully implemented in such facilities, ensuring that the material is transported without contamination and maintaining compliance with stringent quality standards.
In the electronics industry, where sodium hexafluorophosphate is used as a precursor for certain semiconductor materials, the precision and reliability of the transport system are critical. The system's ability to maintain consistent flow rates and prevent material degradation has contributed to improved product quality and reduced waste. These success stories highlight the importance of choosing the right transport technology for specific applications.
In conclusion, the development of specialized transport systems for sodium hexafluorophosphate, particularly those utilizing pneumatic conveying, has revolutionized the way this material is handled in industrial settings. The advantages of closed-system transport, reduced dust emissions, and improved material quality control make these systems a preferred choice for many industries. As technology continues to advance, we can expect further innovations in transport systems that will enhance efficiency, safety, and sustainability in the handling of sodium hexafluorophosphate.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top