With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications involving the handling of crystalline materials, efficient and reliable conveying systems are essential to ensure smooth operations and maintain product quality. Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in the design and implementation of advanced crystal particle conveying systems. This article provides an overview of such systems, highlighting their key advantages and features, particularly focusing on the benefits of pneumatic conveying for crystal particles.
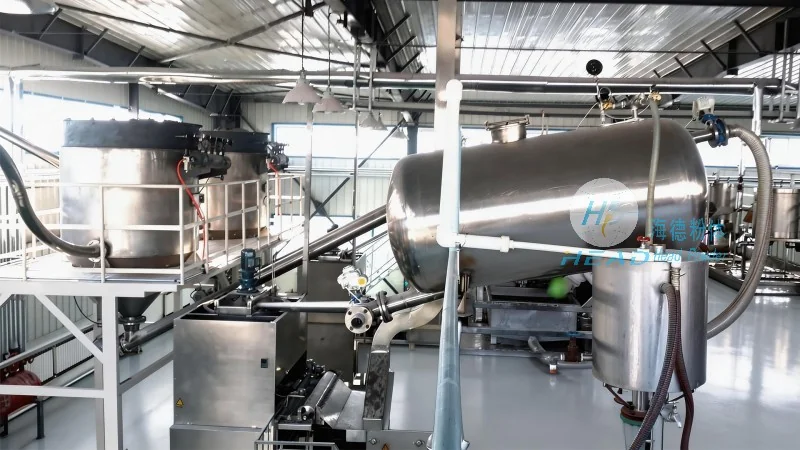
Crystal particle conveying systems are engineered to transport crystalline materials, such as sugar, salt, or pharmaceutical powders, from one location to another within an industrial facility. These systems are designed to handle materials that are often sensitive to moisture, temperature, or contamination, making the choice of conveying method critical for maintaining product integrity. The primary goal of these systems is to ensure that the material is moved efficiently, safely, and without degradation, while minimizing downtime and operational costs.
Pneumatic conveying, also known as air-based conveying, is a widely adopted method for transporting crystal particles due to its versatility and effectiveness. Unlike mechanical systems that rely on belts or screws, pneumatic systems use pressurized air to move materials through a pipeline. This approach offers several advantages, including the ability to handle materials with varying particle sizes and shapes, as well as the capacity to transport materials over long distances without the need for multiple transfer points.
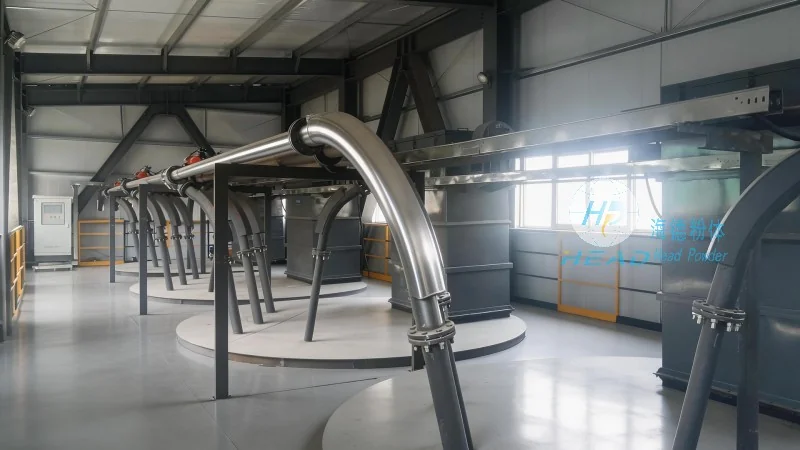
One of the most significant advantages of pneumatic conveying for crystal particles is its ability to maintain product purity and quality. Since the material is enclosed within a sealed pipeline, it is protected from external contaminants, such as dust, moisture, or air pollutants. This is particularly important for pharmaceutical or food-grade crystalline materials, where even minor contamination can have severe consequences. Additionally, pneumatic systems can be designed to operate at low temperatures, preventing thermal degradation of heat-sensitive crystals.
Another key benefit is the flexibility of pneumatic conveying systems. They can be easily integrated into existing industrial setups, allowing for modifications or expansions without major structural changes. The systems can handle both bulk and small quantities of crystal particles, making them suitable for a wide range of applications, from large-scale production lines to laboratory-scale experiments. Furthermore, pneumatic conveying reduces the risk of product degradation due to friction or impact, as the material is gently moved through the pipeline by air currents.
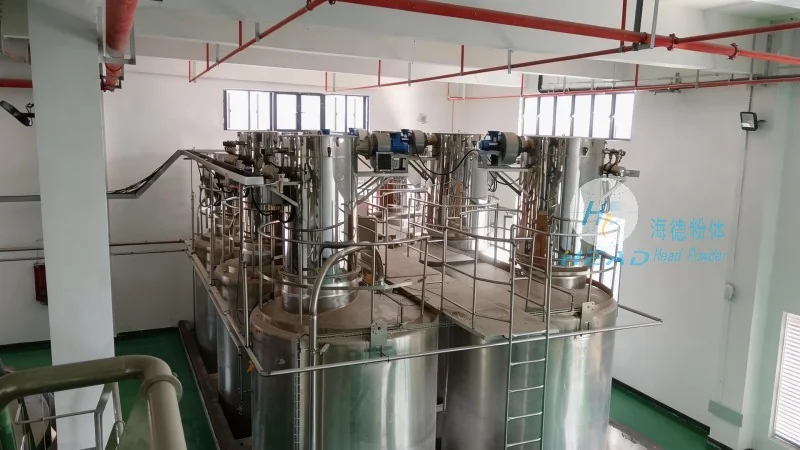
Modern crystal particle conveying systems, particularly those offered by Shandong HeadPowder Engineering Co., Ltd., incorporate several advanced features that enhance performance and reliability. These systems often include automated control mechanisms that monitor and adjust air pressure, flow rate, and material feed, ensuring consistent and efficient operation. The use of high-quality materials, such as stainless steel or corrosion-resistant alloys, ensures durability and longevity, even in harsh industrial environments. Additionally, advanced systems may incorporate dust collection and filtration systems to maintain air quality and comply with environmental regulations.
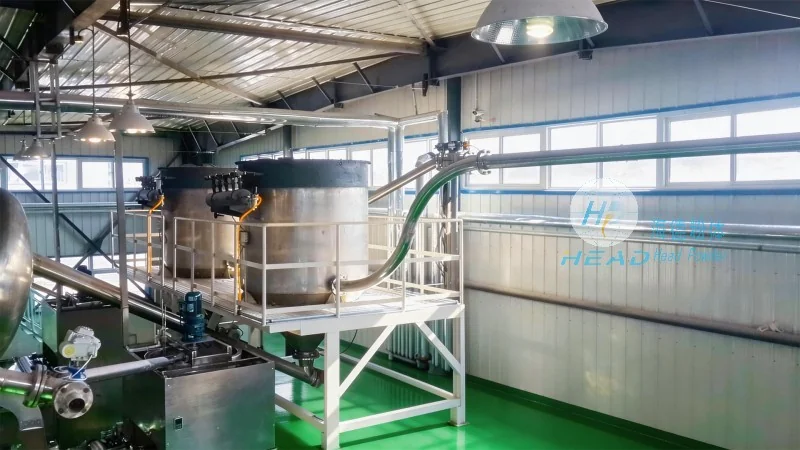
Furthermore, the design of these systems allows for easy maintenance and cleaning, reducing downtime and operational costs. The modular construction of the systems enables quick replacement of components, minimizing the impact of maintenance activities on production schedules. This flexibility in maintenance is particularly valuable for facilities that require continuous operation to meet production targets.
In conclusion, crystal particle conveying systems, especially those utilizing pneumatic conveying, offer significant advantages for industrial applications. The ability to maintain product quality, handle diverse materials, and operate efficiently makes these systems a preferred choice for many industries. By leveraging advanced technology and engineering expertise, companies like Shandong HeadPowder Engineering Co., Ltd. provide tailored solutions that meet the specific needs of their clients. Whether for food processing, pharmaceutical manufacturing, or chemical production, the benefits of crystal particle pneumatic conveying systems are evident in improved operational efficiency, reduced costs, and enhanced product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top