With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and installation of advanced pneumatic conveying systems tailored for the powdered milk industry. This article provides a comprehensive overview of these systems, highlighting their functionality, benefits, and practical applications.
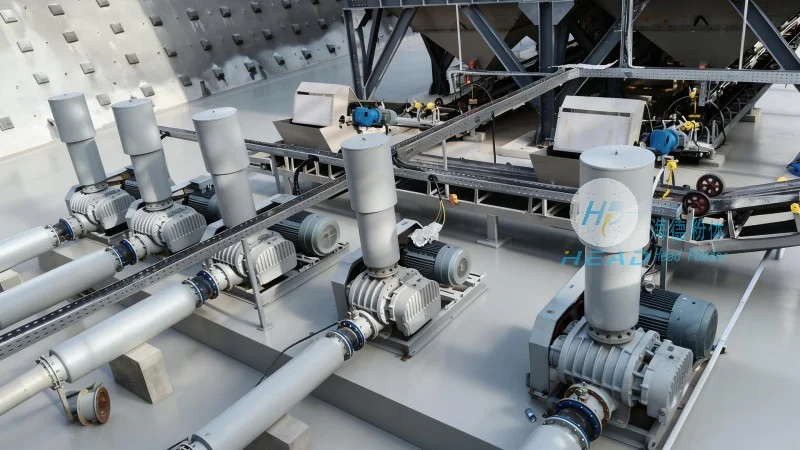
Pneumatic conveying systems are essential for efficiently transporting powdered milk from storage silos, processing units, or packaging lines. These systems utilize air or gas as the primary medium to move bulk materials, offering a clean, low-maintenance, and cost-effective solution compared to traditional mechanical conveying methods. The systems are engineered to handle the delicate nature of powdered milk, ensuring minimal product degradation and maintaining product integrity throughout the conveying process.
The operation of a typical pneumatic conveying system for powdered milk involves several key components and processes. At its core, the system consists of a hopper or storage container where the powdered milk is stored. An air compressor generates the necessary pressure or vacuum to move the material. The system may employ either positive pressure (where air is forced into the system) or negative pressure (where air is drawn out) to transport the powder. The choice between these methods depends on factors such as the distance to be covered, the volume of material, and the specific characteristics of the powdered milk being handled.
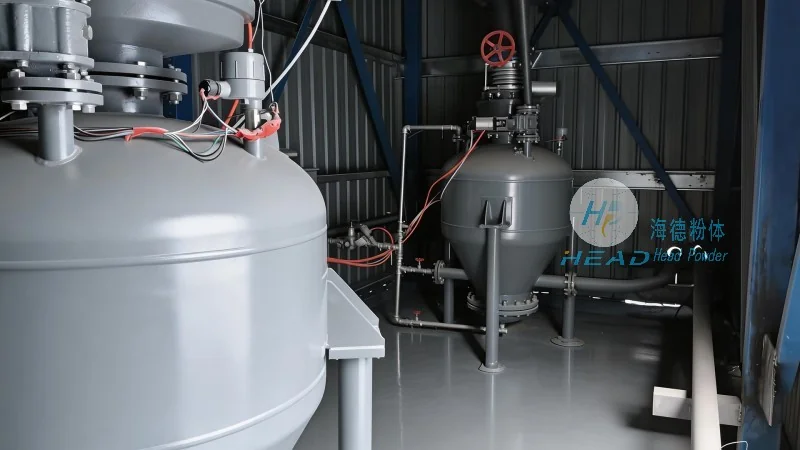
Several critical components work in tandem to ensure the smooth operation of a pneumatic conveying system for powdered milk. These include:
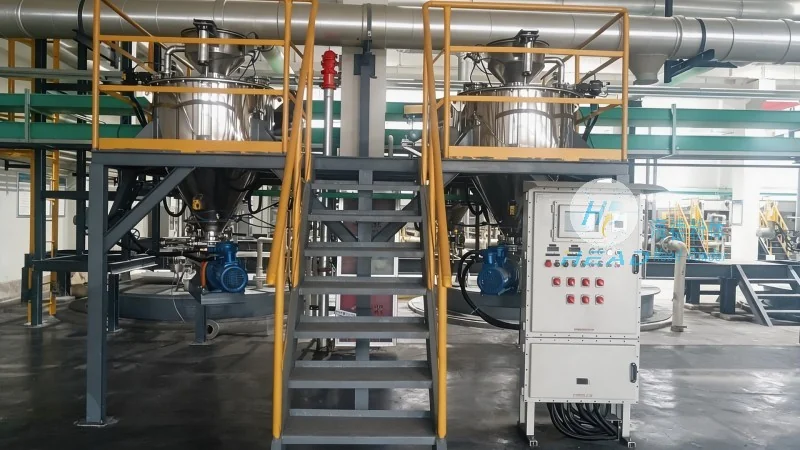
Implementing a pneumatic conveying system for powdered milk offers numerous advantages over traditional methods. These include:
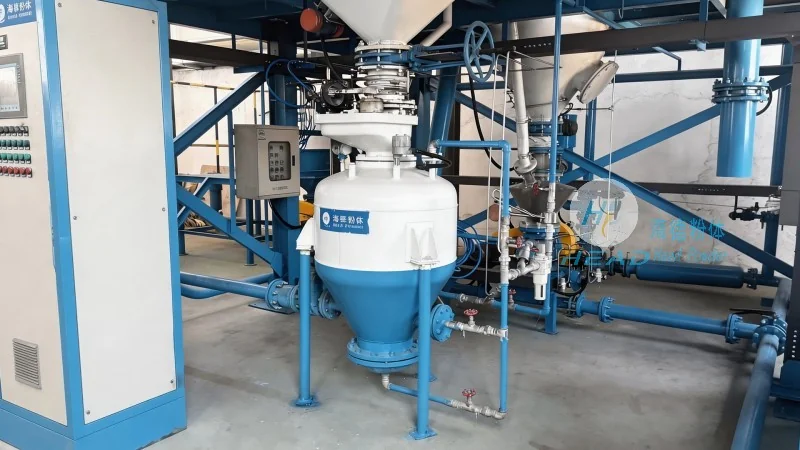
Pneumatic conveying systems are widely used in various stages of the powdered milk production and distribution process. Common applications include:
HeadPowder Engineering Co., Ltd., based in Shandong, China, offers expertly designed pneumatic conveying systems that address the unique challenges of handling powdered milk. By leveraging advanced technology and a deep understanding of the industry, these systems provide reliable, efficient, and hygienic solutions for businesses in the dairy and food processing sectors. Whether for new installations or system upgrades, HeadPowder's pneumatic conveying solutions are tailored to meet the specific needs of each client, ensuring optimal performance and long-term value.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top