With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Organic fertilizer granule pneumatic conveying systems are critical in modern agricultural and industrial applications, designed to efficiently transport granular organic fertilizers with precision and reliability. This article provides an overview of such systems, focusing on their structural components and operational principles, while highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. as a leading manufacturer in this field.
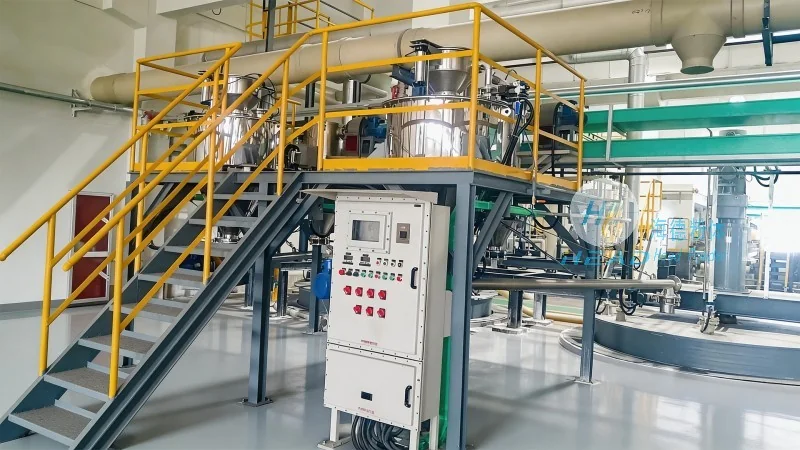
Organic fertilizer granule pneumatic conveying systems are engineered to handle the transportation of granular organic fertilizers from storage or production areas to processing units, storage silos, or application sites. These systems utilize air as the primary medium to move materials, offering advantages such as reduced labor costs, minimized material handling risks, and improved process efficiency compared to traditional mechanical conveyors. The systems are particularly suitable for handling bulk organic fertilizers, which are often dusty and require gentle handling to preserve their quality and nutritional value.
The organic fertilizer granule pneumatic conveying system typically consists of several core components that work in concert to ensure smooth material transport. These components include the hopper or feeder, which holds the granular organic fertilizer and regulates the flow rate; the air compressor or blower, which generates the necessary air pressure to move the material; the conveying line, which can be either a flexible hose or a rigid pipe, depending on the system design; and the receiver or silo, where the fertilizer is deposited after transport. Additionally, the system may incorporate control valves, filters, and dust collection units to maintain air quality and system performance.
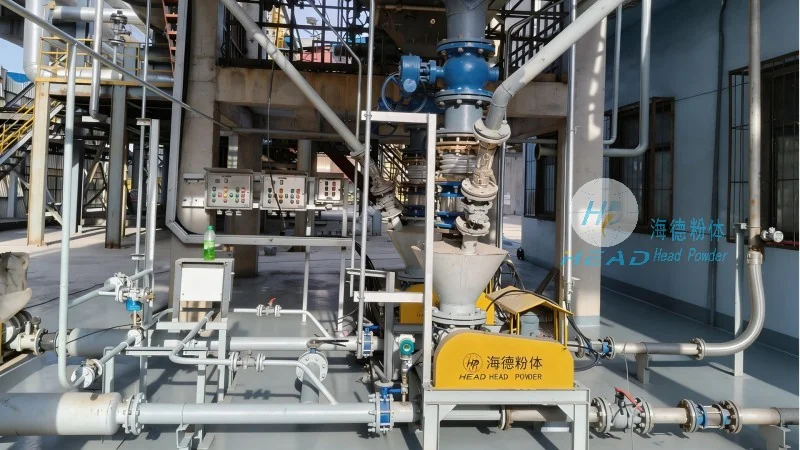
The operational principle of the organic fertilizer granule pneumatic conveying system is based on the creation of a pressure differential between the inlet and outlet of the conveying line. The air compressor or blower supplies compressed air into the conveying line, which then entrains the granular fertilizer particles and propels them through the system. The air velocity within the line is carefully controlled to ensure that the fertilizer particles are suspended and transported without causing excessive wear or degradation. The system may operate in either positive pressure (where the conveying line is under pressure) or negative pressure (where the line is under vacuum) modes, depending on the specific application requirements and the distance over which the material needs to be transported.
Implementing a pneumatic conveying system for organic fertilizer granules offers several key advantages. Firstly, it provides a dust-free and hygienic method of material handling, which is crucial for maintaining the quality of organic fertilizers and ensuring compliance with environmental regulations. Secondly, the system allows for precise control over the flow rate and pressure, enabling consistent and reliable transport of the fertilizer. Thirdly, pneumatic conveyors can handle a wide range of particle sizes and moisture contents, making them versatile for various organic fertilizer formulations. Finally, the system reduces the need for manual labor and minimizes the risk of material spillage or contamination, contributing to overall operational efficiency and cost savings.
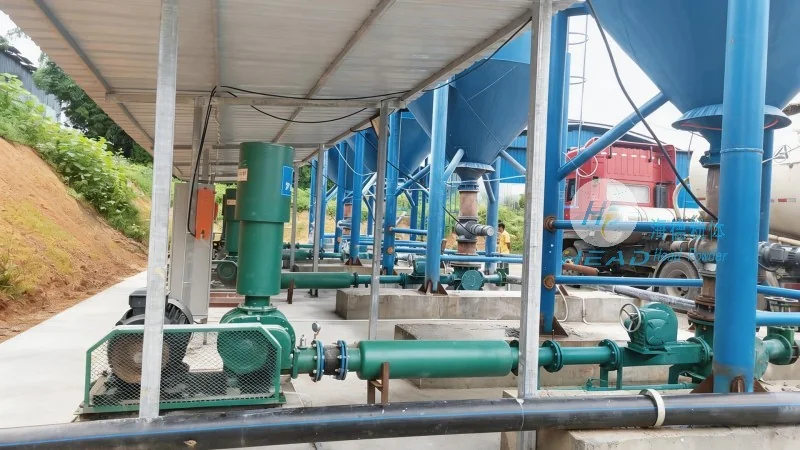
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized organic fertilizer granule pneumatic conveying systems tailored to the specific needs of clients. The company's engineers work closely with customers to assess their operational requirements, including the type and quantity of fertilizer, the distance of transport, and the existing infrastructure. Based on this assessment, they design systems that integrate seamlessly with existing production lines or storage facilities, ensuring minimal disruption to current operations. The company also provides after-sales support, including maintenance services and technical assistance, to ensure the long-term reliability and performance of the conveying systems.
Organic fertilizer granule pneumatic conveying systems are essential for efficient and reliable transport of granular organic fertilizers in agricultural and industrial settings. With its comprehensive understanding of material handling and engineering expertise, Shandong HeadPowder Engineering Co., Ltd. offers high-quality, customized solutions that meet the diverse needs of the fertilizer industry. By leveraging advanced technology and rigorous quality control, the company ensures that its pneumatic conveying systems deliver optimal performance, durability, and cost-effectiveness, helping clients enhance their operational efficiency and maintain the quality of their organic fertilizers.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top