With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
The corn cob material conveying system is a specialized equipment designed for the efficient handling and transportation of corn cobs. As a key component in agricultural processing and material handling, this system plays a crucial role in optimizing production workflows. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, the system integrates advanced engineering principles to ensure reliable and efficient operation.
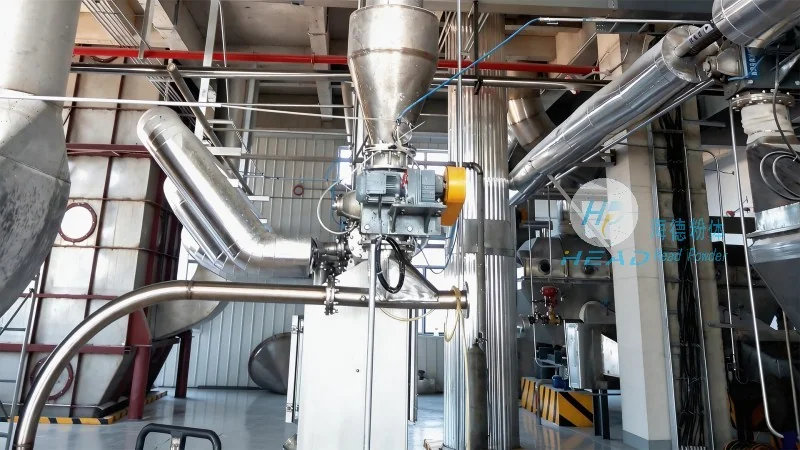
The corn cob material conveying system typically consists of several core components that work in harmony to achieve seamless material transport. The primary elements include a feeding mechanism, a conveyor belt or screw conveyor, a control system, and a discharge unit. The feeding mechanism is responsible for collecting and feeding the corn cobs into the system, ensuring a consistent flow of material. The conveyor belt or screw conveyor then transports the corn cobs through the system, utilizing mechanical power to move the material from the intake to the discharge point. The control system monitors and regulates the operation of the components, maintaining optimal performance and preventing operational issues. The discharge unit collects the transported corn cobs and prepares them for subsequent processing or storage.
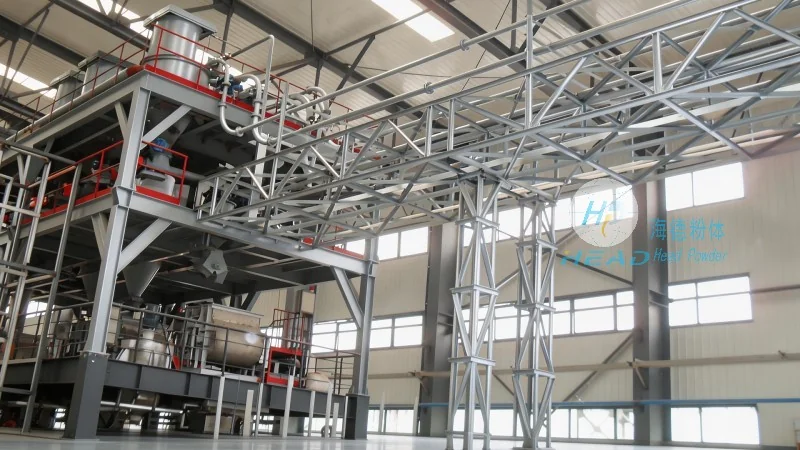
The operation of the corn cob material conveying system follows a systematic process that ensures efficient material handling. Initially, the corn cobs are fed into the system through the feeding mechanism, which may involve a hopper or a manual loading area. The feeding mechanism ensures that the corn cobs are evenly distributed and fed into the conveyor system. Once inside the conveyor, the corn cobs are transported along the path defined by the conveyor belt or screw mechanism. The speed and direction of the conveyor are controlled by the system's control unit, which adjusts based on the material flow and operational requirements. As the corn cobs move through the system, they are guided by the conveyor's structure, preventing jamming or blockages. The discharge unit then collects the corn cobs at the end of the conveyor, where they are either transferred to a storage bin or sent to the next processing stage. Throughout the operation, the control system continuously monitors key parameters such as speed, pressure, and material level, ensuring that the system operates within safe and efficient parameters.
The working principle of the corn cob material conveying system is based on mechanical energy conversion and material flow dynamics. The system utilizes a combination of gravity and mechanical force to move the corn cobs from the intake to the discharge point. The feeding mechanism provides the initial force to push the corn cobs into the conveyor, while the conveyor's mechanical components (such as the belt or screw) generate the necessary force to transport the material. The control system plays a critical role in regulating the operation, ensuring that the conveyor speed matches the material flow rate. This dynamic balance between input force and output transport ensures that the system operates efficiently without excessive energy consumption. Additionally, the system's design incorporates features to handle the unique characteristics of corn cobs, such as their irregular shape and varying size, which may affect material flow. The conveyor's structure, including the angle of inclination and the surface texture, is optimized to minimize friction and ensure smooth movement of the corn cobs. The discharge unit is designed to handle the collected corn cobs without causing damage or loss, maintaining the integrity of the material for subsequent processing.
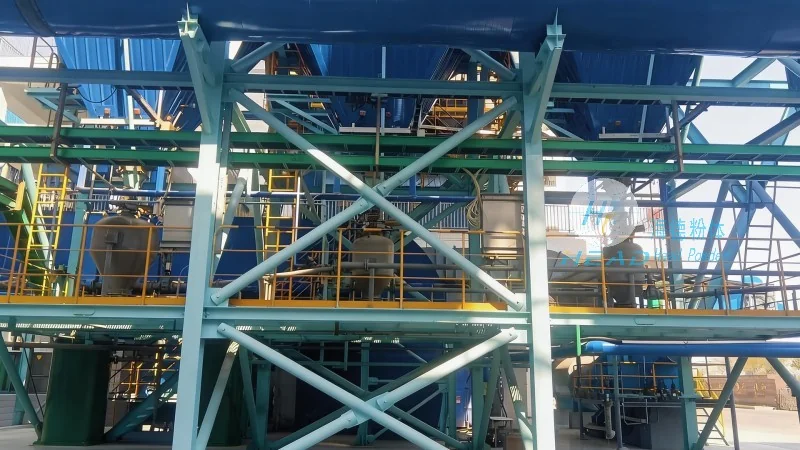
The corn cob material conveying system offers several advantages that make it a preferred choice for agricultural and industrial applications. Its efficient design minimizes material handling time and labor costs, while ensuring high throughput rates. The system's reliability and durability reduce downtime and maintenance expenses, contributing to overall operational efficiency. Additionally, the system's modular design allows for easy integration into existing production lines, making it adaptable to various processing requirements. The system is widely used in corn processing facilities, where it is employed to transport corn cobs from the harvesting stage to the subsequent processing steps, such as drying, grinding, or pelletizing. In industrial settings, the system can be used to transport corn cobs for biofuel production, animal feed manufacturing, or other applications that require consistent material handling. The system's ability to handle large volumes of corn cobs with minimal human intervention makes it an essential component in modern agricultural processing operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top