With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For construction and industrial applications, efficient stone material handling is crucial for maintaining productivity and safety on site. The stone material conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., offers a reliable solution to transport various types of aggregates, crushed stones, and other bulk materials with precision and efficiency. This system is designed to meet the demands of modern construction projects, ensuring smooth material flow from extraction to processing stages.
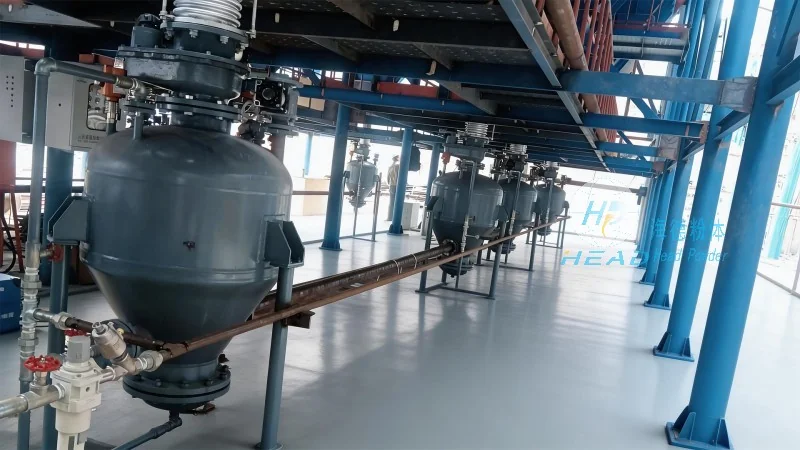
The stone material conveying system comprises several critical components that work in harmony to ensure optimal performance. The primary components include the conveyor belt, drive system, idlers, and supporting structures. The conveyor belt, typically made from durable rubber or synthetic materials, is responsible for carrying the stone materials over long distances. The drive system, which may consist of electric motors and gearboxes, provides the necessary power to move the belt at a consistent speed. Idlers are strategically placed along the conveyor to support the belt and maintain its tension, preventing sagging and ensuring smooth operation. The supporting structures, such as frames and brackets, provide stability and durability to the entire system, allowing it to withstand heavy loads and harsh environmental conditions.
The operation of the stone material conveying system follows a systematic process that begins with material loading at the inlet. At the loading point, stone materials are fed into the system, either manually or through automated feeding mechanisms. The materials then travel along the conveyor belt, moving from the inlet to the discharge point. The speed of the conveyor belt is controlled by the drive system, which can be adjusted based on the material type and processing requirements. As the materials move, they are transported to the next stage of processing, such as crushing or sorting. The system is equipped with sensors and control panels that monitor the operation in real-time, allowing operators to adjust parameters as needed to maintain efficiency. The discharge point is designed to release the materials safely and efficiently, ensuring that the system can handle high volumes of stone materials without interruption.
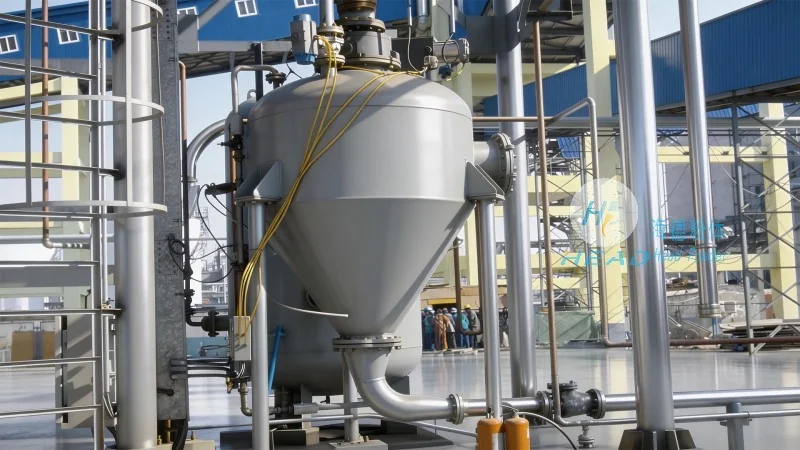
The working principle of the stone material conveying system is based on the frictional force between the conveyor belt and the materials being transported. The drive system rotates the pulleys, which in turn move the conveyor belt. As the belt moves, the materials placed on it are carried along due to the frictional force. This mechanism allows for continuous and unidirectional movement of the stone materials, eliminating the need for manual handling and reducing labor costs. The system is designed to handle a wide range of material sizes and weights, from small gravel to large crushed stones, making it versatile for various industrial applications. The belt's tension and speed are carefully managed to prevent material spillage and ensure that the system operates within safe limits. Additionally, the system incorporates safety features, such as emergency stop buttons and overload protection, to protect both the equipment and the operators from potential hazards.
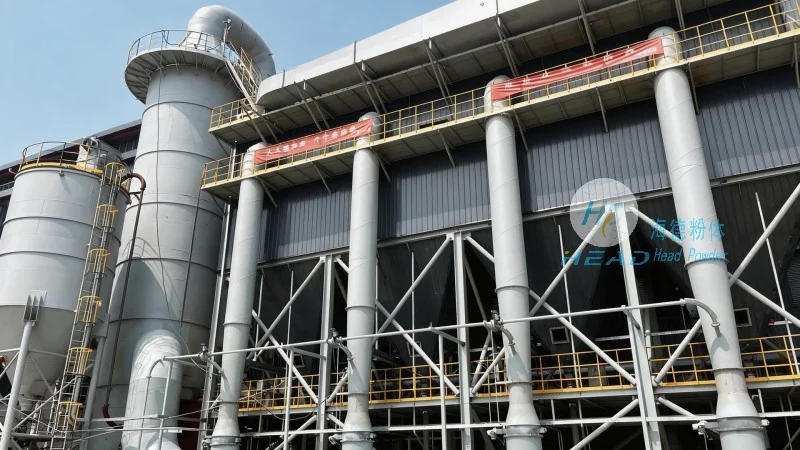
Implementing the stone material conveying system offers several advantages for construction and industrial operations. Firstly, it significantly improves material handling efficiency by automating the transportation process, reducing the time and labor required for manual material movement. This leads to increased productivity and faster project completion times. Secondly, the system minimizes material loss and spillage, as the enclosed design prevents materials from falling off the belt during transport. This not only reduces waste but also improves workplace safety by eliminating the risk of material-related accidents. Thirdly, the system is highly durable and low-maintenance, with components designed to withstand heavy loads and harsh conditions. The use of high-quality materials and robust construction ensures a long service life, reducing the need for frequent repairs and replacements. Furthermore, the system can be customized to meet specific project requirements, such as varying conveyor lengths, widths, and speeds, making it adaptable to different site conditions and material handling needs.
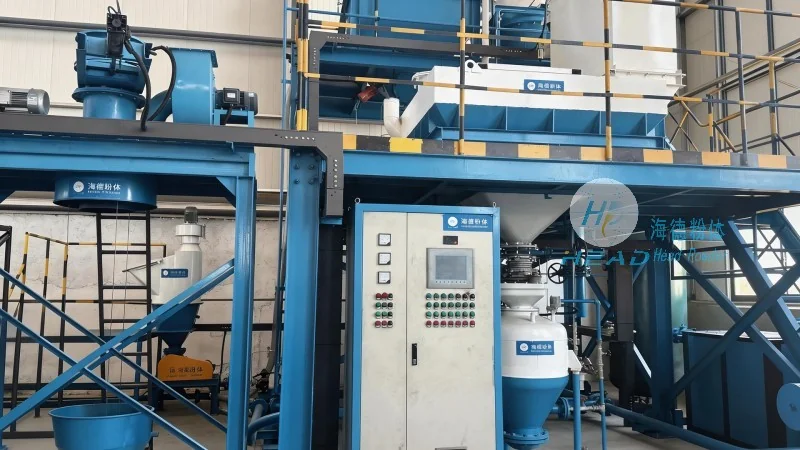
The stone material conveying system is widely used in various industries, including construction, mining, and aggregate processing. In construction projects, it is commonly employed to transport crushed stones and aggregates from stockpiles to the processing plant or construction site. This allows for efficient material supply, ensuring that construction activities proceed without delays due to material shortages. In mining operations, the system is used to transport ore and crushed rock from the extraction site to processing facilities, improving the overall mining efficiency. Additionally, in aggregate processing plants, the system plays a crucial role in moving raw materials through different stages of processing, such as crushing, screening, and sorting. The system's ability to handle bulk materials at high speeds makes it an essential component in these industrial settings, contributing to the smooth operation of the entire production line.
To ensure the long-term performance and safety of the stone material conveying system, regular maintenance and adherence to safety protocols are essential. Regular inspections should be conducted to check the condition of the conveyor belt, pulleys, and idlers for signs of wear and tear. The belt tension should be adjusted periodically to maintain optimal operation and prevent damage to the system components. Lubrication of the drive system and other moving parts is also necessary to reduce friction and extend the lifespan of the equipment. Safety measures, such as proper guarding of moving parts, regular training for operators, and the use of personal protective equipment (PPE), are critical to prevent accidents and injuries. The system should also be equipped with emergency stop mechanisms and overload protection devices to quickly respond to any potential hazards. By following these maintenance and safety guidelines, the stone material conveying system can operate reliably and safely, providing consistent performance over its service life.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top