

[Principle and Working Scene Characteristics of Intelligent Bulk Bag Unloading Pneumatic Conveying E
HeadPowder, a leading provider in the field of material handling solutions, introduces its advanced intelligent bulk bag unloading pneumatic conveying equipment. This technology is designed to streamline the process of handling bulk materials from large containers, such as super sacks or big bags, into processing systems efficiently and safely. The equipment integrates intelligent control systems and robust pneumatic conveying technology to enhance operational efficiency and reduce labor costs in various industrial applications. With a focus on precision and reliability, HeadPowder's solution is tailored to meet the diverse needs of modern industrial operations, ensuring seamless material transfer from bulk bags to downstream processes.
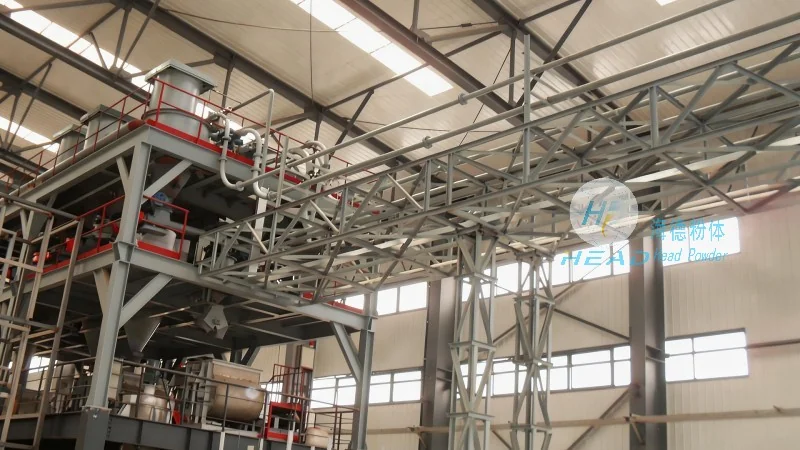
Principle of Operation
The core principle of the intelligent bulk bag unloading pneumatic conveying machine involves the use of compressed air to create a vacuum or pressure differential that moves bulk materials from the bag into a receiving hopper or storage tank. The system typically includes a hopper with a valve mechanism, a vacuum or pressure pump, and a conveying line. When the bulk bag is placed on the hopper, the valve opens, and the pump activates, drawing the material from the bag through the conveying line. The intelligent control system monitors the flow rate, pressure, and other parameters to ensure smooth and controlled material transfer. This principle eliminates the need for manual handling of heavy bags and reduces the risk of material spillage or contamination. The equipment is engineered to handle a wide range of materials, including powders, granules, and even bulk liquids, adapting to different particle sizes and densities through adjustable settings. Advanced sensors and feedback mechanisms ensure that the system operates within optimal parameters, preventing over-pressurization or under-vacuum conditions that could damage the equipment or compromise material quality.
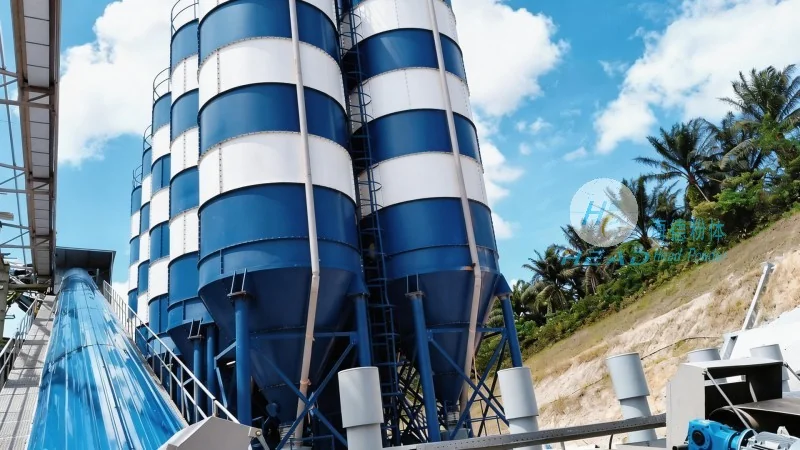
Key Working Scene Characteristics
The intelligent bulk bag unloading pneumatic conveying equipment is particularly suited for industrial environments where large volumes of bulk materials need to be processed. Key characteristics include high throughput capacity, which allows for rapid material transfer even with heavy or abrasive materials. The system is also designed for versatility, accommodating various types of bulk bags and materials, from powders to granules. Another significant characteristic is its integration with automation and control systems, enabling remote monitoring and operation. This feature enhances operational flexibility and allows for real-time adjustments to maintain optimal performance. Additionally, the equipment is built with durability in mind, using high-quality materials that can withstand harsh industrial conditions, ensuring long-term reliability and minimal maintenance. The hygienic design of the equipment, especially in food and pharmaceutical applications, ensures compliance with industry standards and maintains product integrity.

Application Scenarios
HeadPowder's intelligent bulk bag unloading pneumatic conveying equipment is widely used in industries such as chemical, food processing, pharmaceuticals, and mining. In the chemical industry, it is used to handle raw materials like powders and granules, ensuring a clean and efficient transfer process. The food processing industry benefits from the hygienic design of the equipment, which prevents contamination and maintains product quality. In the pharmaceutical sector, the system's ability to handle sensitive materials with precision and minimal exposure is crucial for maintaining compliance with regulatory standards. The mining industry utilizes the equipment to transport bulk ores and minerals from storage bags to processing plants, improving overall production efficiency. Each application leverages the equipment's ability to handle large volumes and maintain consistent material flow, contributing to increased productivity and reduced operational bottlenecks.
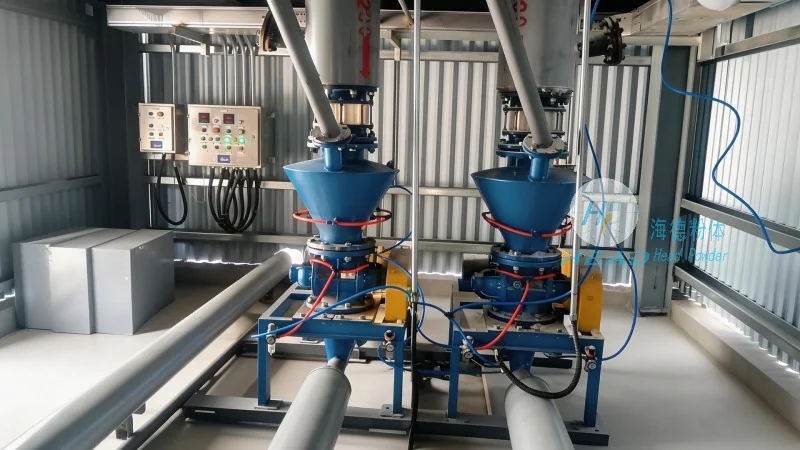
Advantages and Benefits
Implementing intelligent bulk bag unloading pneumatic conveying equipment offers several advantages. Firstly, it significantly reduces labor costs by automating the material handling process, eliminating the need for manual lifting and pouring of heavy bags. This not only saves on labor expenses but also minimizes the risk of workplace injuries associated with manual handling. Secondly, the system minimizes material loss and spillage, which not only reduces waste but also improves workplace safety. The automated control system ensures consistent material flow rates, leading to more accurate inventory management and reduced downtime. Furthermore, the equipment's compact design allows for easy integration into existing production lines, requiring minimal space and infrastructure modifications. This flexibility makes it suitable for both new installations and retrofitting in existing facilities. Lastly, the long-term durability and low maintenance requirements contribute to overall cost savings and operational reliability. The intelligent control system also provides diagnostic capabilities, allowing for proactive maintenance and reducing unexpected breakdowns.