With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Ammonium bicarbonate, a widely used chemical in the fertilizer and food industries, presents unique handling challenges due to its physical properties such as low bulk density and hygroscopic nature. Air-pneumatic conveying has emerged as an effective method to transport this material efficiently and safely. This article explores the fundamental principles behind air-pneumatic conveying for ammonium bicarbonate and highlights the key characteristics of its application in various working scenes.
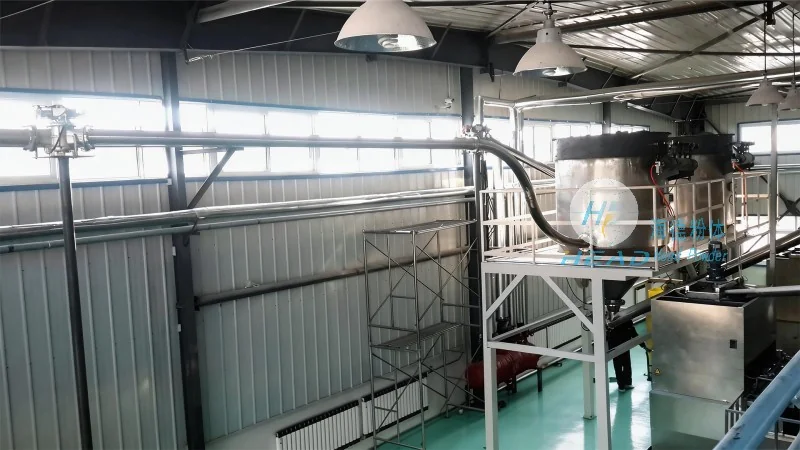
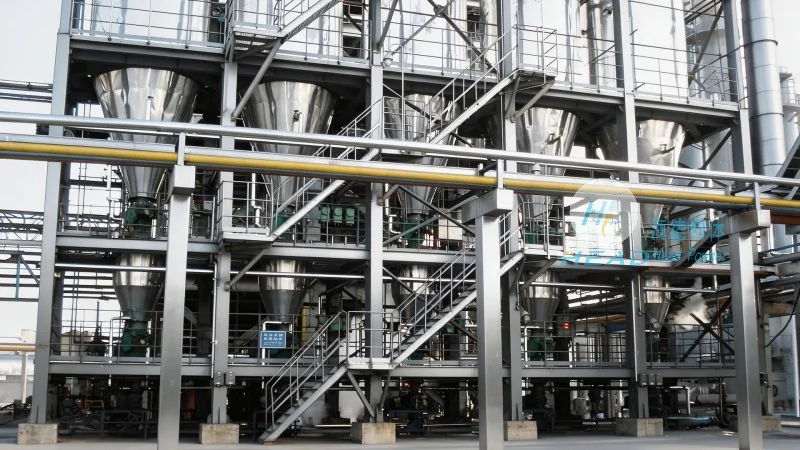
At its core, air-pneumatic conveying utilizes a combination of air flow and pressure to move solid particles through a pipeline. The process involves creating a vacuum or pressure differential that draws or pushes the material along the conveying line. For ammonium bicarbonate, which is a fine, powdery substance, the design of the conveying system must account for its tendency to agglomerate and its sensitivity to moisture. The system typically includes a hopper, a feeder, a conveyor line, and a receiver. The feeder ensures a consistent flow of material into the pipeline, while the conveyor line, often equipped with bends and filters, transports the material to the destination. The receiver then collects the material, often with a dust collection system to prevent environmental contamination. The choice between positive pressure and negative pressure systems depends on factors such as the distance, material characteristics, and environmental regulations. Positive pressure systems use compressed air to push the material, which is suitable for long distances or when the material is prone to dusting. Negative pressure systems, on the other hand, use a vacuum to draw the material, which is ideal for short distances or when the material is less dusty. In the case of ammonium bicarbonate, the system design must also consider the material's hygroscopic properties, as moisture can cause caking and blockages. Therefore, the conveying line is often made of materials resistant to moisture, such as stainless steel, and equipped with heating elements to maintain the material's dryness. The air flow rate is carefully controlled to ensure that the material is conveyed without excessive pressure drop or particle degradation. Proper maintenance of the system, including regular cleaning of filters and checking for leaks, is crucial to maintain its efficiency and prevent downtime.
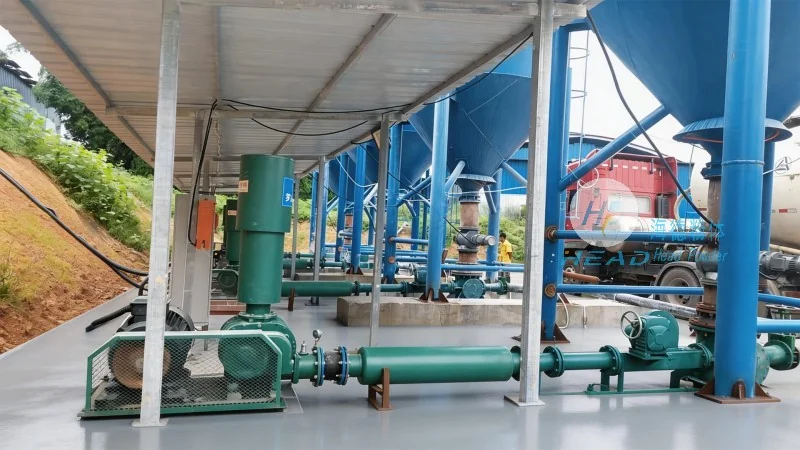
The application of air-pneumatic conveying for ammonium bicarbonate varies across different industrial settings, each with its own unique requirements and characteristics. In the fertilizer production industry, for example, ammonium bicarbonate is often used as a raw material in the manufacturing of nitrogen-based fertilizers. The conveying system must be integrated into the production line, ensuring a continuous flow of material from the storage silo to the reaction vessel. This requires a system that can handle high volumes of material and maintain a consistent flow rate, even under varying production conditions. The working scene in this case is characterized by high throughput, strict quality control, and the need for minimal material loss. The system is typically installed indoors, with proper ventilation to prevent the accumulation of dust and odors. In the food industry, ammonium bicarbonate is used as a leavening agent in baking. The conveying system must be designed to meet food safety standards, with materials that are non-toxic and easy to clean. The working scene here is characterized by lower volumes, higher precision in dosing, and the need for a hygienic environment. The system is often installed in a clean room or a controlled environment, with filters and seals to prevent contamination. Another application scenario is in the chemical processing industry, where ammonium bicarbonate is used as a precursor for other chemicals. The conveying system must be able to handle the material's sensitivity to moisture and its tendency to react with other substances. The working scene in this case is characterized by the need for a closed system to prevent environmental contamination and the need for precise control over the material's temperature and humidity. The system is often integrated with other processing equipment, such as reactors and distillation units, to form a complete production line. In all these scenarios, the key characteristics of the working scene include the need for efficient material transport, minimal downtime, and compliance with industry regulations. The air-pneumatic conveying system must be adaptable to different production volumes and conditions, ensuring that it can meet the specific requirements of each application.
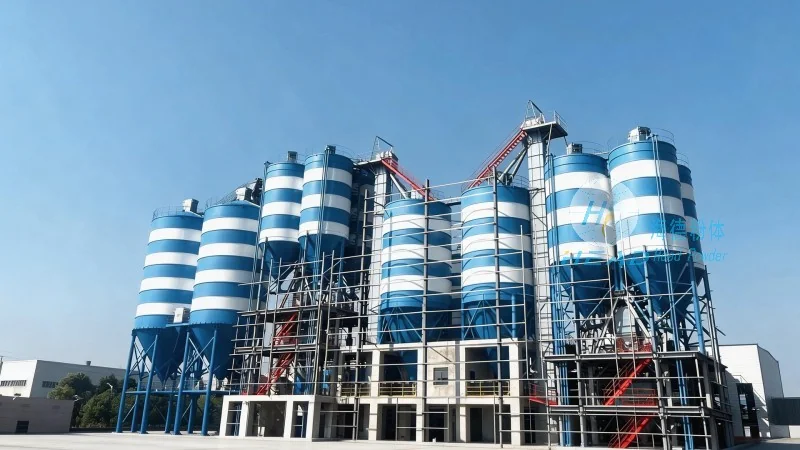
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading engineering company specializing in the design and manufacturing of air-pneumatic conveying systems for various industrial materials. With its headquarters located in Shandong, China, the company has established itself as a trusted partner in the chemical and food industries. HeadPowder's expertise lies in understanding the unique properties of different materials, such as ammonium bicarbonate, and designing customized conveying solutions that meet the specific needs of its clients. The company's team of engineers and technicians has extensive experience in the field of pneumatic conveying, having worked on numerous projects across different industries. HeadPowder's systems are known for their reliability, efficiency, and compliance with international standards. The company provides comprehensive services, including system design, installation, and maintenance, to ensure that its clients can operate their conveying systems at optimal performance. With a focus on innovation and customer satisfaction, HeadPowder continues to be at the forefront of the air-pneumatic conveying industry, providing high-quality solutions for the transportation of industrial materials. The company's commitment to quality and service has earned it a reputation as a reliable partner for businesses looking to improve their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top