With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading enterprise in the field of powder conveying technology, specializes in the design, manufacturing, and supply of advanced fertilizer powder conveying systems. This article delves into the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in modern agricultural and industrial applications.
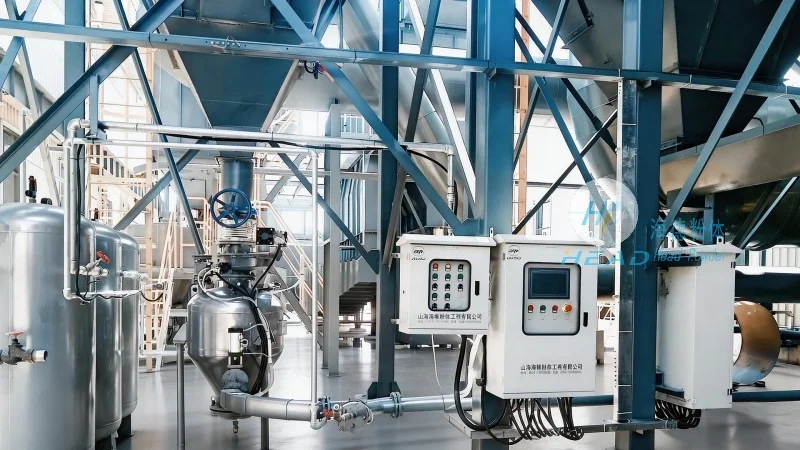
The fertilizer powder conveying system is engineered to efficiently transport bulk fertilizer powders from storage silos or production lines to processing units, packaging facilities, or distribution points. The core principle revolves around the use of mechanical or pneumatic methods to move dry, granular, or powdered materials without causing degradation or segregation. Key components typically include feed hoppers, conveyor belts or pipes, drive mechanisms, and control systems that ensure consistent and reliable material flow. The system's design prioritizes factors such as material compatibility, operational efficiency, and safety, addressing the unique challenges posed by fertilizer powders, which can be abrasive, hygroscopic, or prone to dust generation.
HeadPowder's fertilizer powder conveying systems are tailored to meet diverse operational requirements across various industries. One prominent working scene is in large-scale agricultural fertilizer production facilities, where these systems facilitate the seamless transfer of raw materials like urea, ammonium nitrate, or phosphate-based powders from storage silos to mixing and granulation units. The systems are designed to handle high volumes with minimal downtime, ensuring that production lines operate at optimal efficiency. Another critical application is in bulk handling and distribution centers, where the equipment efficiently transports finished fertilizer products to storage silos or loading docks for transportation to farms or retail outlets. The systems are also utilized in industrial settings, such as chemical plants or fertilizer manufacturing complexes, where precise control over material flow is essential to maintain product quality and prevent contamination.
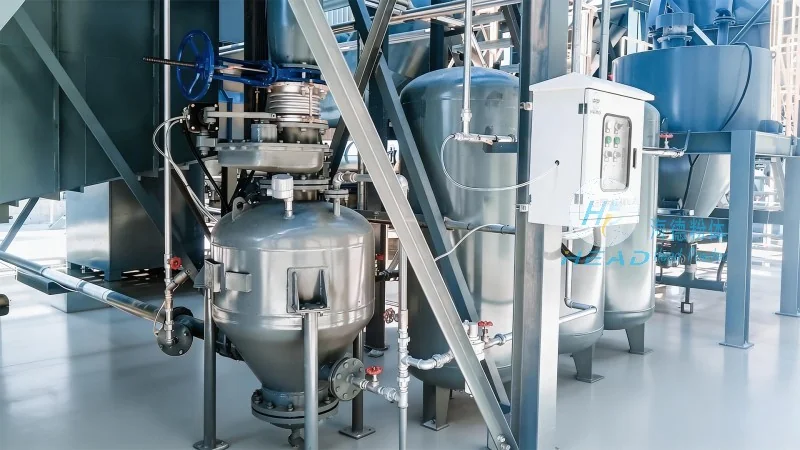
HeadPowder's fertilizer powder conveying systems are built with advanced technology to enhance operational performance and reliability. The use of high-quality materials, such as stainless steel or corrosion-resistant alloys, ensures durability and resistance to the chemical properties of fertilizers. The systems incorporate intelligent control systems that allow for real-time monitoring of flow rates, pressure, and temperature, enabling operators to adjust parameters dynamically to maintain optimal performance. Additionally, the design minimizes material degradation and segregation, which is crucial for maintaining the nutritional value and quality of the fertilizer products. The systems are also engineered for low maintenance, with easy access to components for inspection and repair, reducing operational costs and increasing overall productivity.
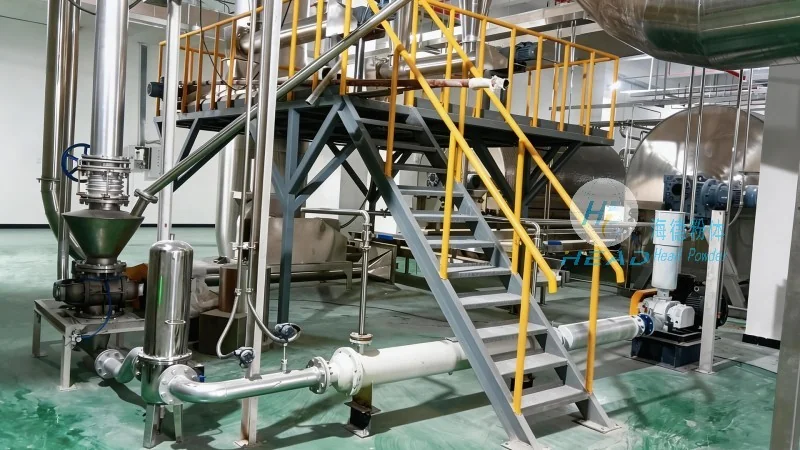
Recognizing that each fertilizer production or handling facility has unique requirements, HeadPowder offers customized solutions tailored to specific working conditions. The company's engineering team works closely with clients to understand their operational needs, including material types, flow rates, and space constraints, to design systems that meet exact specifications. Customization options may include adjustable conveyor speeds, variable pipe diameters, or integrated dust control systems, ensuring that the equipment is optimized for the specific fertilizer being handled. This adaptability makes HeadPowder's systems suitable for a wide range of applications, from small-scale agricultural operations to large industrial complexes, providing a versatile solution for bulk powder handling.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of fertilizer powder conveying systems that combine advanced technology with practical design to meet the demands of modern agricultural and industrial sectors. The company's commitment to quality, efficiency, and customer satisfaction has established it as a leader in the field, delivering reliable and effective solutions for bulk powder handling. By understanding the core principles and working scene characteristics of fertilizer powder conveying systems, HeadPowder continues to innovate and provide solutions that enhance operational performance and ensure the quality of fertilizer products. With a focus on customization and adaptability, the company remains dedicated to supporting the needs of its clients in the fertilizer industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top