Working Principle and Features of a Pneumatic Conveyor for Glucose Powder Material
Release time:2026-09-18 14:01:24
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
For industries dealing with bulk materials like glucose powder, efficient and reliable material handling solutions are crucial. A pneumatic conveyor system designed specifically for glucose powder material offers a seamless way to transport these fine powders with precision and minimal loss. This article explores the working principle and key features of such a specialized pneumatic conveyor, highlighting how it addresses the unique challenges of handling glucose powder.
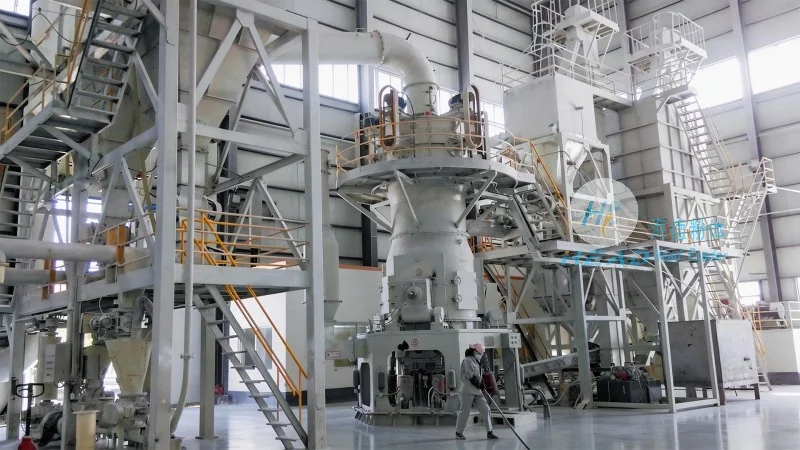
Introduction to Glucose Powder Pneumatic Conveyors
Glucose powder, a common ingredient in food, pharmaceutical, and chemical industries, requires careful handling due to its fine particle size and potential for dust generation. Traditional methods like bucket elevators or belt conveyors may not be suitable for such delicate materials as they can cause product degradation, blockages, or contamination. A pneumatic conveyor for glucose powder, engineered by Shandong HeadPowder Engineering Co., Ltd., provides an advanced solution that ensures efficient, clean, and low-maintenance material transport. This system is designed to meet the stringent requirements of industries where product purity and consistency are paramount.
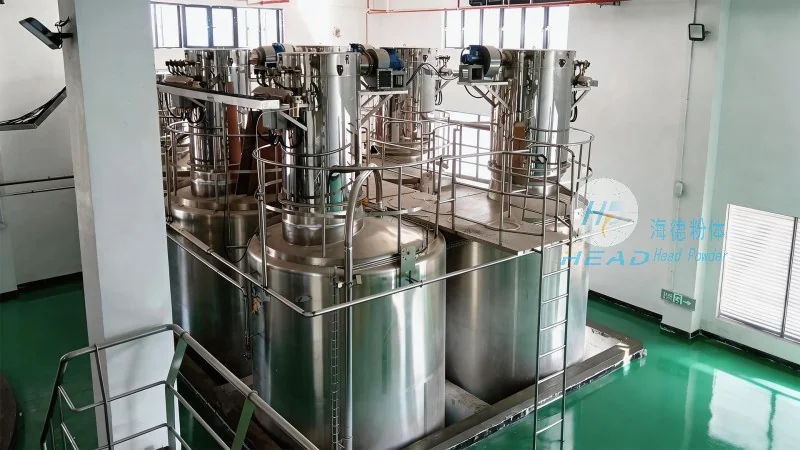
The Working Principle of Glucose Powder Pneumatic Conveyors
The core of a pneumatic conveyor for glucose powder is its ability to use air pressure to move material through a pipeline. The system operates on the principle of creating a pressure differential between the inlet and outlet of the conveyor. Here’s a step-by-step breakdown of how it works:
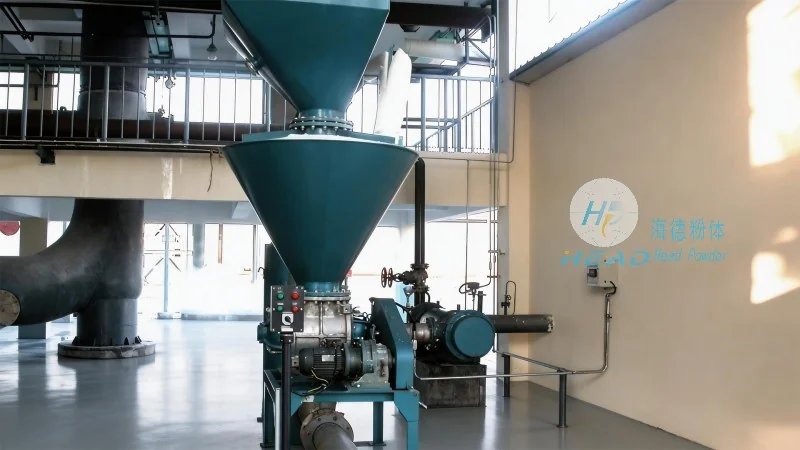
- Air Intake and Material Loading: The process begins with the introduction of air into the conveyor system. The glucose powder is then fed into the inlet hopper, where it is mixed with the air stream. This mixing is typically achieved using a rotary valve or a venturi injector, which ensures the powder is fully entrained by the air.
- Transport Through Pipeline: Once the powder is entrained, the air-powder mixture travels through the pipeline under pressure. The pressure maintained in the system (either positive or negative, depending on the design) propels the material forward. The pipeline is usually made of materials resistant to corrosion and abrasion, such as stainless steel or food-grade plastic, to prevent contamination and ensure durability.
- Discharge and Separation: At the discharge end, the air and powder are separated. This is typically done using a cyclone separator or a filter, which allows the air to be recirculated while the glucose powder is collected in a receiving bin. The separation process is designed to minimize product loss and maintain the quality of the material.
Key Features of Glucose Powder Pneumatic Conveyors
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing pneumatic conveyors tailored to the needs of glucose powder handling. The key features of their systems include:
- Low Product Loss and Contamination: The design minimizes product loss during transport by ensuring efficient air-powder separation. The use of high-quality materials and precise engineering reduces the risk of contamination, making it suitable for food and pharmaceutical applications.
- Energy Efficiency: Modern pneumatic conveyor systems are engineered for energy efficiency. By optimizing the air flow and pressure, the system reduces energy consumption while maintaining high transport capacity. This not only lowers operational costs but also aligns with sustainability goals.
- Easy Maintenance and Cleaning: The system is designed for easy maintenance and cleaning, which is essential for industries where hygiene is critical. The components are easily accessible, and the system can be quickly disassembled for cleaning, reducing downtime and ensuring compliance with regulatory standards.
- Customizable Design: Shandong HeadPowder Engineering Co., Ltd. offers customizable solutions to meet specific operational requirements. Whether it's the length of the pipeline, the capacity, or the type of material handling, the system can be tailored to fit the unique needs of the client. This flexibility ensures optimal performance and cost-effectiveness.
Benefits of Using a Glucose Powder Pneumatic Conveyor
Implementing a pneumatic conveyor for glucose powder offers several benefits that enhance operational efficiency and product quality:
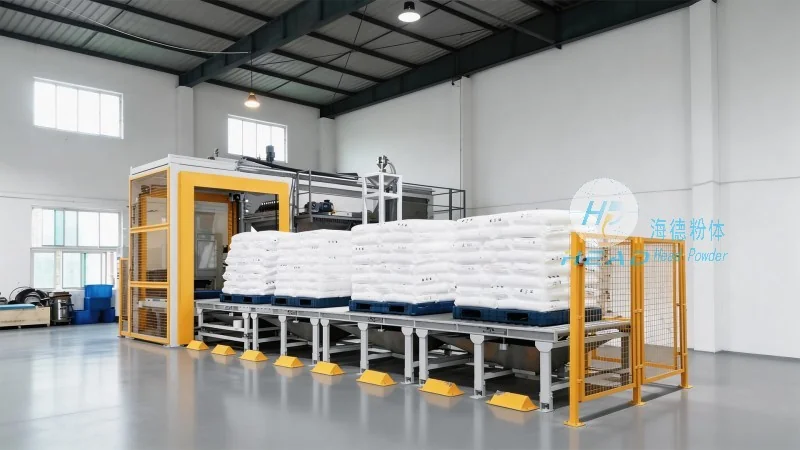
- Improved Product Purity: The enclosed system prevents contamination from external sources, ensuring that the glucose powder remains pure and free from dust or other particles.
- Reduced Downtime: The system’s design minimizes blockages and clogs, reducing the risk of downtime and increasing overall productivity.
- Space Efficiency: Pneumatic conveyors are compact and can be installed in tight spaces, making them ideal for facilities with limited floor space.
- Versatility: The system can handle various particle sizes and flow rates, making it suitable for different production stages, from raw material transport to final product packaging.
Conclusion
A pneumatic conveyor for glucose powder is a sophisticated solution that addresses the unique challenges of handling fine, delicate materials. By leveraging the principles of air pressure and efficient separation, these systems provide reliable, clean, and efficient material transport. Shandong HeadPowder Engineering Co., Ltd., with its expertise in engineering and manufacturing, offers high-quality pneumatic conveyors that meet the demanding requirements of industries dealing with glucose powder. Whether it's for food processing, pharmaceutical manufacturing, or chemical production, investing in a specialized pneumatic conveyor can significantly improve operational efficiency and product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China
