With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd. specializes in industrial material handling solutions, with a focus on developing efficient equipment for transporting bulk materials like bentonite powder. The company's expertise lies in designing and manufacturing pneumatic conveying systems that ensure reliable, cost-effective, and safe material transport. HeadPowder's bentonite powder pneumatic conveying machine is engineered to meet the diverse needs of clients across various industries, including chemical processing, pharmaceuticals, and food production. By leveraging advanced engineering and high-quality materials, the equipment delivers superior performance while minimizing product loss and operational downtime.
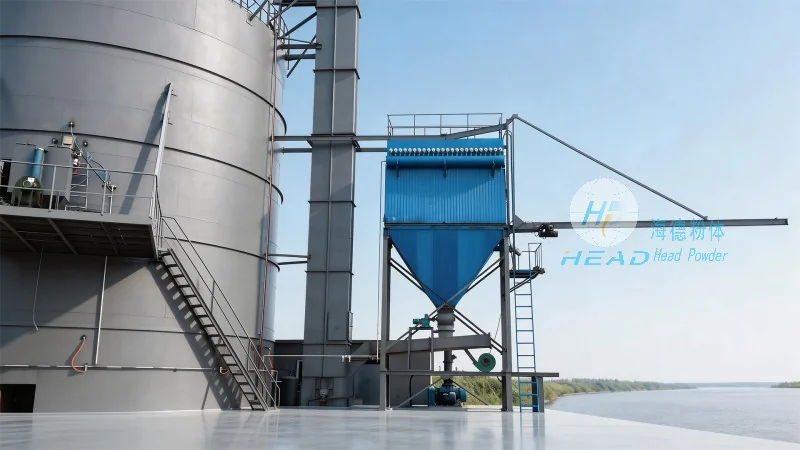
The bentonite powder pneumatic conveying machine operates based on the principle of pneumatic transport, which utilizes compressed air to move dry bulk materials through a sealed pipeline system. The process begins with the bentonite powder being fed into a hopper or feeder, where it is then introduced into the conveying pipeline. Compressed air is introduced into the pipeline, creating a flow that propels the powder forward. The machine employs a combination of positive and negative pressure systems to achieve efficient material transport. In the positive pressure system, air is forced through the pipeline, pushing the bentonite powder along its path. Conversely, the negative pressure system draws the material from the source by creating a vacuum in the pipeline. This dual-pressure approach allows for flexible operation, enabling the machine to handle both short and long-distance conveying tasks with equal efficiency. The system also incorporates air filtration and separation mechanisms to prevent dust accumulation and maintain air quality, ensuring compliance with environmental regulations and operational safety standards.
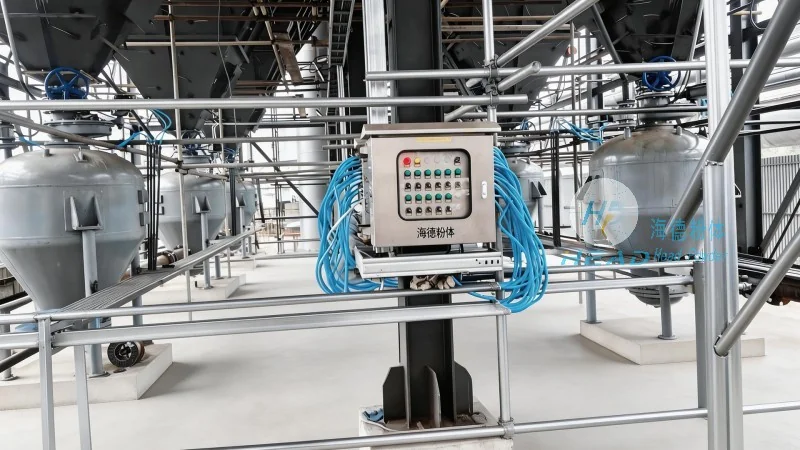
Shandong HeadPowder Engineering Co., Ltd.'s bentonite powder pneumatic conveying machine is equipped with several key features that enhance its performance and reliability. Firstly, the machine features a robust construction using high-quality materials, such as stainless steel and corrosion-resistant alloys, which are specifically chosen to withstand the abrasive and moisture-rich nature of bentonite powder. This ensures long-term durability and minimal maintenance requirements. The equipment is also designed with precision-engineered components, including high-capacity feeders and adjustable air valves, to maintain consistent material flow rates and prevent blockages. Advanced control systems are integrated into the machine, allowing for real-time monitoring of pressure, flow rate, and material level, enabling operators to adjust the conveying process dynamically and optimize efficiency. The system also includes automatic cleaning and maintenance functions, reducing downtime and ensuring continuous operation. Another notable feature is the machine's ability to handle varying particle sizes and moisture content in bentonite powder, making it versatile for different industrial applications. The compact and modular design of the equipment allows for easy installation and integration into existing production lines, while its low energy consumption contributes to cost savings and environmental sustainability.
The bentonite powder pneumatic conveying machine offers several advantages over traditional material handling methods, such as bucket elevators or belt conveyors. One of the primary benefits is the ability to transport bentonite powder in a closed system, which minimizes dust exposure and improves workplace safety. This is particularly important in industries where dust can pose health risks or affect product quality. Additionally, the pneumatic conveying system eliminates the need for manual handling, reducing labor costs and the risk of product contamination. The machine also provides a more hygienic and controlled environment for handling sensitive materials like bentonite powder, which is critical in pharmaceutical and food processing applications. Furthermore, the system's ability to handle high volumes of material at a consistent rate enhances production efficiency, allowing manufacturers to meet increasing demand without compromising quality. The low maintenance requirements and long service life of the equipment further contribute to its cost-effectiveness, making it a preferred choice for industrial applications.
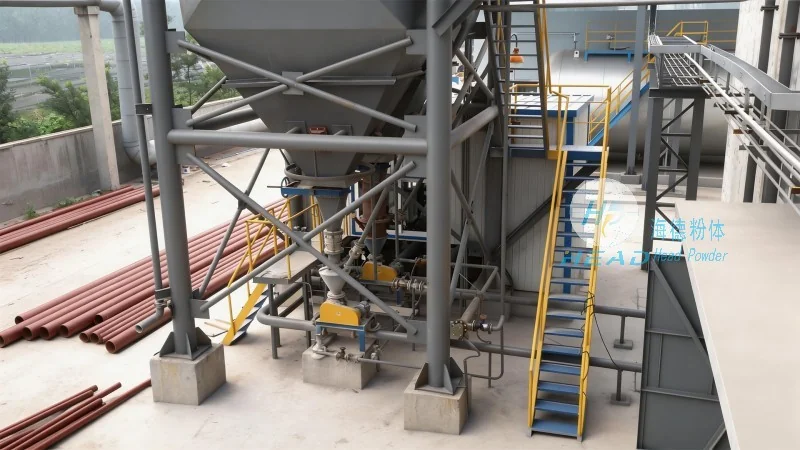
The bentonite powder pneumatic conveying machine is widely used in various industrial sectors due to its versatility and efficiency. In the chemical industry, it is commonly employed for transporting bentonite powder used in the production of drilling fluids, adsorbents, and other chemical products. The machine's ability to handle fine powders and maintain consistent flow rates ensures that the final product meets quality specifications. In the pharmaceutical industry, the equipment is used for the transport of bentonite powder in the manufacturing of medications and supplements, where hygiene and product purity are paramount. The closed system and advanced filtration features of the machine help maintain a sterile environment, reducing the risk of contamination. Performance metrics of the machine typically include a conveying capacity ranging from 5 to 50 tons per hour, depending on the system design and application. The system's pressure range is usually between 0.5 to 2.0 bar, with adjustable air flow rates to accommodate different material characteristics. The machine's efficiency is measured by its ability to transport material with minimal pressure drop and energy consumption, ensuring optimal performance while reducing operational costs. Overall, the bentonite powder pneumatic conveying machine from Shandong HeadPowder Engineering Co., Ltd. provides a reliable and efficient solution for handling bentonite powder, meeting the needs of modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top