With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in the design and production of coffee powder material pneumatic conveying systems. Based in Shandong, China, the company has established itself as a trusted provider of efficient and reliable solutions for the coffee industry. This article explores the working principle and key features of these systems, highlighting how they enhance operational efficiency and product quality in coffee processing facilities.
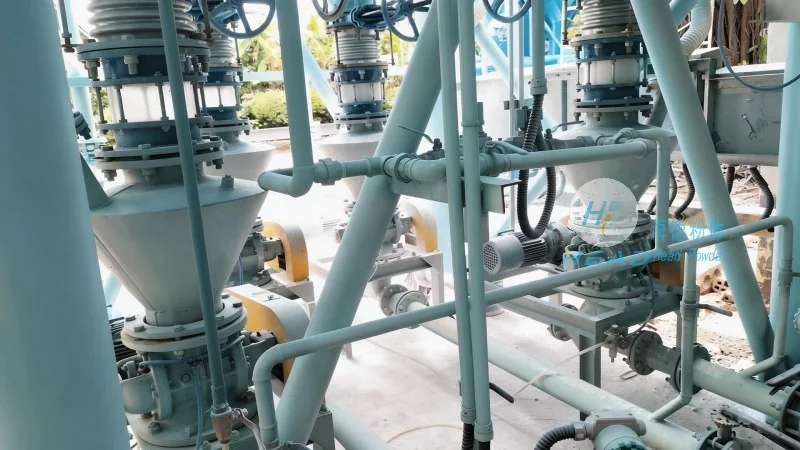
The core of a coffee powder pneumatic conveying system lies in its ability to transport dry, fine materials like coffee powder through an air stream. The system typically operates under either positive pressure (where air is forced through the system) or negative pressure (where air is drawn out). In the case of coffee powder, positive pressure systems are more common as they ensure consistent and controlled flow. The process begins with the coffee powder being fed into a hopper or feeder, which then delivers the material into a venturi or a series of pipes. Compressed air is introduced at the inlet, creating a high-velocity air stream that carries the coffee powder particles through the pipeline. At the discharge end, a separator or cyclone separates the coffee powder from the air, allowing the powder to be collected in a designated container while the air is either filtered or recirculated. This continuous cycle ensures a seamless and efficient transfer of coffee powder from the source to the destination, minimizing material loss and contamination.
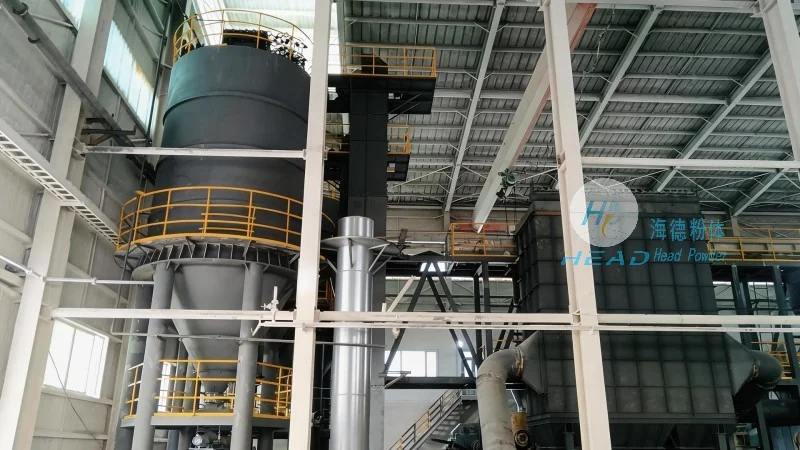
HeadPowder's coffee powder pneumatic conveying systems are engineered with several distinct features that set them apart in the industry. Firstly, they offer high efficiency in material transport, capable of handling large volumes of coffee powder with minimal energy consumption. The systems are designed to maintain a clean and hygienic environment, which is crucial for maintaining the quality and safety of coffee products. Unlike traditional mechanical conveyors, pneumatic systems eliminate the risk of cross-contamination and reduce the likelihood of dust accumulation, making them ideal for food processing applications. Additionally, these systems provide flexibility in terms of layout and installation, as they can be configured to fit various plant designs and space constraints. The adjustable air pressure and flow rates allow operators to control the speed and volume of coffee powder transfer, ensuring precise delivery to different processing stages. Maintenance is also simplified, with modular components that are easy to access and replace, reducing downtime and operational costs. The systems are also equipped with safety features such as pressure relief valves and air filtration systems, ensuring safe and reliable operation in industrial settings.
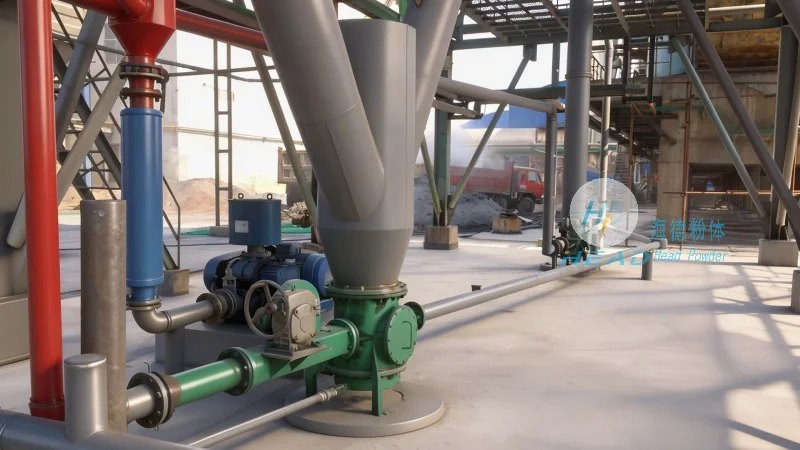
Coffee powder pneumatic conveying systems from headpowder are widely used in various stages of coffee processing, from raw material handling to final product packaging. In coffee roasting facilities, these systems efficiently transport roasted coffee beans to grinding machines, ensuring a consistent supply of raw material for the next step. During the grinding process, the systems handle the fine coffee powder, preventing clogging and maintaining uniform particle size. In the blending and packaging stages, the pneumatic conveyors deliver the coffee powder to storage silos or packaging lines, maintaining product integrity and preventing exposure to external contaminants. The benefits of using these systems extend beyond efficiency; they also contribute to improved product quality by reducing the risk of moisture absorption and oxidation, which can affect the flavor and aroma of coffee. Furthermore, the systems enhance workplace safety by eliminating manual handling of heavy or dusty materials, reducing the risk of respiratory issues and other health hazards. Overall, the adoption of coffee powder pneumatic conveying systems in coffee processing facilities leads to increased productivity, reduced operational costs, and higher product quality, making them a valuable investment for businesses in the coffee industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top