With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Quartz stone powder pneumatic conveying equipment is a critical component in modern industrial processing, designed to efficiently transport fine powders like quartz stone. This equipment plays a vital role in various industries, including mining, construction, and manufacturing, by providing a reliable and efficient method for material handling. The technology behind these systems combines the principles of fluidization and air movement to achieve seamless powder transport, minimizing the need for traditional mechanical conveyors that often suffer from issues like clogging and wear.
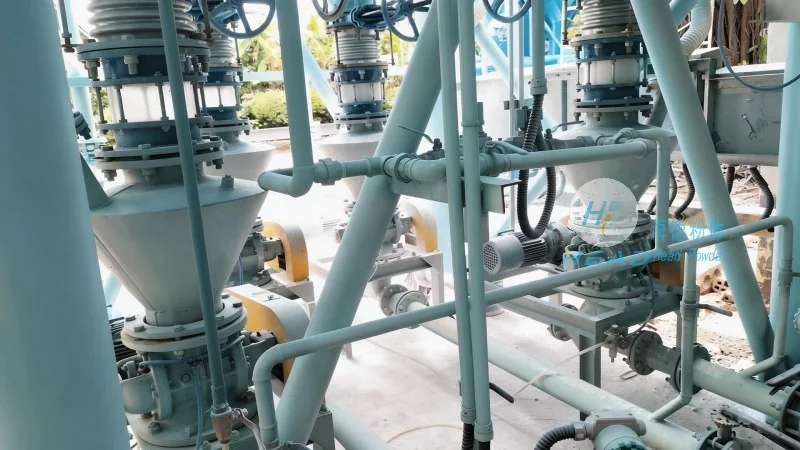
The core mechanism of quartz stone powder pneumatic conveying equipment revolves around the use of compressed air to move the powder. The process typically begins with the powder being fed into a hopper or feeder, where it is then introduced into a pipeline. Compressed air is then introduced into the pipeline, creating a flow that carries the powder particles along. This method is known as dilute-phase pneumatic conveying, which is particularly effective for fine powders like quartz stone due to its ability to maintain particle integrity and prevent agglomeration. The equipment utilizes a series of components, including a feeder, a pipeline system, and a receiver, to ensure the smooth and continuous transport of the material. The compressed air acts as the medium, providing the necessary force to move the powder while maintaining a consistent flow rate. The system is designed to handle varying particle sizes and moisture content, making it versatile for different quartz stone applications. The working principle also involves controlling the air pressure and flow rate to optimize the conveying efficiency, ensuring that the powder is transported without excessive pressure drops or particle degradation.
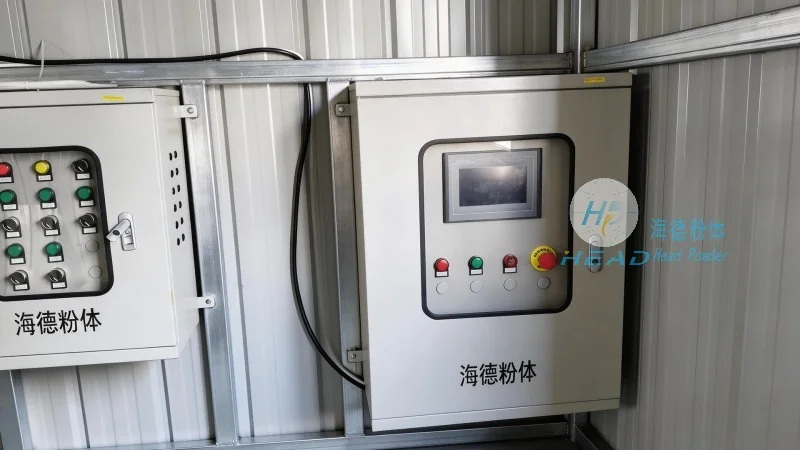
Quartz stone powder pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. offers several distinct features that enhance its performance and reliability. One of the primary features is its ability to handle fine and abrasive materials, such as quartz stone, without causing wear or damage to the system components. The equipment is constructed with high-quality materials, including corrosion-resistant metals and durable plastic components, to withstand the harsh conditions of quartz stone processing. Another key feature is the system's flexibility in terms of layout and integration. It can be customized to fit various plant configurations, allowing for seamless integration with existing production lines. The equipment also includes advanced control systems that monitor and adjust the air pressure, flow rate, and powder feed rate in real-time, ensuring optimal performance and preventing operational issues. Additionally, the system is designed for low maintenance, with easy access to components for inspection and replacement, reducing downtime and operational costs. The use of pneumatic conveying also eliminates the need for traditional conveyor belts or buckets, which can be prone to clogging and require frequent cleaning. This results in a cleaner and more hygienic processing environment, which is particularly important in industries where product purity is critical.
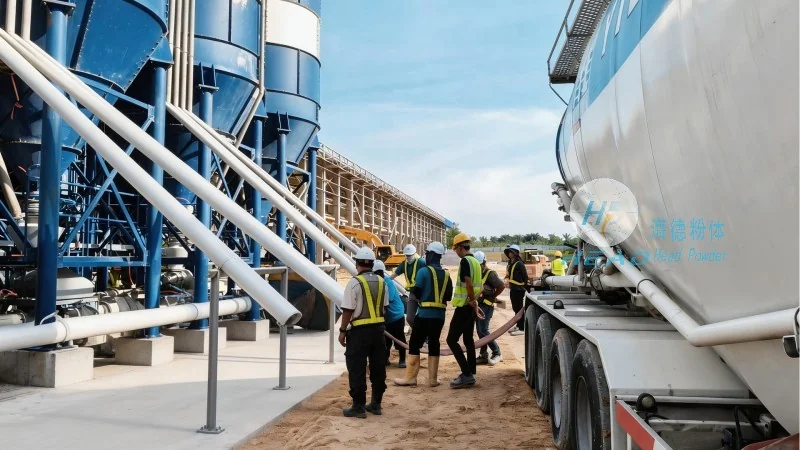
Implementing quartz stone powder pneumatic conveying equipment provides numerous advantages for industrial operations. One of the most significant benefits is the reduction in material handling costs. By eliminating the need for traditional mechanical conveyors, companies can save on maintenance, replacement, and energy costs. The equipment also improves operational efficiency by providing a continuous and reliable flow of quartz stone powder, reducing bottlenecks and increasing production throughput. Another advantage is the enhanced safety and hygiene in the processing environment. Pneumatic conveying systems are enclosed, preventing dust emissions and minimizing the risk of dust explosions, which is a critical concern in quartz stone processing. The system also allows for better control over the powder's moisture content and particle size distribution, ensuring consistent product quality. Furthermore, the equipment's compact design saves valuable floor space in industrial facilities, making it ideal for plants with limited space. The use of compressed air as the conveying medium also reduces the risk of product contamination, as there is no direct contact between the powder and the conveyor components. This is particularly important in applications where the quartz stone is used in food or pharmaceutical industries, where product purity is paramount. Overall, the adoption of quartz stone powder pneumatic conveying equipment leads to improved operational efficiency, reduced costs, and enhanced safety in industrial processing.
Quartz stone powder pneumatic conveying equipment is widely used in various industrial applications where fine quartz stone powders need to be transported efficiently. In the mining industry, it is used to transport quartz stone from processing plants to storage facilities or to other processing units. The equipment is also used in the construction industry for transporting quartz stone powders used in concrete and mortar production. In manufacturing, it is employed in the production of quartz-based products, such as glass and ceramics, where the consistent transport of fine powders is essential for maintaining product quality. The equipment is also utilized in the chemical industry for transporting quartz stone powders used as fillers or additives in various chemical formulations. Additionally, it is used in the pharmaceutical industry for transporting quartz stone powders used in the production of certain medications or as a filler in tablets. The versatility of the equipment makes it suitable for a wide range of applications, from small-scale operations to large-scale industrial plants. The ability to customize the system to meet specific application requirements ensures that it can be adapted to various production needs, making it a valuable asset in any industrial setting.
In conclusion, quartz stone powder pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. offers a reliable and efficient solution for transporting fine quartz stone powders. The working principle, which relies on compressed air to move the powder, ensures a smooth and continuous transport process. The key features, including durability, flexibility, and advanced control systems, enhance the equipment's performance and reliability. The advantages of using this equipment, such as cost reduction, improved efficiency, and enhanced safety, make it a valuable investment for industrial operations. With its wide range of applications and customizable design, the quartz stone powder pneumatic conveying equipment is an essential component in modern industrial processing, contributing to improved productivity and product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top