

Working Principle and Features of Capsule Material Conveying System Equipment
For pharmaceutical and food processing industries, efficient and reliable capsule material conveying systems are crucial for maintaining production flow and ensuring product quality. The capsule material conveying system, as offered by Shandong HeadPowder Engineering Co., Ltd. (commonly known as headpowder), is designed to handle the transportation of capsule materials with precision and durability. This article will delve into the working principle and key features of such equipment, providing a comprehensive overview for potential users.
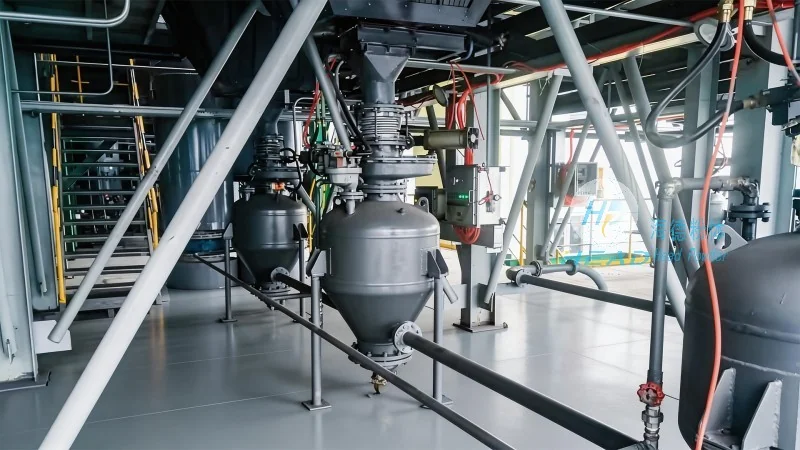
Working Principle of Capsule Material Conveying Systems
The core working principle of a capsule material conveying system involves the use of mechanical components to transport capsule materials from one location to another within a production facility. Typically, these systems employ a combination of rollers, belts, or conveyor belts to move the capsules along a designated path. The process begins with the loading of capsule materials into a hopper or feeding mechanism. From there, the material is fed into the conveyor system, which uses a series of driven rollers or a belt to transport the capsules. The speed and direction of the conveyor can be adjusted to match the production requirements, ensuring smooth and consistent movement. Additionally, the system may include sensors and control mechanisms to monitor the flow of capsules and prevent jams or blockages. This automated approach minimizes human intervention, reducing the risk of errors and improving overall operational efficiency.
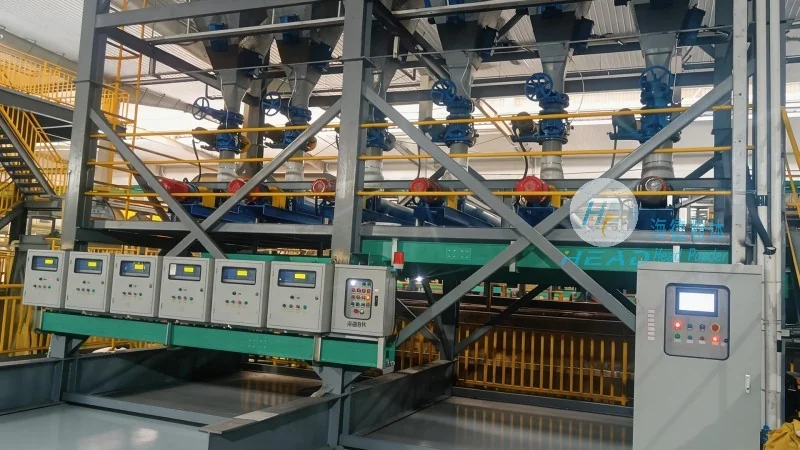
Key Features of Capsule Material Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd. specializes in manufacturing high-quality capsule material conveying systems that are equipped with several advanced features. One of the primary features is the robust construction, which is designed to withstand the rigors of continuous operation in industrial environments. The equipment is typically made from stainless steel or other corrosion-resistant materials, ensuring durability and hygiene, which is essential for pharmaceutical applications. Another notable feature is the adjustable speed control, allowing operators to modify the conveyor speed based on the specific needs of the production line. This flexibility helps in maintaining optimal processing times and reducing bottlenecks. The system also includes safety features such as emergency stop buttons and overload protection, which enhance operational safety and prevent damage to the equipment. Furthermore, the design incorporates easy maintenance components, such as accessible parts and quick-release mechanisms, which reduce downtime and maintenance costs. The integration of sensors for real-time monitoring provides valuable data on the material flow, enabling proactive maintenance and troubleshooting.
Benefits of Using Capsule Material Conveying Systems
Implementing a capsule material conveying system offers numerous benefits for businesses in the pharmaceutical and food industries. Firstly, it significantly improves production efficiency by automating the material handling process. This reduces the time and labor required for manual transportation, allowing workers to focus on other critical tasks. Secondly, the system enhances product quality by minimizing the risk of capsule damage or contamination during transportation. The gentle handling of capsules ensures that the final product maintains its integrity and meets quality standards. Thirdly, the system provides better control over the production process, enabling precise monitoring and adjustment of material flow. This leads to consistent output and reduced waste. Additionally, the automated nature of the system reduces human error, which is particularly important in industries where precision is paramount. The use of advanced materials and design also contributes to longer equipment lifespan and lower maintenance costs over time.

Application Scenarios
Capsule material conveying systems are widely used in various applications within the pharmaceutical and food processing sectors. For instance, in pharmaceutical manufacturing, these systems are employed to transport empty capsules from the filling machine to the packaging line. In food processing, they are used to move capsule-shaped food products from the production line to the packaging area. The versatility of the system allows it to be adapted to different production volumes and speeds, making it suitable for both small-scale and large-scale operations. The system's ability to handle different types of capsules, including hard gelatin and soft gelatin capsules, further expands its applicability. Additionally, the system can be integrated with other production equipment, such as filling machines and packaging lines, to create a seamless production flow. This integration enhances overall operational efficiency and reduces the need for manual transfers between equipment.