With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Your current position:首页 >> News >> Updates

Working Principle and Features of Rare Earth Mineral Powder Material Handling Systems

Release time:2026-09-17 19:01:25
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang

Understanding the working principle and features of rare earth mineral powder material handling systems is crucial for industries dealing with these specialized materials. These systems are designed to efficiently transport, process, and manage rare earth mineral powders, which are essential components in various high-tech applications. The following sections provide a detailed overview of how such systems operate and the key characteristics that make them effective.
Working Principle and Features of Rare Earth Mineral Powder Material Handling Systems

Working Principle of Rare Earth Mineral Powder Material Handling Systems

Rare earth mineral powder material handling systems typically operate through a combination of mechanical and pneumatic components tailored to handle the unique properties of rare earth powders. The core working principle involves the following steps:

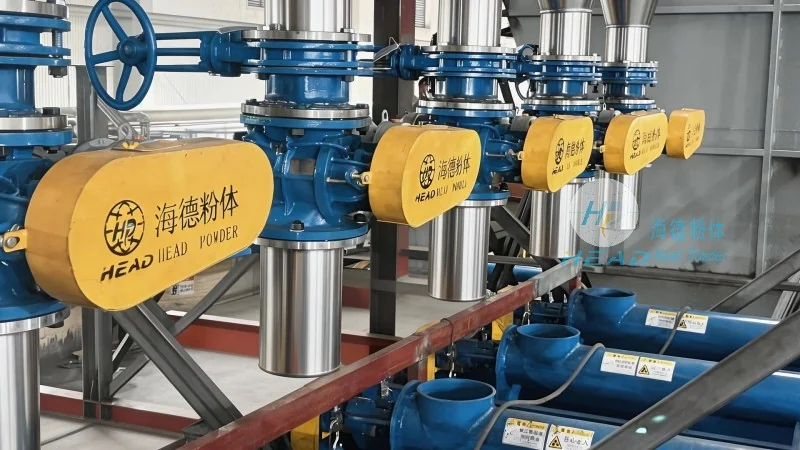
  1. Feeding and Conveying: The system starts with the feeding of rare earth mineral powders into a hopper or feeder. This initial step ensures a consistent and controlled flow of material into the system. The feeder may use gravity or mechanical means to move the powder into the conveyor section.
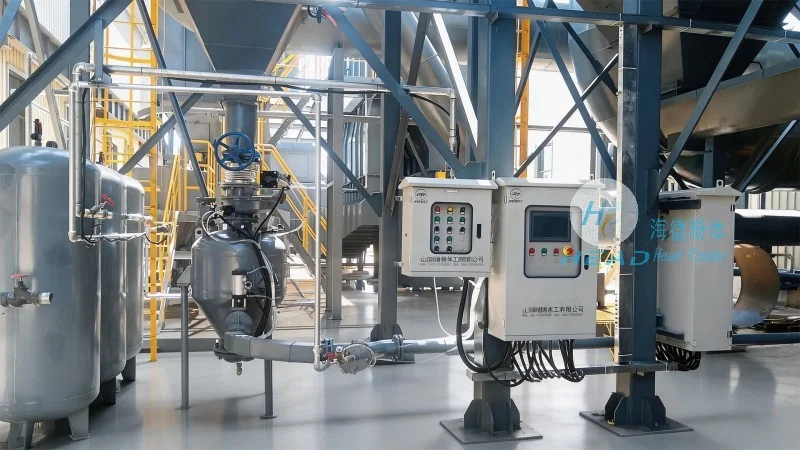
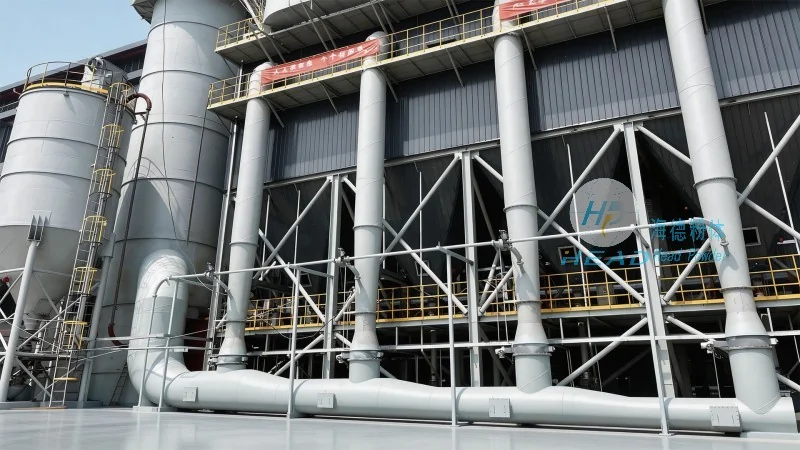
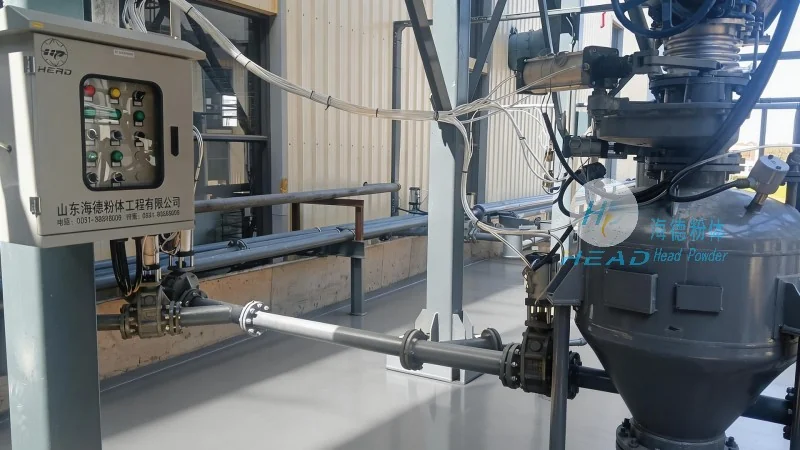
  2. Conveying Mechanism: The primary conveying method for rare earth mineral powders often involves pneumatic conveying systems, such as pressure or vacuum pneumatic conveyors. These systems use air to transport the fine powders through pipelines, minimizing dust generation and ensuring a smooth flow. Alternatively, mechanical conveyors like screw conveyors or belt conveyors may be used for bulk handling, especially when dealing with larger particle sizes or higher volumes.
  3. Distribution and Processing: Once the powder reaches the processing stage, it may be directed to various components for further processing, such as mixing, screening, or packaging. The system is designed to maintain the integrity of the rare earth powders, preventing agglomeration or contamination during transport.
  4. Control and Monitoring: Advanced control systems are integrated into the material handling system to monitor parameters like flow rate, pressure, and temperature. These controls ensure optimal performance and allow for real-time adjustments to maintain consistent material quality and system efficiency.

Overall, the working principle of these systems focuses on precision, efficiency, and safety, addressing the challenges posed by rare earth mineral powders, which are often fine, abrasive, and valuable. The design of the system is tailored to minimize dust, prevent material loss, and ensure a stable operation, making it suitable for industrial applications where reliability is paramount.
Working Principle and Features of Rare Earth Mineral Powder Material Handling Systems

Key Features of Rare Earth Mineral Powder Material Handling Systems

Several key features distinguish rare earth mineral powder material handling systems from conventional material handling solutions. These features are critical for meeting the specific demands of handling rare earth powders and ensuring operational excellence. The main features include:

  • High Efficiency and Low Maintenance: Modern systems are engineered for high efficiency, with components designed to minimize energy consumption and reduce downtime. The use of durable materials and advanced sealing technologies helps in reducing maintenance requirements, leading to lower operational costs over the system's lifecycle.
  • Environmental Protection and Dust Control: Rare earth mineral powders are often fine and can generate significant dust during handling. These systems incorporate effective dust collection and filtration systems to ensure compliance with environmental regulations and maintain a safe working environment. The design minimizes particle emission, protecting both equipment and personnel.
  • Customization and Flexibility: Systems are often customizable to meet the specific requirements of different applications and processing needs. This flexibility allows for integration with existing production lines and adaptation to varying material properties, such as particle size, moisture content, or bulk density.
  • Advanced Control and Automation: Integration of sophisticated control systems enables automated operation, reducing the need for manual intervention and improving process consistency. Real-time monitoring and data analysis help in optimizing performance and identifying potential issues before they impact production.
  • Material Compatibility and Safety: The components used in the system are selected to be compatible with rare earth mineral powders, which may be corrosive or have specific handling requirements. Safety features, such as explosion-proof designs and emergency shut-off mechanisms, are incorporated to protect against potential hazards and ensure safe operation.

These features collectively contribute to the effectiveness of rare earth mineral powder material handling systems, making them indispensable in industries that rely on these critical materials. The combination of efficiency, safety, and adaptability ensures that these systems can meet the evolving demands of modern manufacturing processes.
Working Principle and Features of Rare Earth Mineral Powder Material Handling Systems

Application and Industry Relevance

Rare earth mineral powder material handling systems are widely used in various industries, including electronics, automotive, and renewable energy sectors. The demand for rare earth elements in high-tech applications has increased the need for efficient and reliable material handling solutions. These systems play a vital role in ensuring the smooth flow of rare earth powders from extraction to processing and final product manufacturing.

For industries dealing with rare earth minerals, investing in a well-designed material handling system is essential for maintaining productivity, ensuring product quality, and complying with environmental standards. The systems not only enhance operational efficiency but also contribute to cost savings by reducing material loss and minimizing downtime.
Working Principle and Features of Rare Earth Mineral Powder Material Handling Systems

Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing rare earth mineral powder material handling systems tailored to the specific needs of its clients. With a focus on innovation and quality, the company has established itself as a trusted partner in the industry, delivering systems that meet the highest standards of performance and reliability.

Headquartered in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. leverages its expertise and advanced technology to develop customized solutions that address the unique challenges of handling rare earth mineral powders. The company's commitment to customer satisfaction and technological advancement has made it a preferred choice for businesses seeking reliable material handling systems.

recommend

Copyright © Shandong Headpowder Engineering Co., Ltd.    营业执照公示 网站地图

top
