With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Perlite powder conveyors are specialized equipment designed for the efficient and reliable transportation of perlite powder, a lightweight, inorganic material widely used in construction, horticulture, and industrial applications. As a key component in material handling systems, these conveyors play a crucial role in ensuring smooth and consistent operation in various industrial settings. This article will explore the working principle and key features of perlite powder conveyors, providing insights into how they function and the advantages they offer, with a focus on the solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
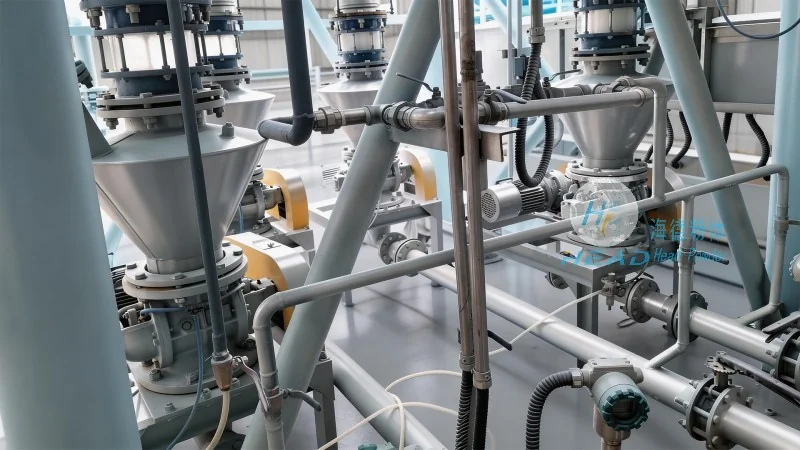
The operation of perlite powder conveyors is based on a combination of mechanical and pneumatic principles, tailored to handle the unique properties of perlite powder. The core mechanism typically involves a hopper or feeding system that stores the perlite powder, which is then fed into a conveyor tube or duct. Within the conveyor, a series of components work in tandem to move the powder through the system. A common design includes a motor-driven fan or blower that generates airflow, which propels the perlite particles along the conveyor path. The airflow is controlled to maintain a consistent velocity, preventing clogging and ensuring uniform material flow. Additionally, some systems incorporate vibration or agitation mechanisms to assist in moving the powder, especially when dealing with finer or more cohesive perlite particles. The entire process is automated, with sensors and controls monitoring the flow rate and pressure to maintain optimal performance. This integrated approach ensures that the perlite powder is transported efficiently from the source to the destination, minimizing downtime and maximizing productivity.
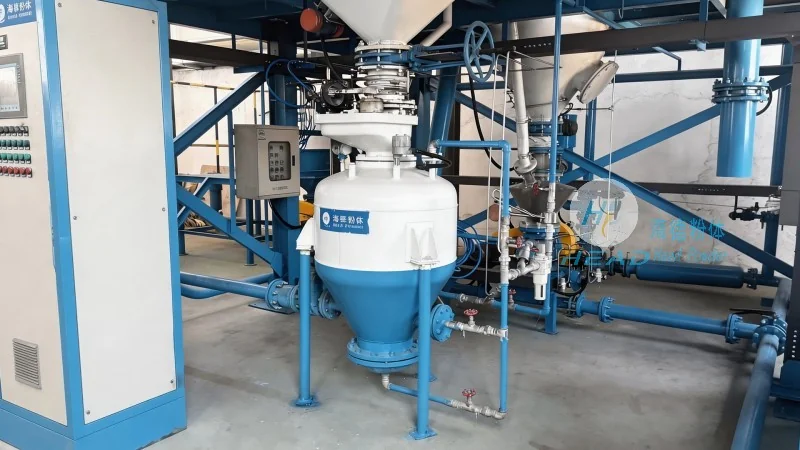
Perlite powder conveyors are engineered with several key features that enhance their performance and adaptability. One of the primary features is their ability to handle fine, lightweight powders without causing excessive wear or degradation. The materials used in the construction of the conveyor components, such as stainless steel or corrosion-resistant alloys, are selected to withstand the abrasive nature of perlite while maintaining durability. Another critical feature is the system's efficiency in maintaining a consistent flow rate, which is essential for processes that require precise material delivery. The use of variable speed drives allows operators to adjust the airflow and conveyor speed according to the specific requirements of the application, ensuring optimal performance under different load conditions. Furthermore, perlite powder conveyors are designed for easy maintenance and cleaning, with removable components that can be cleaned or replaced without extensive downtime. This feature is particularly important in industries where hygiene and material purity are critical, such as in food processing or pharmaceutical applications. The compact design of these conveyors also contributes to their versatility, as they can be integrated into existing production lines or used as standalone units in smaller operations. Overall, the combination of these features makes perlite powder conveyors a reliable and efficient solution for material handling in various industrial sectors.
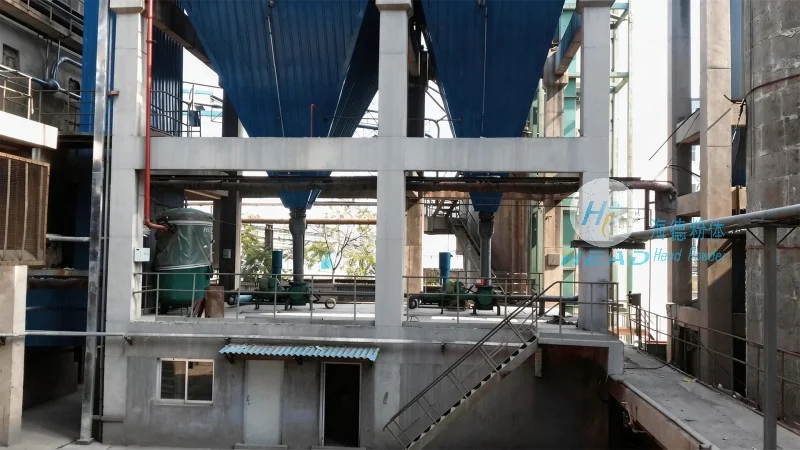
Perlite powder conveyors find applications in a wide range of industries, including construction, where perlite is used as a lightweight aggregate in concrete and plaster, horticulture, where it serves as a soil amendment and growing medium, and industrial processes that require the transport of fine powders. The benefits of using these conveyors include improved material handling efficiency, reduced labor costs, and enhanced safety in the workplace. By automating the transportation process, companies can minimize the risk of dust exposure and material spillage, which not only improves working conditions but also reduces the risk of product contamination. Additionally, the consistent flow of perlite powder ensures that production processes are not interrupted, leading to higher overall productivity. The durability and low maintenance requirements of these conveyors also contribute to long-term cost savings, as they require less frequent repairs and replacements compared to traditional material handling methods. In summary, perlite powder conveyors offer a reliable and efficient solution for transporting perlite powder, making them an essential component in modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top