

Working Principle and Features of Multi-Hopper Powder Transport Systems
Multi-hopper pneumatic conveying systems are advanced industrial equipment designed for efficient and reliable powder handling and transportation. This article provides an in-depth exploration of the working principle and key features of such systems, with a focus on the technology and applications that make them indispensable in various industries.
Introduction to Multi-Hopper Powder Transport Systems
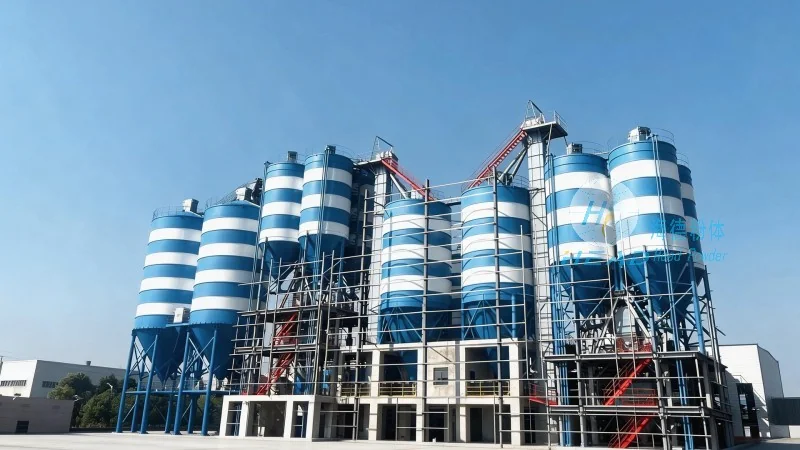
Developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in China, multi-hopper powder transport systems represent a significant advancement in bulk material handling. These systems are engineered to handle a wide range of powders, from fine to coarse particles, with high efficiency and minimal product degradation. The design incorporates multiple hoppers that allow for the sequential or simultaneous feeding of different materials, enhancing operational flexibility and throughput.
Working Principle of Multi-Hopper Powder Transport Systems
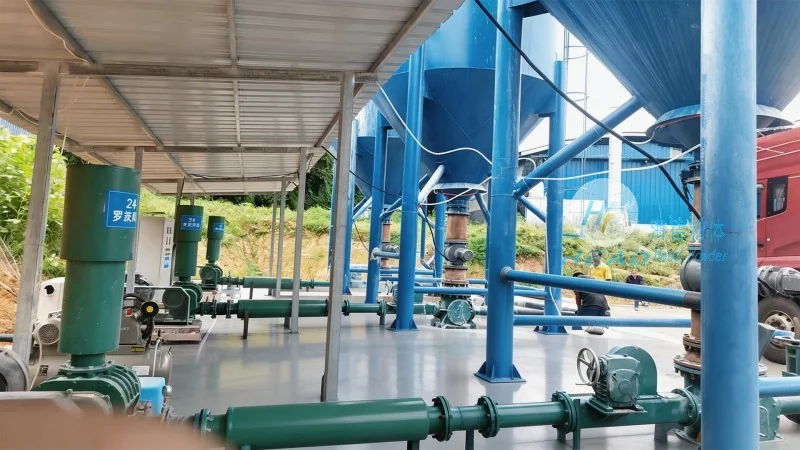
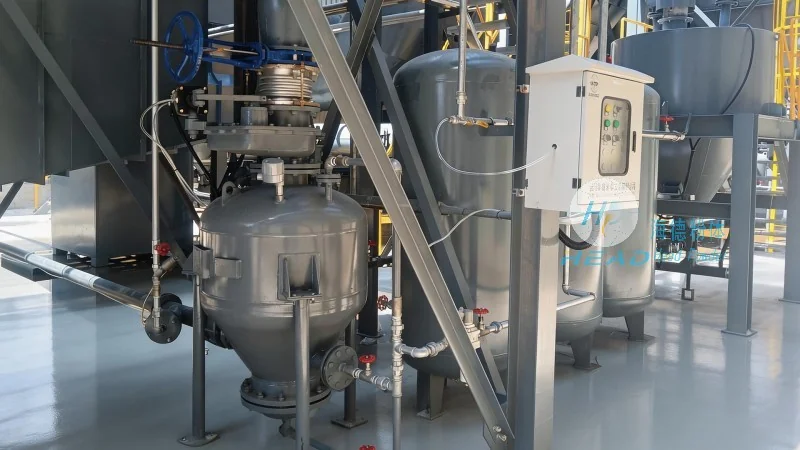
The core working principle of multi-hopper powder transport systems is based on pneumatic conveying, where air or gas is used to transport powders through a pipeline network. The system typically consists of several key components: hoppers for material storage, feeders to control the flow rate, a conveying line with appropriate ducting, and a receiver for the discharged material. The operation begins with the material being loaded into the hoppers. As the feeder opens, the powder is released into the conveying line under the pressure of the air stream. The air velocity is carefully controlled to ensure that the powder particles are entrained and transported without clogging or degradation. The system may use positive pressure or negative pressure (vacuum) depending on the application requirements, with positive pressure being more common for long-distance or high-capacity transport.
Key Features and Advantages
Multi-hopper powder transport systems offer several distinct advantages that make them superior to traditional bulk handling methods. Firstly, they provide a dust-free and enclosed environment, which is crucial for maintaining product quality and ensuring workplace safety. The enclosed design prevents dust emissions, reducing the risk of inhalation and contamination. Secondly, these systems are highly efficient in terms of energy consumption and material throughput. By using a single air stream to transport multiple materials, they achieve high capacity with minimal energy input. Thirdly, the modular design allows for easy integration with existing production lines and scalability to meet varying production demands. The ability to handle different materials in separate hoppers enables precise control over the mixing ratios and prevents cross-contamination, which is essential in industries such as pharmaceuticals, food processing, and chemical manufacturing.
Application-Specific Considerations
The versatility of multi-hopper powder transport systems makes them suitable for a wide array of applications across different industries. In the pharmaceutical industry, for example, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with strict quality control requirements. The enclosed and sterile design ensures that the materials remain free from contamination and maintain their potency. In the food industry, they are employed to handle powders like flour, sugar, and spices, where hygiene and product integrity are paramount. The ability to handle hygroscopic materials without moisture absorption is a key feature that enhances product quality. In the chemical industry, multi-hopper systems are used for transporting raw materials and intermediates, often in high-temperature or corrosive environments, where the robust construction and material compatibility of the system are critical.
Conclusion and Company Overview
Multi-hopper powder transport systems, as exemplified by the products of Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated solution for modern bulk material handling challenges. By combining advanced pneumatic conveying technology with modular design, these systems offer high efficiency, reliability, and flexibility. The working principle, which relies on controlled air flow to transport powders through an enclosed system, ensures minimal product degradation and optimal performance. The key features, including dust-free operation, energy efficiency, and material separation capabilities, make them a preferred choice in industries where product quality and safety are non-negotiable. As a leading manufacturer based in China, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide tailored solutions that meet the evolving needs of global industries, ensuring that bulk material handling remains efficient, safe, and sustainable.