With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Pharmaceutical powder conveying systems are critical components in modern pharmaceutical manufacturing, designed to efficiently and safely transport powders from one processing stage to another. These systems are engineered to meet stringent regulatory requirements and ensure product integrity throughout the manufacturing process. Understanding the working principle and key features of such systems is essential for optimizing production efficiency and maintaining compliance in the pharmaceutical industry.
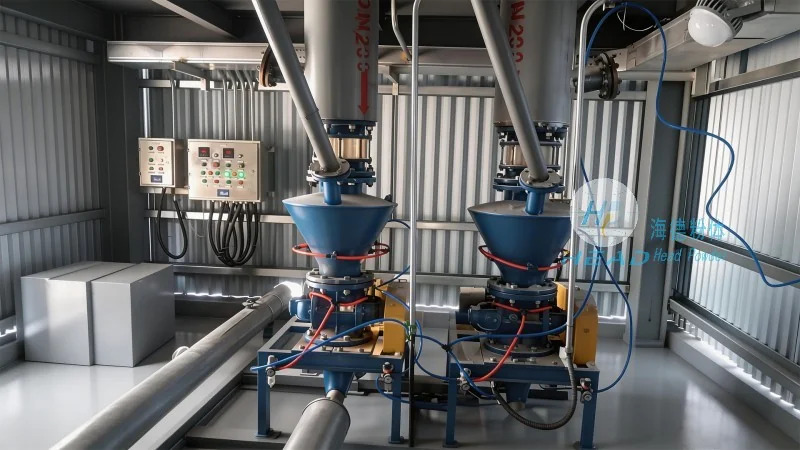
The working principle of pharmaceutical powder conveying systems typically involves a combination of mechanical and pneumatic components working in tandem to move powders. The process begins with the powder being loaded into a hopper or storage container. From there, the system uses various mechanisms such as rotary valves, screw conveyors, or air slides to transport the powder through a network of pipes or enclosed ducts. Pneumatic conveying systems, in particular, utilize compressed air to create a flow of powder particles, ensuring gentle handling and minimal product degradation. The system is equipped with control panels that allow operators to monitor and adjust the flow rate, pressure, and other parameters to maintain consistent performance. This integrated approach ensures that powders are conveyed with precision, avoiding issues like caking, agglomeration, or contamination.
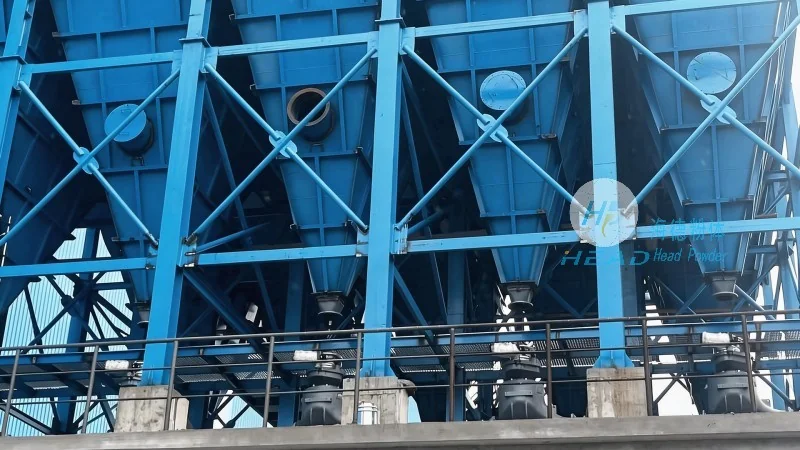
Pharmaceutical powder conveying systems are characterized by several key features that make them suitable for the demanding requirements of the pharmaceutical industry. One of the most important features is their ability to provide precise control over the flow of powders, which is crucial for maintaining consistent dosages and batch uniformity. The systems are often designed with stainless steel or other corrosion-resistant materials to ensure compliance with GMP (Good Manufacturing Practice) standards and prevent contamination. Additionally, these systems incorporate advanced filtration and cleaning mechanisms to maintain a sterile environment and prevent cross-contamination between different product batches. Another notable feature is their flexibility, allowing for easy integration with other manufacturing equipment and adaptability to different powder types and processing needs. The systems also include safety features such as pressure relief valves and emergency shut-off mechanisms to prevent accidents and protect personnel. These features collectively contribute to the reliability and efficiency of pharmaceutical powder conveying lines.
Pharmaceutical powder conveying systems are widely used in various stages of pharmaceutical manufacturing, including raw material handling, blending, packaging, and quality control. In raw material handling, these systems efficiently transport raw powders from storage to processing areas, reducing manual handling and associated risks. During blending, the systems ensure uniform mixing of different powder components, which is critical for achieving the desired product formulation. In packaging, the systems deliver powders to filling machines with high accuracy, minimizing product loss and improving production throughput. The benefits of using these systems extend beyond operational efficiency; they also contribute to cost savings by reducing material waste and downtime due to equipment failures. Furthermore, the precise control and clean design of the systems help maintain product quality and regulatory compliance, which are paramount in the pharmaceutical industry. By optimizing powder handling processes, pharmaceutical companies can enhance their overall manufacturing performance and meet the increasing demands of the market.
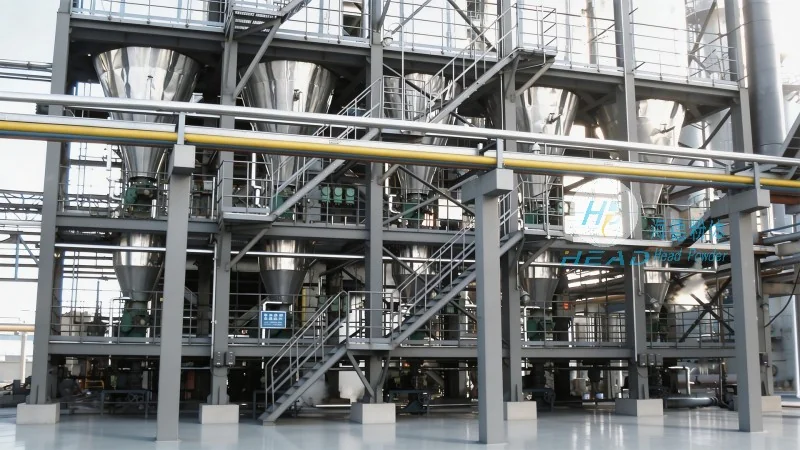
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of pharmaceutical powder conveying systems and related equipment. The company is headquartered in Shandong, China, and has established a strong reputation for providing high-quality, reliable solutions tailored to the specific needs of the pharmaceutical industry. With years of experience and a commitment to innovation, headpowder has developed advanced powder handling technologies that meet the stringent requirements of GMP and other regulatory standards. The company’s products are designed with precision engineering and rigorous quality control to ensure durability, efficiency, and safety. Headpowder’s team of experts works closely with clients to understand their unique manufacturing challenges and provide customized solutions that enhance production capabilities and reduce operational costs. By leveraging advanced materials and manufacturing techniques, headpowder delivers systems that are not only effective but also easy to maintain and operate. The company’s dedication to customer satisfaction and continuous improvement has made it a trusted partner for pharmaceutical manufacturers worldwide, helping them achieve their production goals while maintaining the highest standards of quality and compliance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top