With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Embolic powder transport equipment is a specialized device designed for the efficient and controlled transportation of powders in industrial applications. Understanding its working principle and key features is essential for users seeking reliable solutions in powder handling processes. This article provides an in-depth overview of the technology behind embolism-type powder transport equipment, highlighting its operational mechanics and distinctive characteristics.
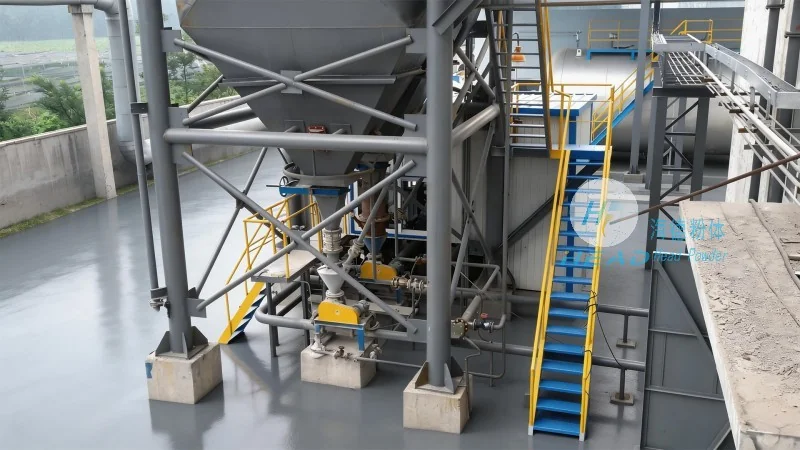
The core working principle of embolism-type powder transport equipment revolves around the creation of a controlled, high-pressure environment to move powders through a pipeline. The system typically operates by using a pump or compressor to generate pressure, which forces the powder particles to flow through the transport line. A critical component in this process is the embolism valve or nozzle, which regulates the flow rate and pressure, ensuring consistent and stable powder transport. The equipment often incorporates a hopper or storage tank at the inlet to hold the powder, and a discharge mechanism at the outlet to deliver the material to the target location. The pressure differential between the inlet and outlet, combined with the design of the embolism nozzle, enables the efficient movement of even fine or cohesive powders without clogging or degradation. This mechanism allows for precise control over the flow rate, making it suitable for applications requiring accurate dosing or uniform distribution.
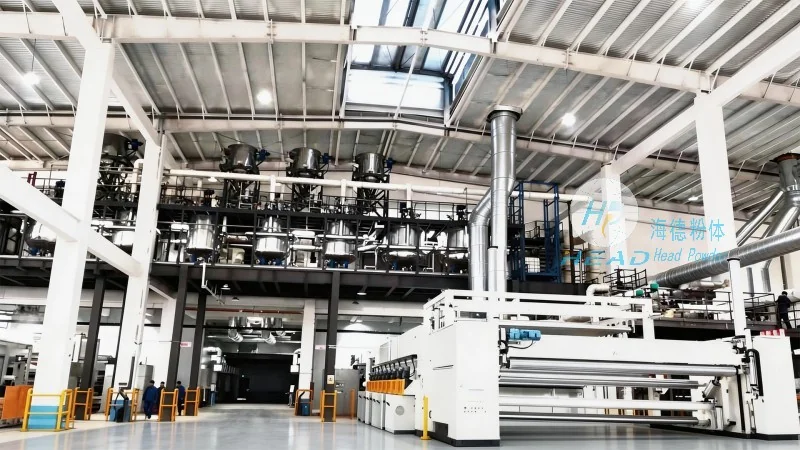
Embolism-type powder transport equipment is characterized by several notable features that enhance its performance and usability in industrial settings. One of the primary features is its ability to handle a wide range of powder types, including fine powders, granules, and even cohesive materials that are challenging for conventional transport methods. The equipment is designed to minimize particle degradation and agglomeration during transport, preserving the integrity of the material. Another key feature is the high efficiency in terms of energy consumption and operational costs. By using a pressure-driven system, it reduces the need for large volumes of air or other media, leading to lower operational expenses and reduced environmental impact. The equipment also offers excellent scalability, allowing it to be adapted for both small-scale laboratory applications and large-scale industrial production lines. Additionally, the system provides reliable and consistent performance, with minimal downtime due to its robust construction and advanced control systems. Safety features are integrated into the design, such as pressure relief valves and material containment mechanisms, to ensure safe operation in various industrial environments. The compact design of the equipment makes it suitable for installation in confined spaces, while the modular components allow for easy maintenance and replacement of parts.
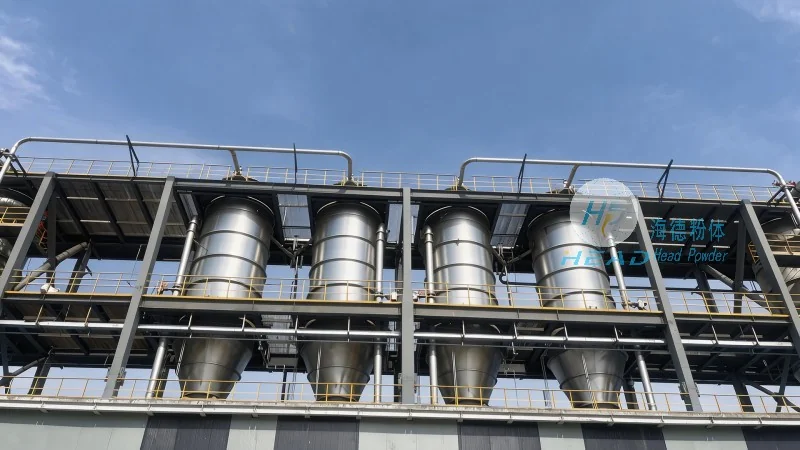
The embolism-type powder transport equipment is widely used in various industrial sectors, including pharmaceuticals, chemicals, food processing, and mining. In pharmaceutical manufacturing, it is employed for the transport of active pharmaceutical ingredients (APIs) and excipients, ensuring precise dosing and contamination-free handling. In the chemical industry, it facilitates the movement of raw materials and intermediates, supporting continuous production processes. The equipment's ability to handle cohesive powders makes it particularly valuable in the food industry, where it is used for transporting ingredients like flour, sugar, and spices. In mining operations, it aids in the transport of ore and minerals from processing plants to storage or further processing facilities. The advantages of this technology extend beyond efficiency and reliability. The controlled pressure system reduces the risk of dust explosions and material loss, enhancing workplace safety. Furthermore, the equipment's low maintenance requirements and long service life contribute to overall cost savings for industrial operations. The adaptability of the system to different powder types and process conditions makes it a versatile solution for diverse industrial needs.
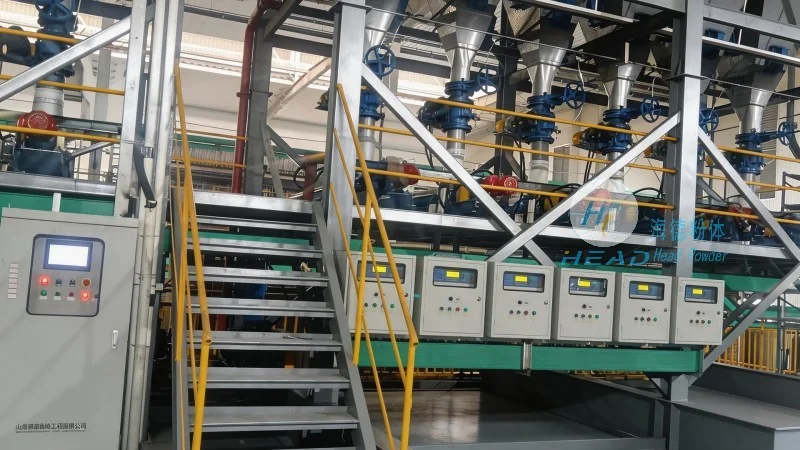
In summary, embolism-type powder transport equipment offers a sophisticated solution for the efficient and reliable handling of powders in industrial applications. Its working principle, based on controlled pressure and embolism valve technology, enables the smooth transport of various powder types with minimal degradation. The key features, including wide material compatibility, high efficiency, and robust design, make it an ideal choice for industries requiring precise and consistent powder handling. As a product of Shandong HeadPowder Engineering Co., Ltd., this equipment exemplifies advanced engineering and industrial innovation, providing users with a reliable and cost-effective solution for their powder transport needs. With its commitment to quality and performance, Shandong HeadPowder Engineering Co., Ltd. continues to deliver cutting-edge solutions that meet the evolving demands of modern industrial processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top