With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
In modern industrial facilities, the management of particulate matter is a critical aspect of operations. Dust not only poses significant health risks to personnel but can also create hazardous environments if not handled correctly. Consequently, industries ranging from pharmaceuticals to heavy manufacturing require robust systems to manage waste and byproducts. The primary focus of this discussion is the various methods available for handling these materials, specifically comparing traditional mechanical approaches with advanced pneumatic solutions. Understanding these dust conveying methods is essential for selecting the right infrastructure that ensures safety, efficiency, and regulatory compliance.
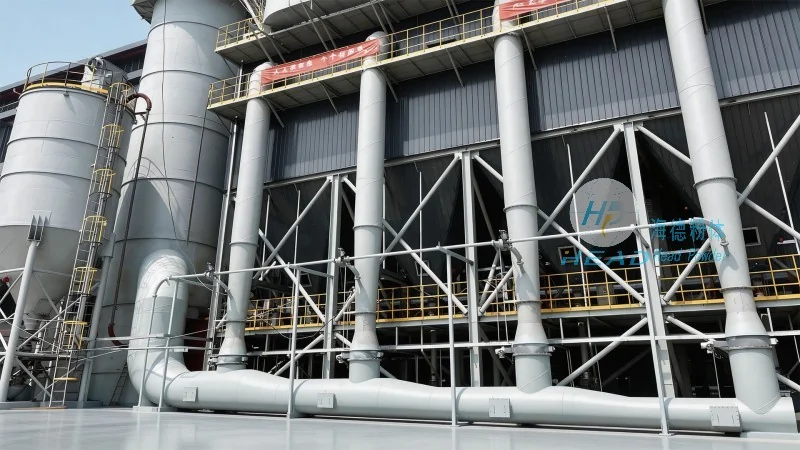
Traditional dust removal often relies on mechanical equipment such as rotary valves, screw conveyors, and belt systems. While these are effective for bulk materials, they are often prone to leakage and can introduce contaminants into the surrounding air. This necessitates a shift toward more sophisticated systems that prioritize containment and cleanliness. As industrial processes become more automated, the demand for precise and reliable material handling has grown. This evolution has led to the widespread adoption of systems that utilize air pressure or vacuum to transport materials, marking a significant advancement in the field of dust conveying methods.
At the forefront of modern material handling is the technology known as dust pneumatic conveying. This method utilizes air pressure or vacuum to transport dry bulk materials through a closed pipeline system. Unlike mechanical conveyors that rely on physical contact, pneumatic systems suspend the particles in the air stream, allowing for a clean transfer process. This technology is particularly vital for handling fine, light, or abrasive dust, which can be difficult to manage with traditional equipment.
The core mechanism of a pneumatic system involves a source of compressed air or vacuum that creates a flow within a pipeline. The material is introduced into the pipeline, where it is mixed with the air stream and transported to the desired destination. This process ensures that the material remains contained within the system, minimizing dust emissions and preventing cross-contamination. Because the system is fully enclosed, it meets strict hygiene standards, making it the preferred choice for industries where cleanliness is paramount. The versatility of dust pneumatic conveying allows it to handle a wide range of materials, from fine powders to granules, with high reliability and minimal maintenance requirements.
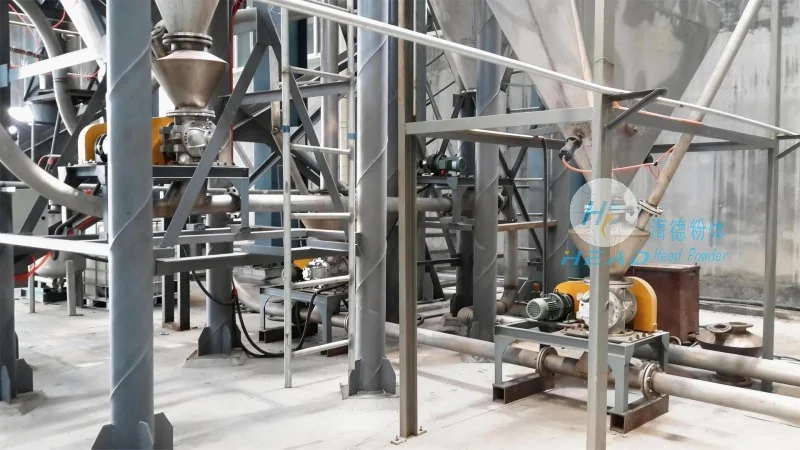
Shandong Headpowder Engineering Co., Ltd. has established itself as a premier provider of engineering solutions in the field of powder and dust handling. Headquartered in Shandong, China, the company combines advanced engineering principles with practical manufacturing expertise to deliver superior systems. Our core competency lies in the design and installation of comprehensive dust conveying solutions that cater to the specific needs of our clients. We specialize in bridging the gap between complex industrial requirements and reliable, efficient machinery.
As a dedicated engineering firm, we understand that every facility has unique challenges. Therefore, we do not offer generic solutions; instead, we focus on tailored designs that optimize the flow of materials. Our team of engineers possesses deep knowledge of fluid dynamics and material handling, ensuring that every system we design is robust and efficient. By leveraging our location in Shandong—a hub for industrial manufacturing—we are able to utilize high-quality components and innovative technologies to produce systems that stand the test of time. Our commitment to excellence ensures that clients receive not just a machine, but a complete engineering solution.
Our primary offerings center on high-performance dust conveying systems and general material transport solutions. We engineer systems that are capable of handling large volumes of dust and powder without compromising on safety or speed. The dust conveying systems we manufacture are designed to integrate seamlessly into existing production lines, enhancing overall efficiency. Whether the requirement is for a simple vacuum collection or a complex multi-point distribution network, our systems provide the flexibility needed to modernize operations.
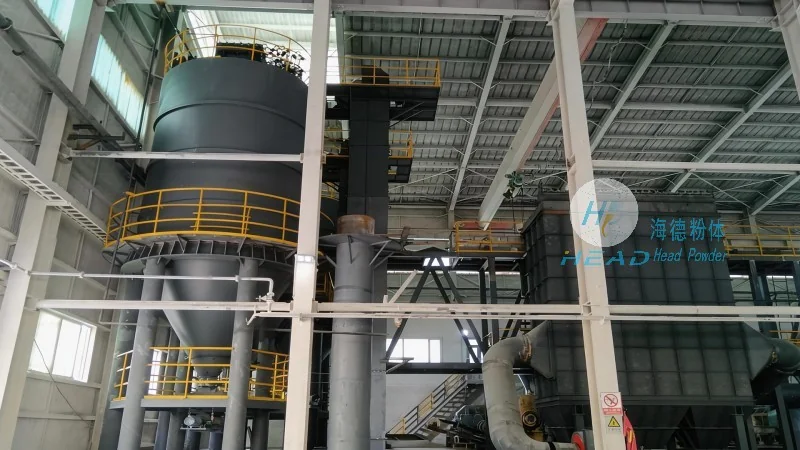
The material transport capabilities of our systems are unmatched in terms of reliability. By utilizing advanced control valves and sensors, we ensure precise metering and consistent flow rates. This precision reduces waste and increases the yield of valuable materials. Our dust conveying solutions are engineered to handle the most challenging materials, including those that are cohesive, hygroscopic, or highly abrasive. By focusing on the integrity of the dust conveying process, we help our clients maintain a clean and productive work environment while maximizing the recovery and reuse of valuable byproducts.
Investing in a system from Headpowder offers numerous technical and operational advantages. One of the standout features of our dust pneumatic conveying systems is their ability to operate in diverse environments. The fully enclosed nature of the system eliminates the risk of dust explosions, a critical safety feature for handling combustible powders. Furthermore, our systems are designed for energy efficiency, utilizing optimized air-to-material ratios to reduce power consumption while maintaining high throughput.
Another significant benefit is the reduction in maintenance costs. Traditional mechanical conveyors often suffer from wear and tear due to friction, whereas pneumatic systems have fewer moving parts in contact with the material. This results in a longer service life for the equipment and less frequent downtime for repairs. Our engineering team focuses on durability, using high-grade materials that resist corrosion and erosion. This ensures that the dust conveying systems remain operational and efficient even under continuous heavy loads. By choosing Headpowder, clients are investing in a sustainable and cost-effective approach to material handling.
The versatility of our dust conveying methods makes them suitable for a wide array of industries. In the pharmaceutical sector, our systems ensure that active ingredients are transported without contamination, adhering to strict Good Manufacturing Practices (GMP). In the chemical industry, they handle hazardous powders safely, protecting both workers and the environment. Additionally, our material transport solutions are utilized in food processing for transporting flour, sugar, and other dry ingredients, ensuring product purity.

Industrial facilities that generate significant amounts of waste dust also benefit greatly from our specialized equipment. Our systems are capable of connecting multiple collection points to a central processing unit, streamlining the waste management process. This centralized approach simplifies operations and improves overall facility management. Regardless of the specific application, our goal remains the same: to provide a reliable, clean, and efficient method of moving materials from point A to point B.
To discuss your specific material handling requirements or to request a detailed consultation, please reach out to our team. We are dedicated to providing expert guidance to help you select the best dust conveying methods for your facility. Our experienced staff is ready to assist you in designing a system that meets your operational goals.
For direct inquiries regarding project planning and engineering support, please contact Mr. Zhang, our dedicated manager. He can be reached via WeChat at 15662777102. We look forward to the opportunity to collaborate with you and provide a solution that enhances your production capabilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top