

What is a Tote Bag Packing Powder Pneumatic Conveying Machine? What are its Design Principles?
For industrial operations dealing with bulk powders, the tote bag packing pneumatic conveying machine is a critical piece of equipment designed to efficiently handle, transport, and package materials. This article explores the functionality and design principles behind such machinery, providing insights into how it operates and its significance in modern material handling processes.
Understanding the Core Function of the Equipment
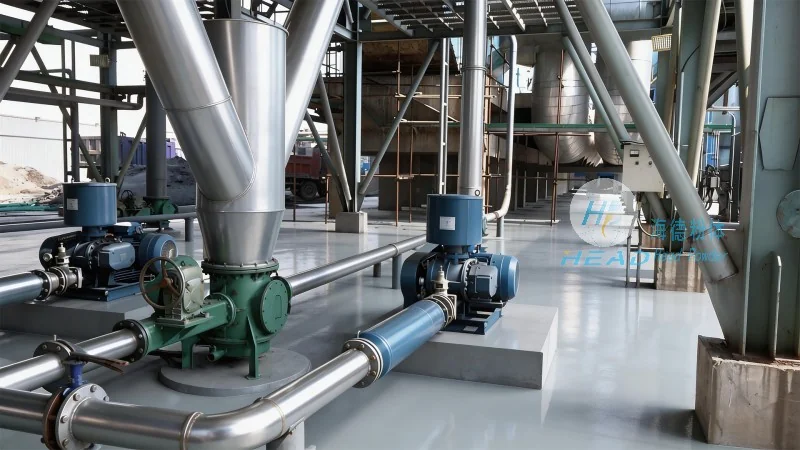
The primary purpose of a tote bag packing powder pneumatic conveying machine is to facilitate the movement of bulk powders from a storage or processing area to a packaging unit, all within a sealed system to maintain material integrity and prevent contamination. These machines are particularly useful for handling materials that are prone to dust, such as chemicals, food products, or pharmaceuticals, ensuring a clean and controlled environment throughout the conveying process.
Key Design Principles and Technical Aspects
The design of a tote bag packing powder pneumatic conveying machine is built on several fundamental principles to ensure efficiency and reliability. One of the core components is the airlock system, which acts as a valve to control the flow of material and air, preventing backflow and maintaining consistent pressure. The conveying system typically uses positive or negative pressure to move the powder, with positive pressure being more common for short-distance transport and negative pressure for longer distances or when dealing with fine powders that may be susceptible to clogging.
Components and Operational Mechanism
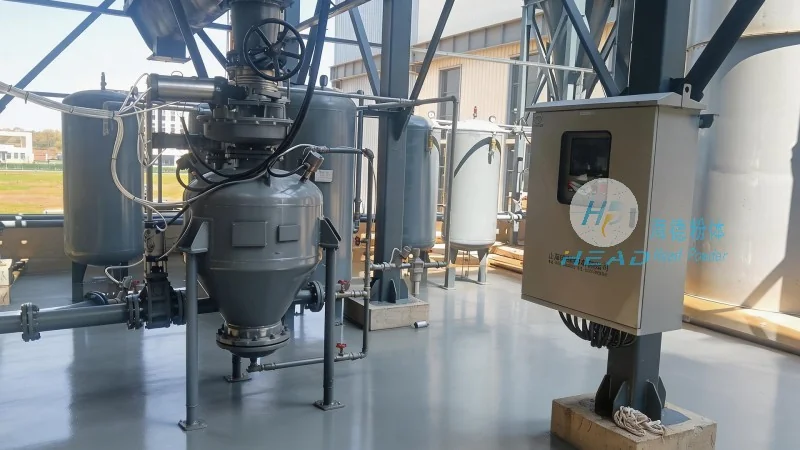
At the heart of the machine are several key components that work in tandem to achieve effective material handling. The hopper or inlet where the powder is loaded is designed to minimize material buildup and ensure a smooth flow. The conveying line, often equipped with flexible hoses or rigid pipes, transports the powder to the packaging station. The air compressor or vacuum system provides the necessary pressure or suction to move the material. The outlet or discharge point is integrated with the tote bag, which is sealed and filled as the powder is conveyed. This integrated system ensures that the entire process—from loading to packaging—is automated and streamlined.
Advantages of Using Tote Bag Packing Pneumatic Conveying Machines
Implementing a tote bag packing powder pneumatic conveying machine offers several advantages for industrial applications. Firstly, it enhances safety by containing dust and preventing exposure to airborne particles, which is crucial for maintaining a healthy work environment and complying with occupational health regulations. Secondly, it improves efficiency by automating the material handling process, reducing labor costs and minimizing the risk of human error. Thirdly, it ensures consistent product quality by maintaining a controlled environment and preventing contamination or degradation of the powder during transport. Additionally, the system is flexible and can be adapted to handle various types of powders, making it a versatile solution for different industries.
Applications in Different Industries
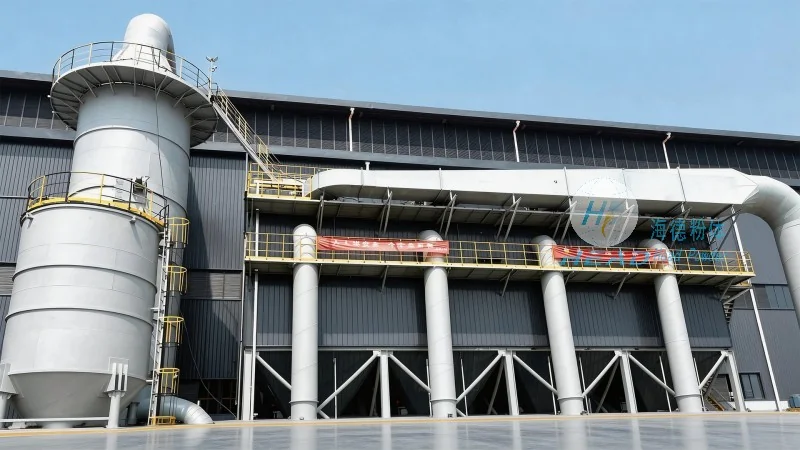
The versatility of tote bag packing powder pneumatic conveying machines makes them applicable across a wide range of industries. In the chemical industry, they are used to transport and package powders such as fertilizers, pigments, and specialty chemicals. In the food and beverage sector, they handle ingredients like flour, sugar, and spices, ensuring that the products remain fresh and free from contamination. The pharmaceutical industry also relies on these machines for handling active pharmaceutical ingredients (APIs) and other sensitive powders, where maintaining sterility and purity is paramount. Furthermore, in the mining and mineral processing industries, they are used to transport raw materials and finished products, improving the overall efficiency of the production line.
Customization and Scalability
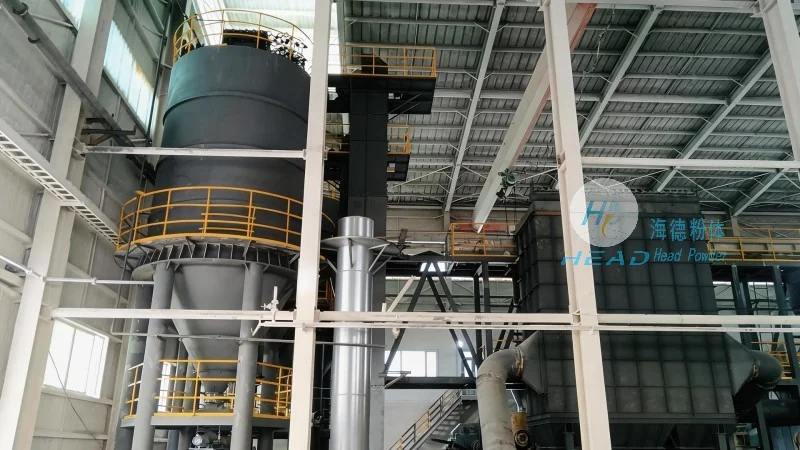
Manufacturers of tote bag packing powder pneumatic conveying machines, such as Shandong HeadPowder Engineering Co., Ltd., offer customization options to meet the specific needs of different clients. These machines can be scaled to handle varying capacities, from small batches to large-scale production. The design can be adjusted to accommodate different powder types, particle sizes, and conveying distances. Additionally, the system can be integrated with other equipment, such as weighing scales or labeling machines, to create a fully automated packaging line. This flexibility ensures that the equipment can be tailored to fit the unique requirements of each industrial application.
Maintenance and Longevity
Proper maintenance is essential to ensure the longevity and optimal performance of a tote bag packing powder pneumatic conveying machine. Regular cleaning of the hopper, conveying lines, and airlock components is necessary to prevent material buildup and clogging. The air compressor or vacuum system should be checked regularly for proper operation and maintenance to avoid breakdowns. Additionally, the seals and gaskets should be inspected and replaced as needed to maintain airtightness and prevent leaks. By following a regular maintenance schedule, users can extend the lifespan of the equipment and minimize downtime, ensuring consistent and reliable operation.