With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
When discussing industrial material handling, the sand powder conveying system equipment plays a crucial role in efficiently transporting bulk materials like sand, powders, and granules. This equipment is designed to handle various types of dry materials, ensuring smooth and reliable movement from one location to another within a production facility or construction site. Understanding the functionality and design principles of such systems is essential for optimizing operational efficiency and maintaining product quality.
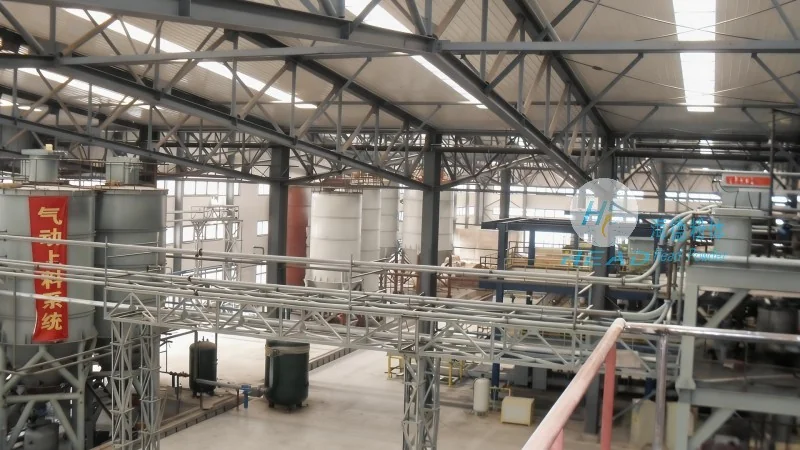
A sand powder conveying system is a specialized piece of industrial equipment engineered to transport dry, free-flowing materials. These systems are commonly used in industries like construction, mining, chemical processing, and manufacturing where large volumes of sand or other powders need to be moved. The primary goal of these systems is to provide a cost-effective, energy-efficient, and safe method of material transport, reducing manual labor and minimizing the risk of material loss or contamination.
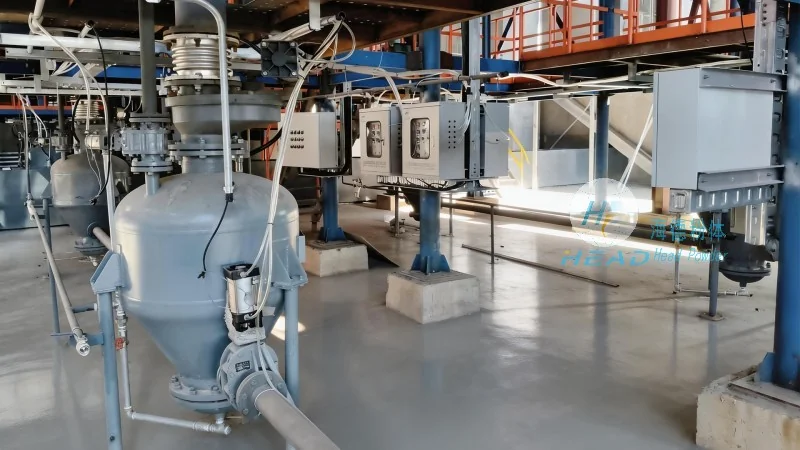
The sand powder conveying system typically consists of several key components that work in tandem to achieve effective material transport. These components include a hopper or feed hopper for material intake, a conveyor mechanism (such as a screw conveyor, pneumatic conveyor, or belt conveyor), a control system for regulating the flow rate, and a discharge outlet for delivering the material to its destination. Each component is carefully designed to handle the specific characteristics of the material being conveyed, such as particle size, density, and moisture content.
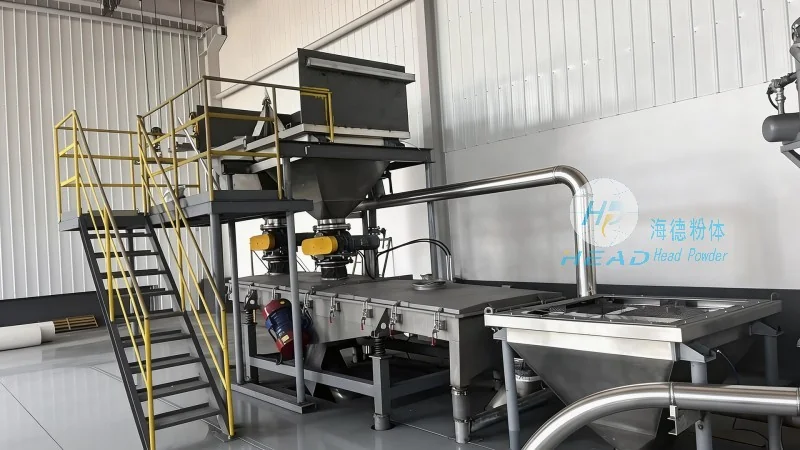
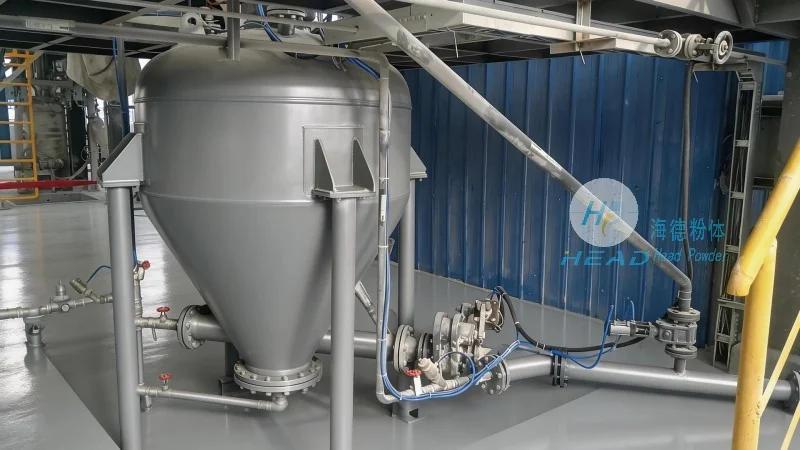
The design of a sand powder conveying system is based on several fundamental principles to ensure optimal performance. One of the key principles is the principle of gravity and mechanical force, where the system uses a combination of gravity and mechanical power to move the material. Another important principle is the principle of air flow in pneumatic conveyors, which involves using compressed air to create a flow of material through a pipeline. The design also considers factors like material flow rate, system pressure, and energy consumption to achieve the best balance between efficiency and cost.
Sand powder conveying systems are widely used in various applications across different industries. In the construction industry, they are used to transport sand for concrete mixing and other building projects. In the mining industry, they help in transporting ore and other minerals from processing plants to storage areas. In the chemical industry, these systems are used to handle powders like cement, flour, and other chemicals, ensuring safe and efficient transport. The versatility of these systems makes them indispensable in modern industrial operations.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial material handling equipment. The company specializes in designing and manufacturing sand powder conveying systems tailored to meet the specific needs of various industries. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner for businesses seeking reliable and efficient material transport solutions. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top