With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Long-distance powder conveying systems are specialized industrial equipment designed to transport bulk powders over significant distances with efficiency and precision. These systems are essential in various industries, including pharmaceuticals, food processing, and chemical manufacturing, where the reliable and safe movement of powders is critical to operational success.
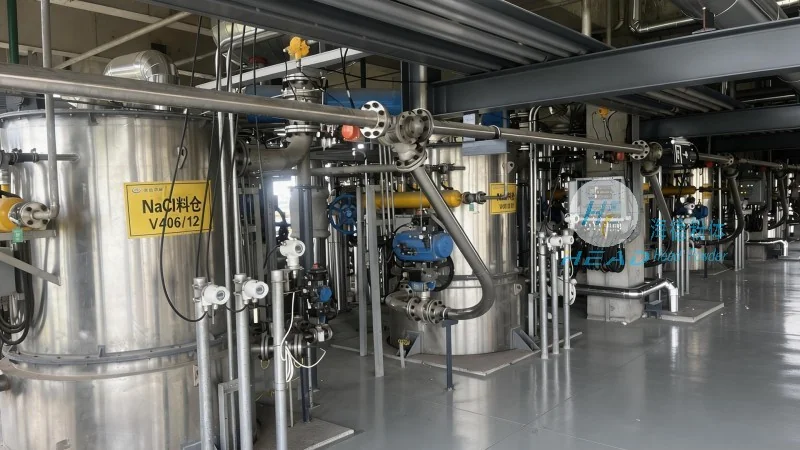
At the heart of a long-distance powder conveying system are several key components that work in tandem to ensure effective material transport. The primary components typically include a feeding mechanism, a conveying device (such as a screw or pneumatic system), a control unit, and a discharge system. The feeding mechanism, often a hopper or feeder, ensures a consistent flow of powder into the system. The conveying device, which may be a screw conveyor, pneumatic pipeline, or a combination of both, is responsible for moving the powder through the system. The control unit monitors and regulates the operation, ensuring optimal performance and preventing issues like blockages or overloading. Finally, the discharge system delivers the powder to its destination, such as a storage silo or processing unit.
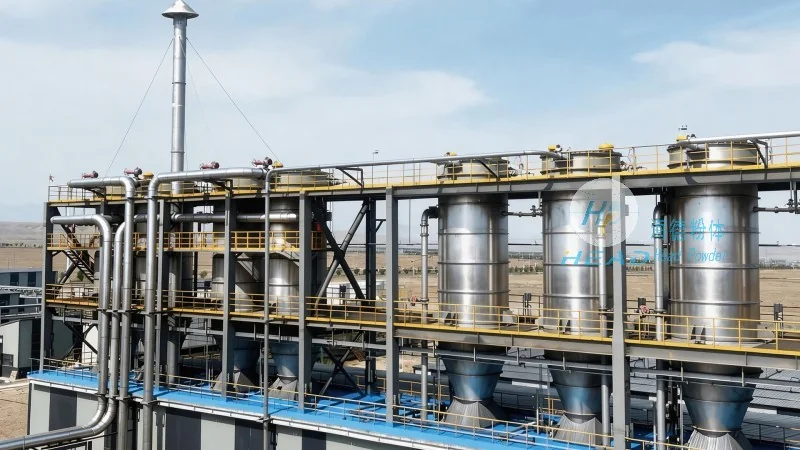
The design of long-distance powder conveying systems is guided by several fundamental principles aimed at maximizing efficiency, minimizing downtime, and ensuring safety. One of the most critical principles is the selection of the appropriate conveying method based on the characteristics of the powder being transported. For example, cohesive or fine powders may require pneumatic conveying systems, while bulkier or heavier materials might be better suited for mechanical screw conveyors. The system's design also considers the distance and elevation changes, as these factors directly impact the power requirements and overall system complexity. Additionally, material compatibility is a key consideration; the components must be resistant to the specific powders being handled to prevent contamination or degradation. The system's layout is carefully planned to minimize the number of bends and changes in direction, as these can cause powder buildup and reduce efficiency. Proper sealing and dust control measures are also integrated into the design to maintain a clean and safe working environment.
Long-distance powder conveying systems find applications across a wide range of industries, each benefiting from the systems' ability to handle bulk materials efficiently. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the final product meets strict quality standards. The food processing industry relies on these systems to move ingredients like flour, sugar, and spices from storage to production lines, maintaining hygiene and preventing contamination. In chemical manufacturing, long-distance powder conveying systems are essential for transporting raw materials and finished products, supporting continuous production processes. The benefits of these systems extend beyond efficiency; they also contribute to cost savings by reducing labor costs associated with manual handling and minimizing material loss. Furthermore, the systems enhance safety by eliminating the need for manual handling of powders, which can be hazardous due to dust inhalation or physical contact. The ability to operate continuously and with minimal maintenance also adds to the overall value of these systems for industrial operations.
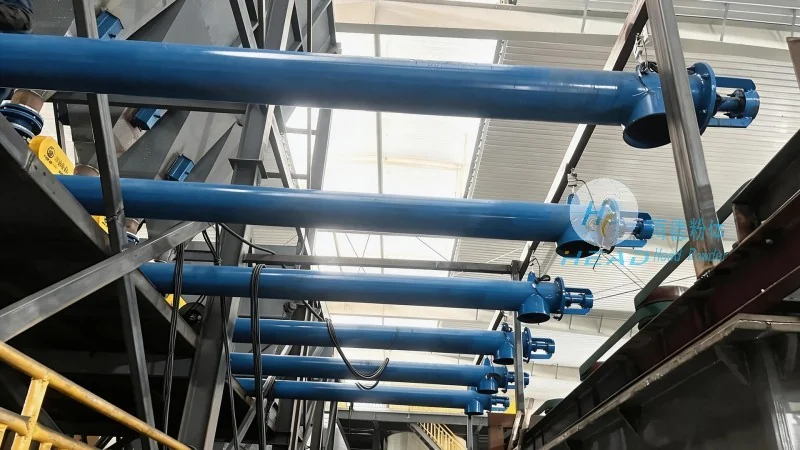
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent manufacturer and supplier of long-distance powder conveying systems. With a focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the industry. The company's products are designed to meet the specific needs of various applications, offering customized solutions that enhance operational efficiency and reliability. HeadPowder's expertise lies in the integration of advanced technology with robust engineering, resulting in systems that are durable, efficient, and easy to maintain. The company's commitment to quality is evident in its adherence to international standards and rigorous testing procedures. HeadPowder's facilities are located in Shandong, China, where the company leverages local resources and expertise to deliver high-quality products to clients worldwide. By combining technical knowledge with practical experience, HeadPowder continues to provide reliable and effective long-distance powder conveying solutions that meet the evolving needs of the industrial sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top