With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the operation of fertilizer granule pneumatic conveying equipment is crucial for optimizing material handling in agricultural and industrial settings. This equipment utilizes pneumatic technology to transport granular fertilizers efficiently and safely. The core principle involves creating a flow of air or gas within a pipeline system, which lifts and moves the fertilizer particles through the system. By leveraging pressure differentials and air velocity, the equipment can handle various types of granular materials, ensuring consistent and reliable transport from storage to processing or application points.
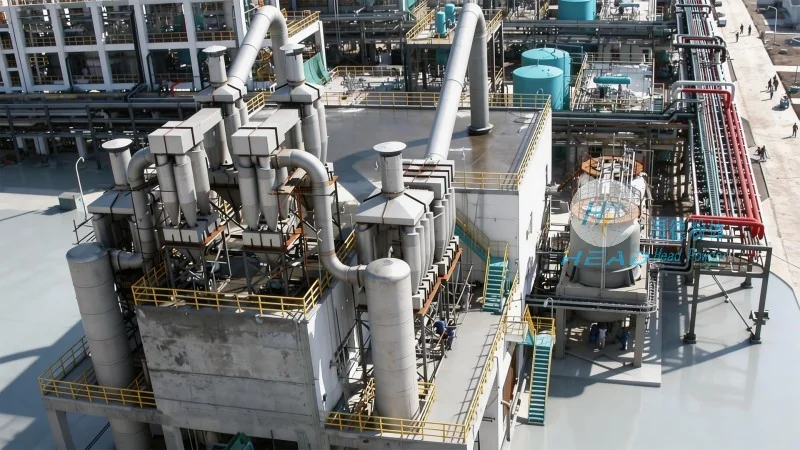
The pneumatic conveying system for fertilizer granules typically consists of several key components, each playing a vital role in the overall operation. The primary components include a blower or compressor to generate the necessary air pressure, a hopper or feeder to introduce the fertilizer granules into the system, a pipeline network to transport the material, and a separator or cyclone to separate the fertilizer from the air at the receiving end. The process begins when the fertilizer granules are fed into the hopper, where they are drawn into the pipeline by the moving air stream. As the air flows through the pipeline, it carries the granules along, maintaining a stable suspension that prevents clogging and ensures smooth transport. At the destination, the separator uses centrifugal force to separate the fertilizer from the air, allowing the fertilizer to be discharged while the air is either recirculated or vented to the atmosphere.
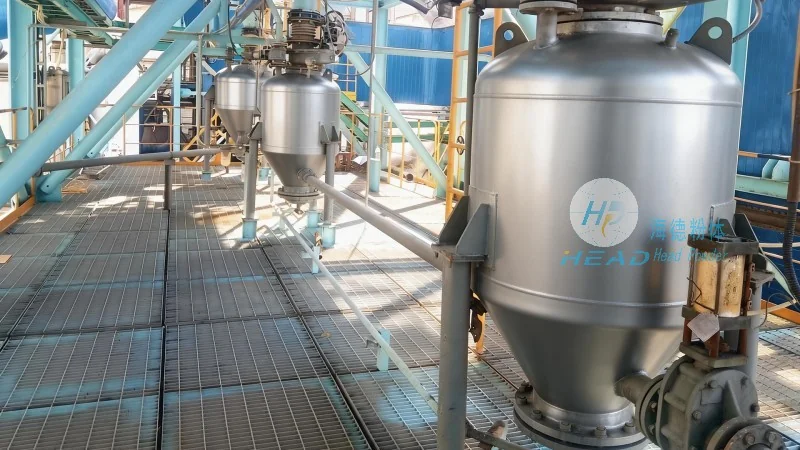
Compared to traditional mechanical conveying methods, pneumatic conveying offers several advantages for fertilizer granule transport. One of the most significant benefits is the ability to handle materials that are difficult to move with mechanical systems, such as fine or cohesive granules. The air flow provides a gentle yet effective method of transport, reducing the risk of material degradation or breakage. Additionally, pneumatic systems can cover longer distances and operate in multiple stages, making them suitable for large-scale agricultural operations. The enclosed pipeline system also minimizes dust emissions and improves safety by containing the material within the system, reducing exposure to workers and the environment. Furthermore, these systems can be easily integrated with other processing equipment, such as mixing or packaging units, enhancing overall operational efficiency.
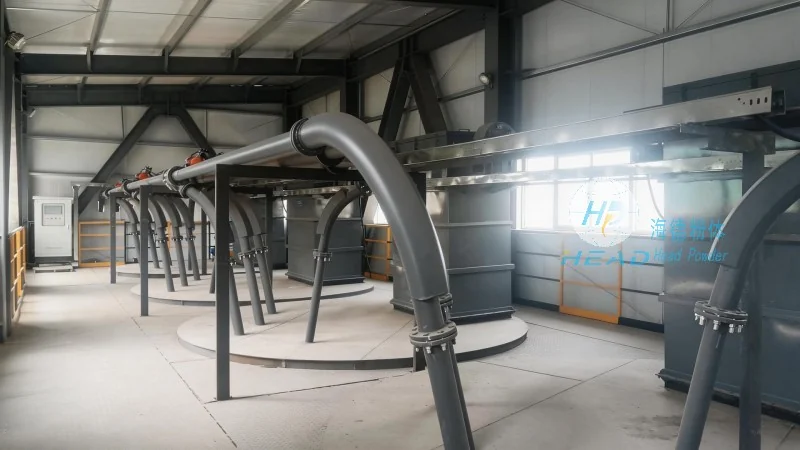
HeadPowder, a leading manufacturer of specialized material handling equipment, is dedicated to providing high-quality solutions for fertilizer granule pneumatic conveying. With years of experience in the industry, the company has developed advanced systems that meet the demands of modern agricultural and industrial applications. HeadPowder's equipment is designed with durability, efficiency, and safety in mind, ensuring reliable performance in demanding environments. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking effective fertilizer handling solutions. HeadPowder's facilities are located in Shandong, China, where the company leverages local expertise and resources to deliver superior products and services to clients worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top