With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder Engineering Co., Ltd., a leading enterprise based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for the white sugar industry. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for sugar processing facilities seeking efficient and reliable material handling solutions.
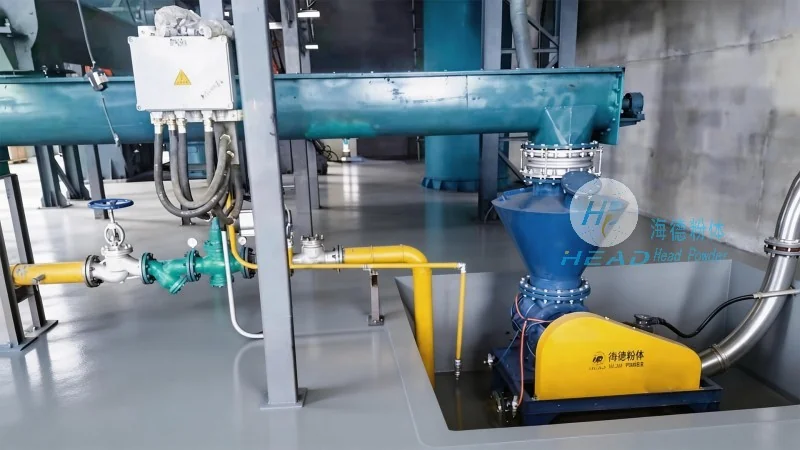
White sugar pneumatic conveying systems are crucial for modern sugar production, offering a flexible and efficient method to transport granular sugar from storage silos to processing lines, packaging areas, or other operational zones. The core of these systems lies in the use of air to move the material, eliminating the need for mechanical components like conveyor belts or buckets, which can be prone to wear and maintenance issues.
There are primarily two main types of pneumatic conveying systems used in the white sugar industry: vacuum (or suction) conveying and positive pressure (or pressure) conveying. Each type has distinct characteristics that make it suitable for different operational requirements and system configurations.
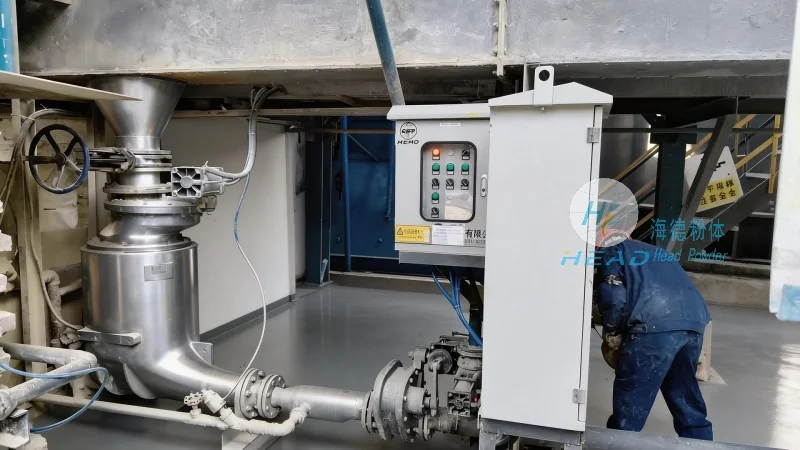
Vacuum conveying systems operate by creating a negative pressure in the conveying line, which draws the white sugar from the source (such as a storage silo or hopper) into the system. This method is particularly effective for conveying materials over short to medium distances and is often used when the material needs to be transferred from a lower elevation to a higher one, or when the system requires a relatively low air volume. The main advantages of vacuum conveying include its ability to handle a wide range of particle sizes and moisture contents, and its gentle handling of the sugar, which minimizes product degradation and dust generation. However, it may have limitations in terms of conveying distance and the maximum particle size it can handle efficiently.
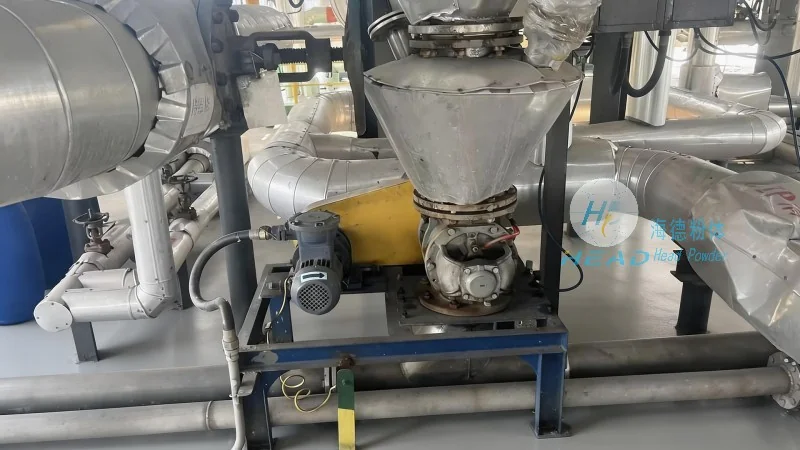
Positive pressure conveying systems, on the other hand, work by blowing air or a mixture of air and other gases under pressure into the conveying line, pushing the white sugar from the source to the destination. This type of system is generally more suitable for longer conveying distances and can handle larger particles or more abrasive materials. Positive pressure systems are often preferred when the material needs to be transported over long distances or when the system requires higher air velocities to maintain flow. The key benefits include higher conveying capacities, the ability to handle more challenging materials, and greater flexibility in system layout. However, they may require more energy input and can generate more dust if not properly designed and maintained.
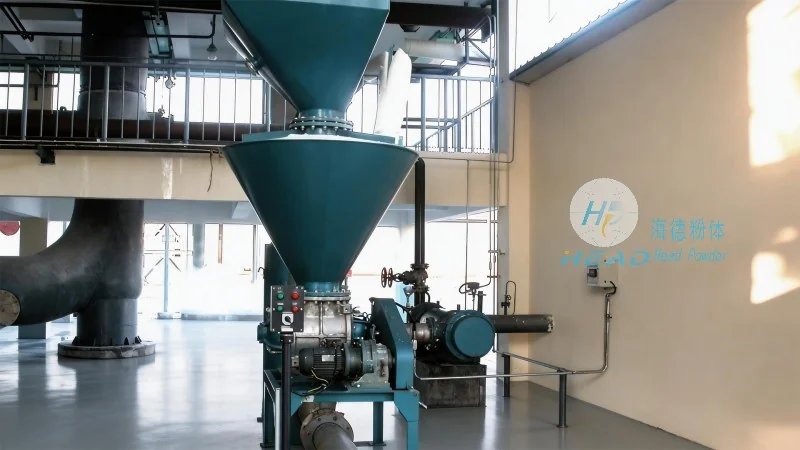
Beyond the basic types, several key characteristics define the performance and suitability of white sugar pneumatic conveying systems. These include the system's capacity, which refers to the volume of material that can be conveyed per unit time; the conveying distance, which determines the maximum length the material can be transported; and the air velocity, which affects the flow rate and the system's efficiency. Additionally, the system's ability to handle varying particle sizes and moisture levels is critical, as white sugar can have different granule sizes and moisture contents depending on the production process. Advanced systems may also incorporate features such as air filtration and dust collection to ensure environmental compliance and product purity.
The application ranges of white sugar pneumatic conveying systems are broad and cover various stages of the sugar production and processing cycle. In the storage and handling phase, these systems are used to transfer white sugar from storage silos to intermediate hoppers or processing lines. They are also employed in the packaging stage, where the sugar is conveyed from processing equipment to packaging machines, ensuring a continuous and efficient flow of product. Furthermore, pneumatic conveying systems can be integrated into quality control processes, such as sampling and testing, where the material needs to be transported to analytical equipment. The versatility of these systems allows them to be adapted to different production scales, from small-scale operations to large industrial facilities, making them a valuable asset in the modern sugar industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top